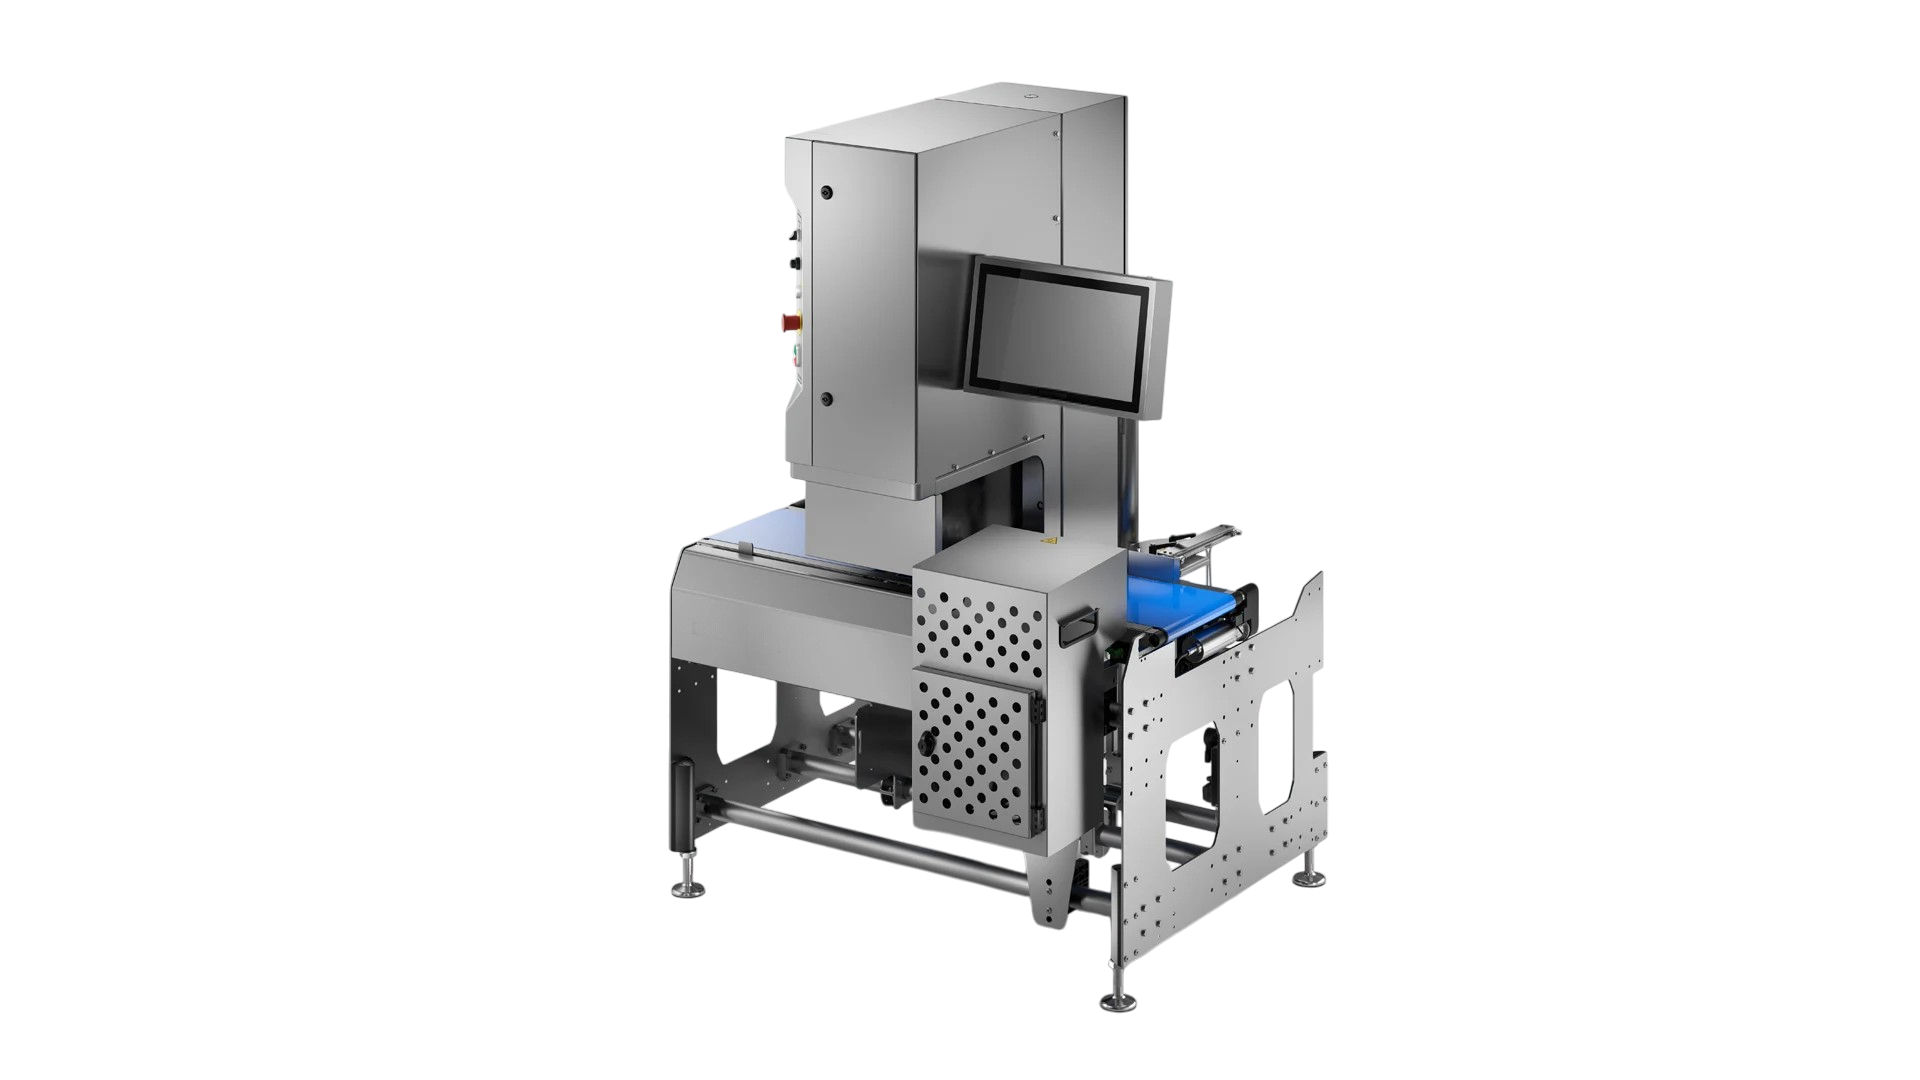
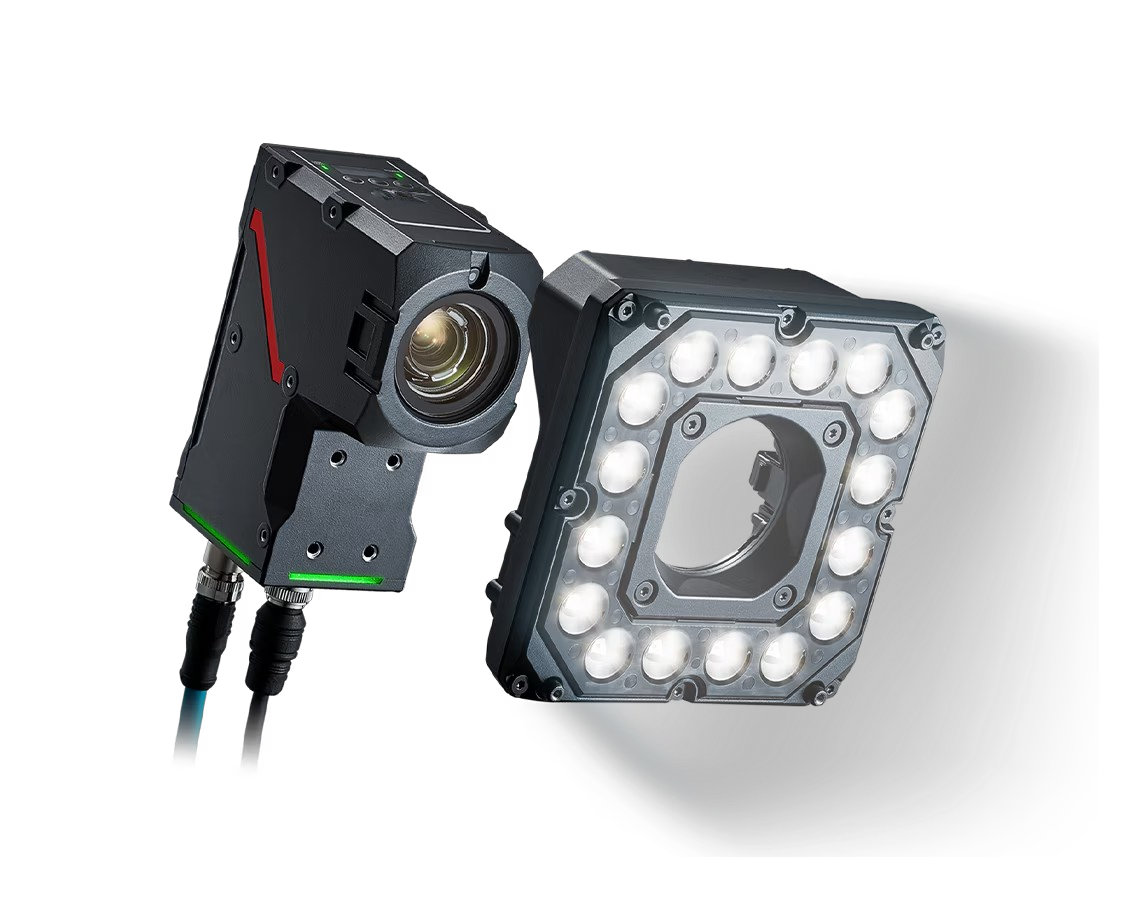
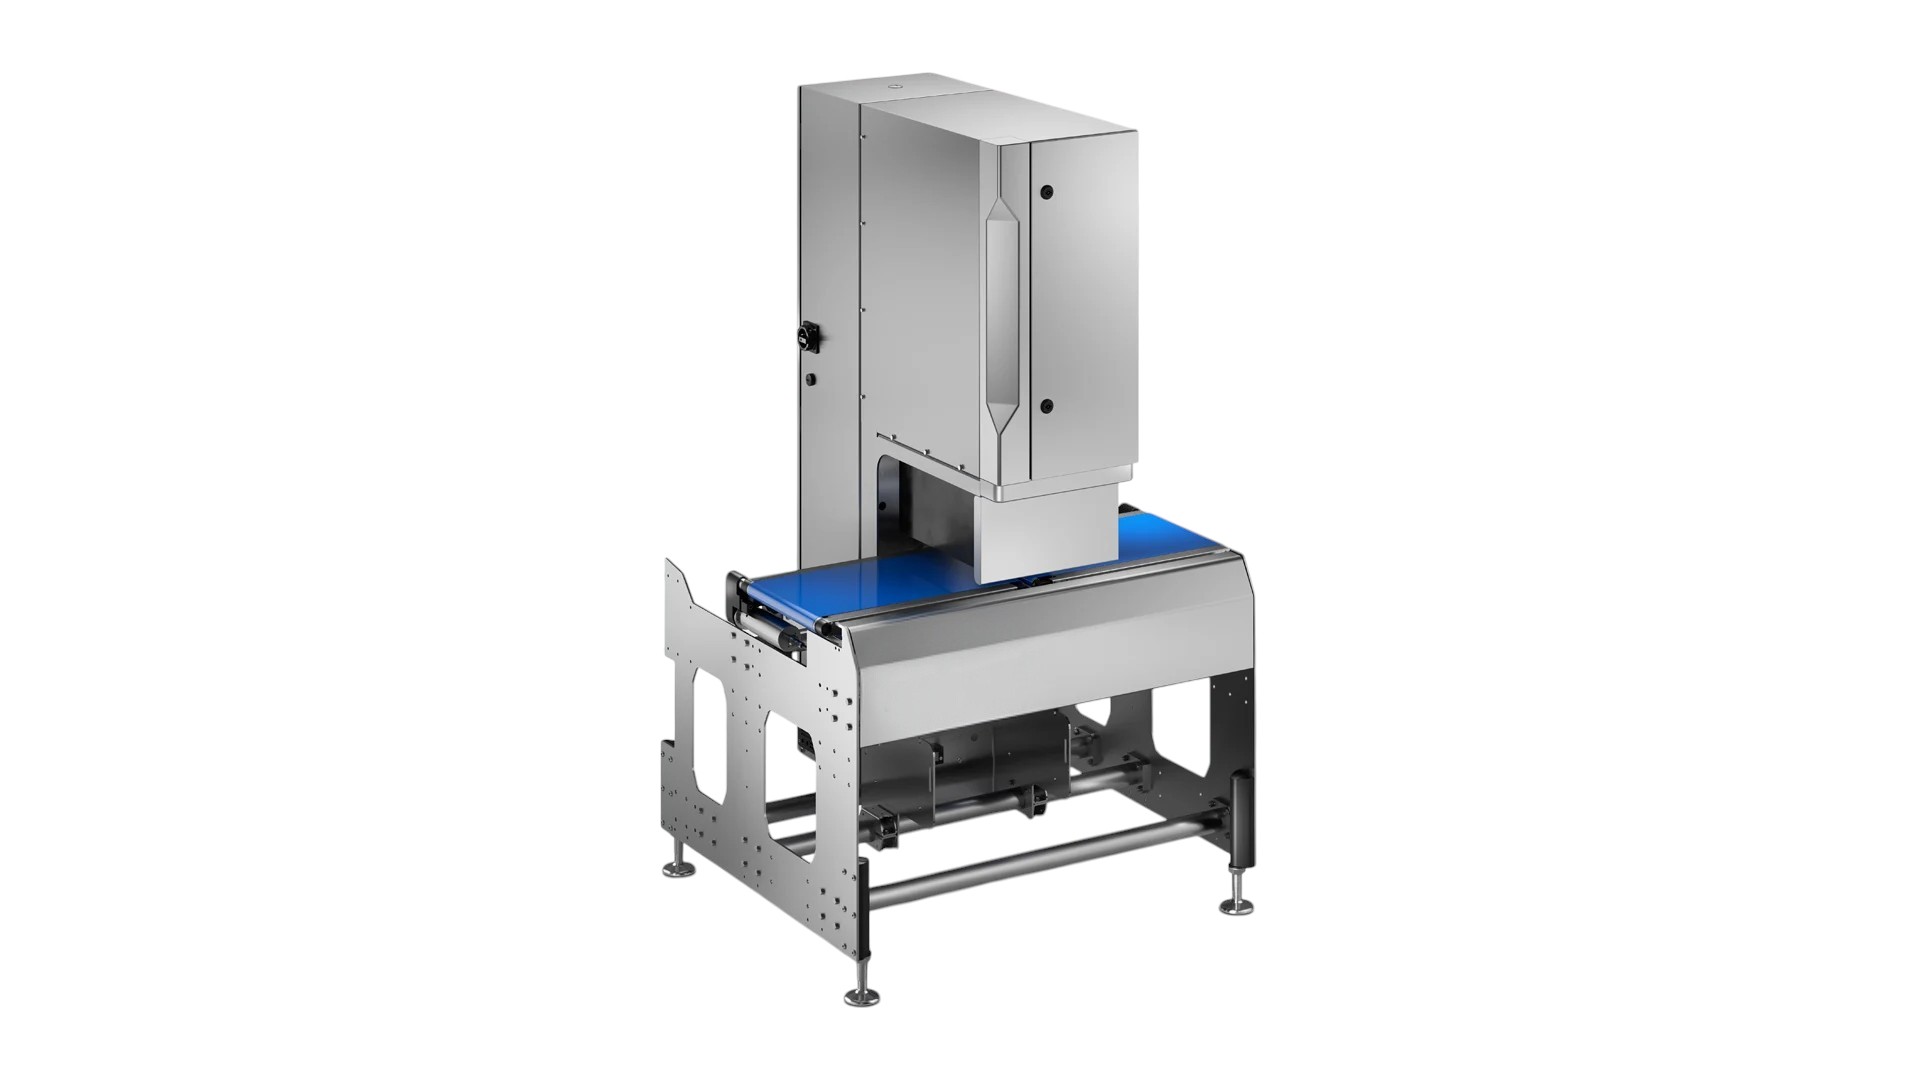
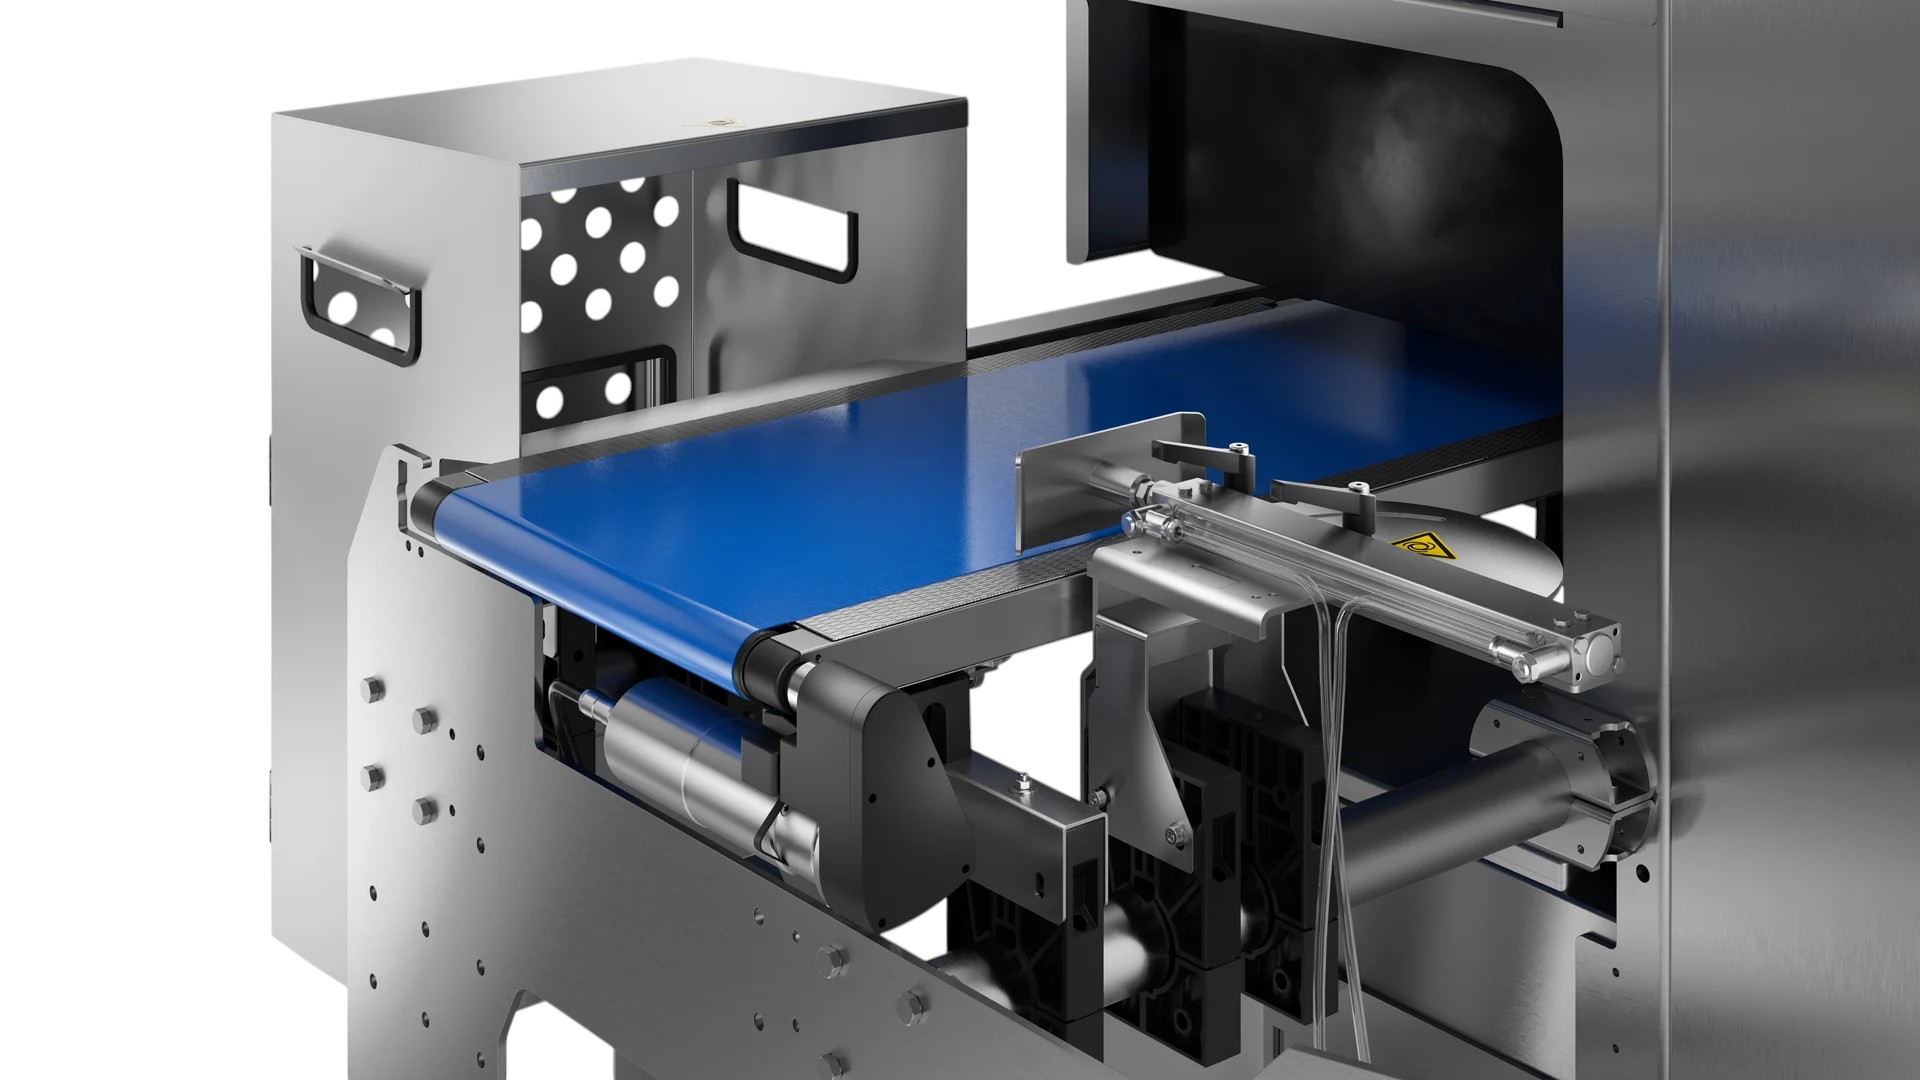
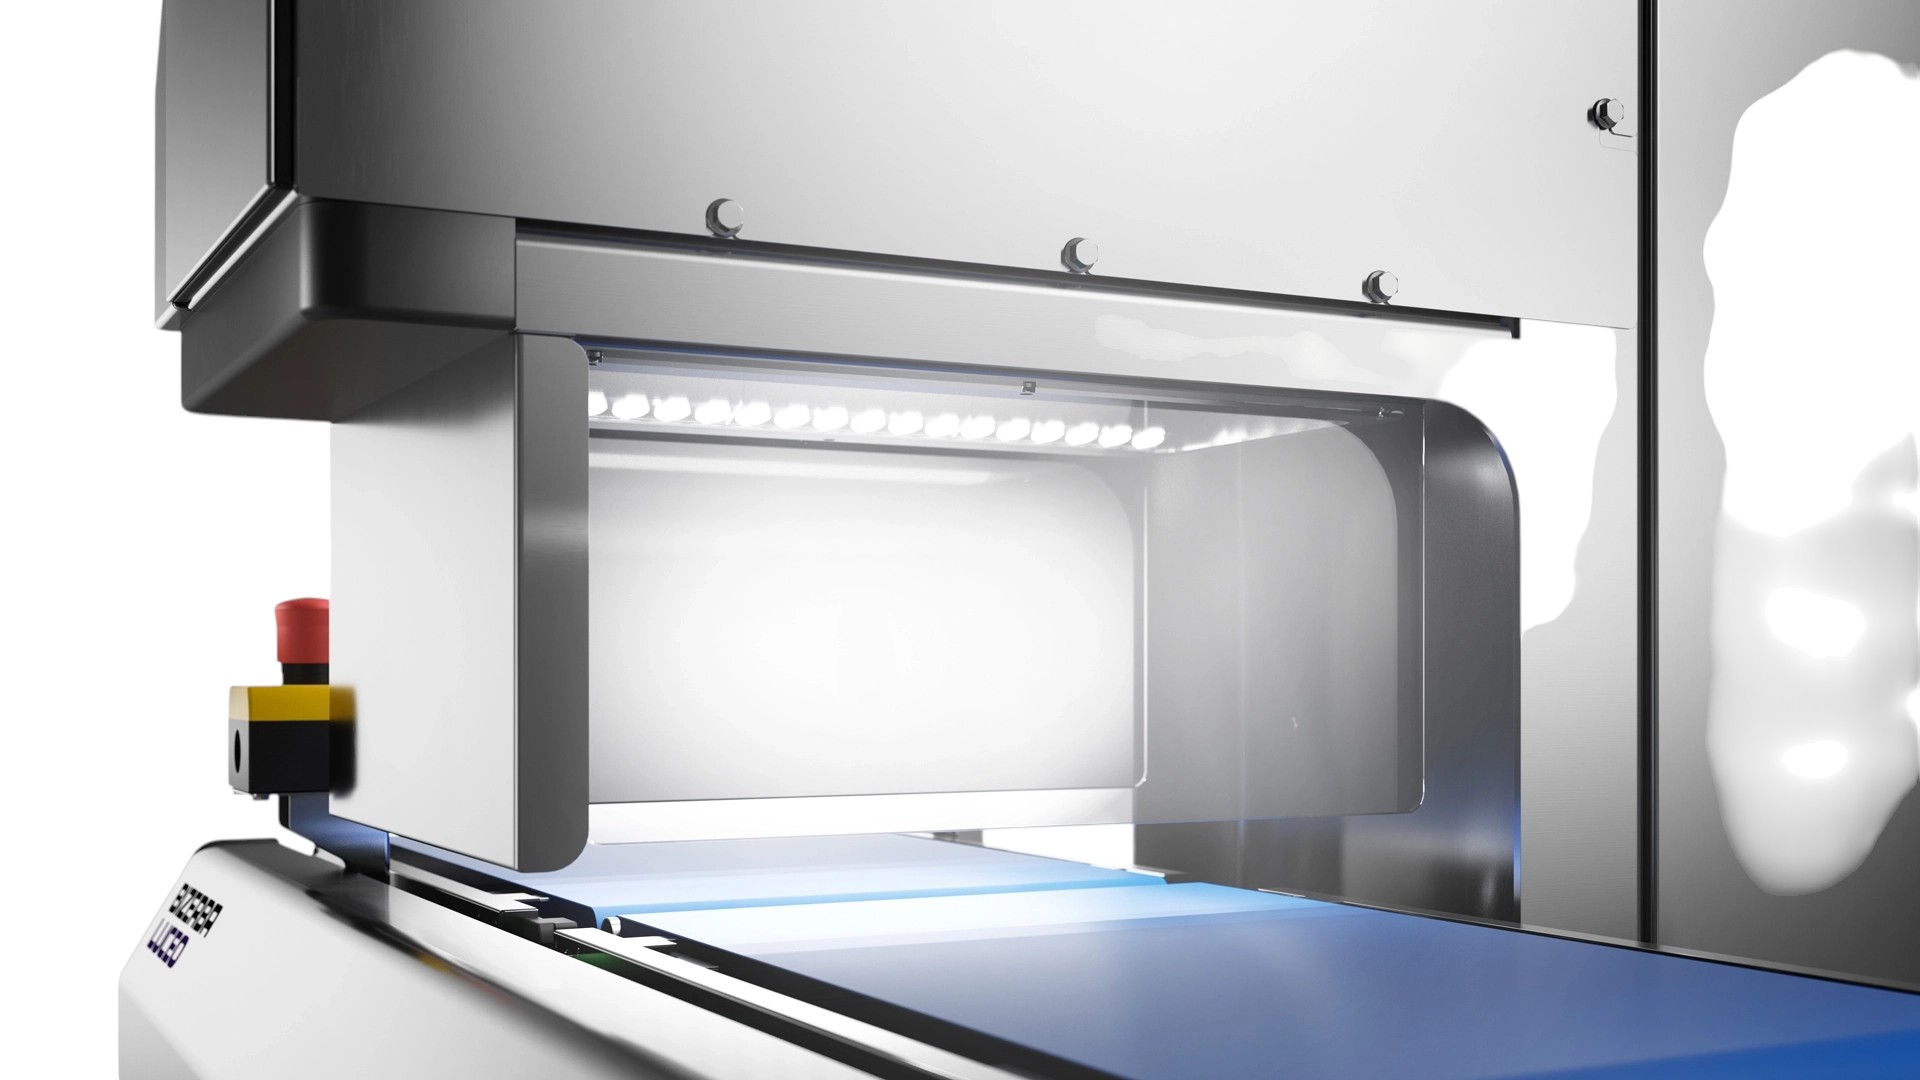
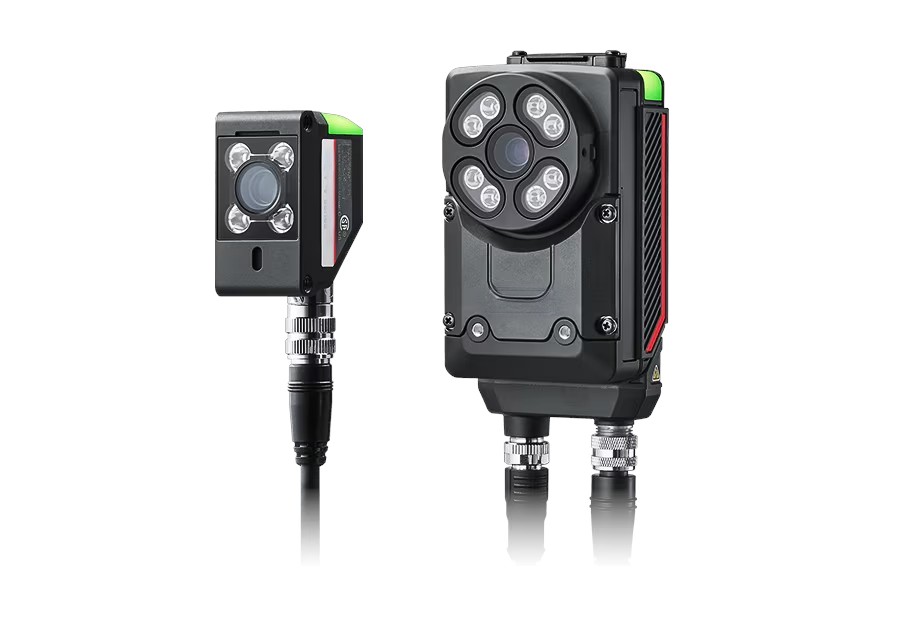
Our Vision Inspection Systems provide automated visual quality control for a wide range of products and packaging applications. Systems can range from a standalone industrial camera installed over an existing conveyor to a complete inspection system incorporating conveyors, lighting, controls, guarding and automatic product rejection.
Vision technology can perform 100% inline inspection at production speed, providing consistent inspection criteria while reducing reliance on manual visual checks. Depending on the application, systems can use one or multiple cameras with customized lenses and lighting to inspect products from the top, bottom, sides or multiple angles.
Applications include label presence and positioning, barcode and 2D code reading, OCR/OCV text verification, date and lot code inspection, cap or component presence, product counting, dimensional checks, orientation, assembly verification, color inspection and surface defect detection. Vision systems can process images to perform measurement, positioning, counting, character/code reading and defect detection, with results used for automatic pass/fail decisions.
For packaging applications, complete vision systems can inspect trays, flow packs, pouches, cartons, boxes, bottles, cans, jars and other packaged products. They can verify that the correct label is present and readable and identify packaging or product defects before products continue downstream.
More advanced systems can perform seal and package integrity inspection, identifying problems such as contaminated or defective seal areas. These applications are particularly useful for thermoformed packages, top-sealed trays and flow packs.
Inspection results can be connected to an automatic reject system to remove products that do not meet the programmed criteria. Depending on the application, images and inspection results can also be stored for quality assurance, production reporting and traceability.
From a single-camera verification station to a fully integrated multi-camera inspection system, each solution can be configured around the product, inspection requirements, line speed and production environment.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad