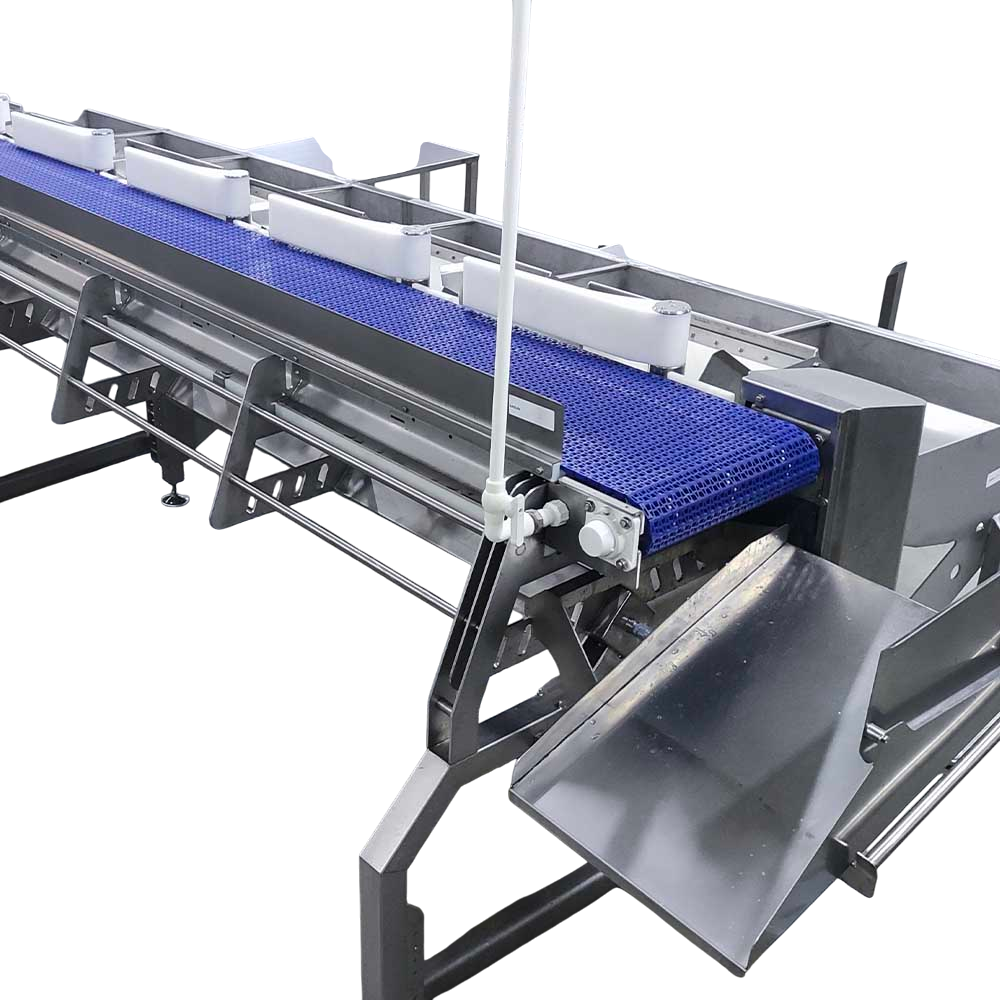
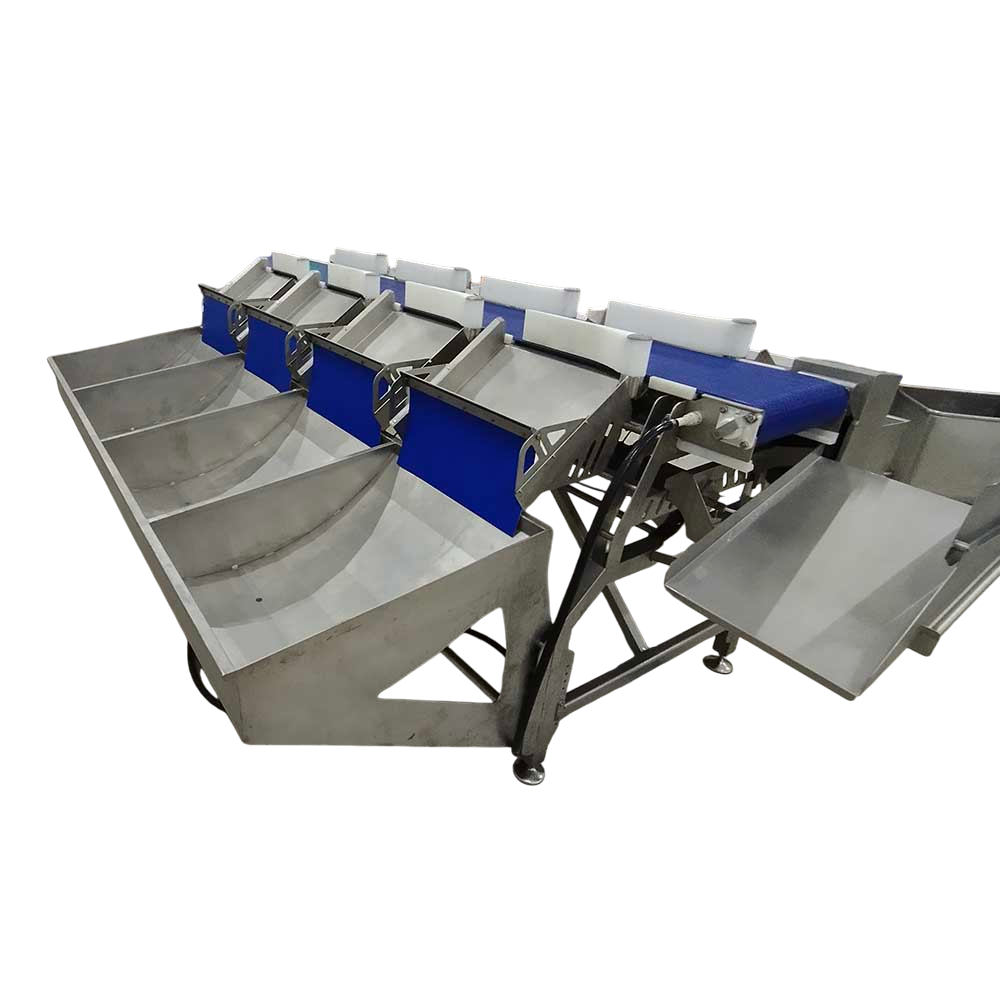
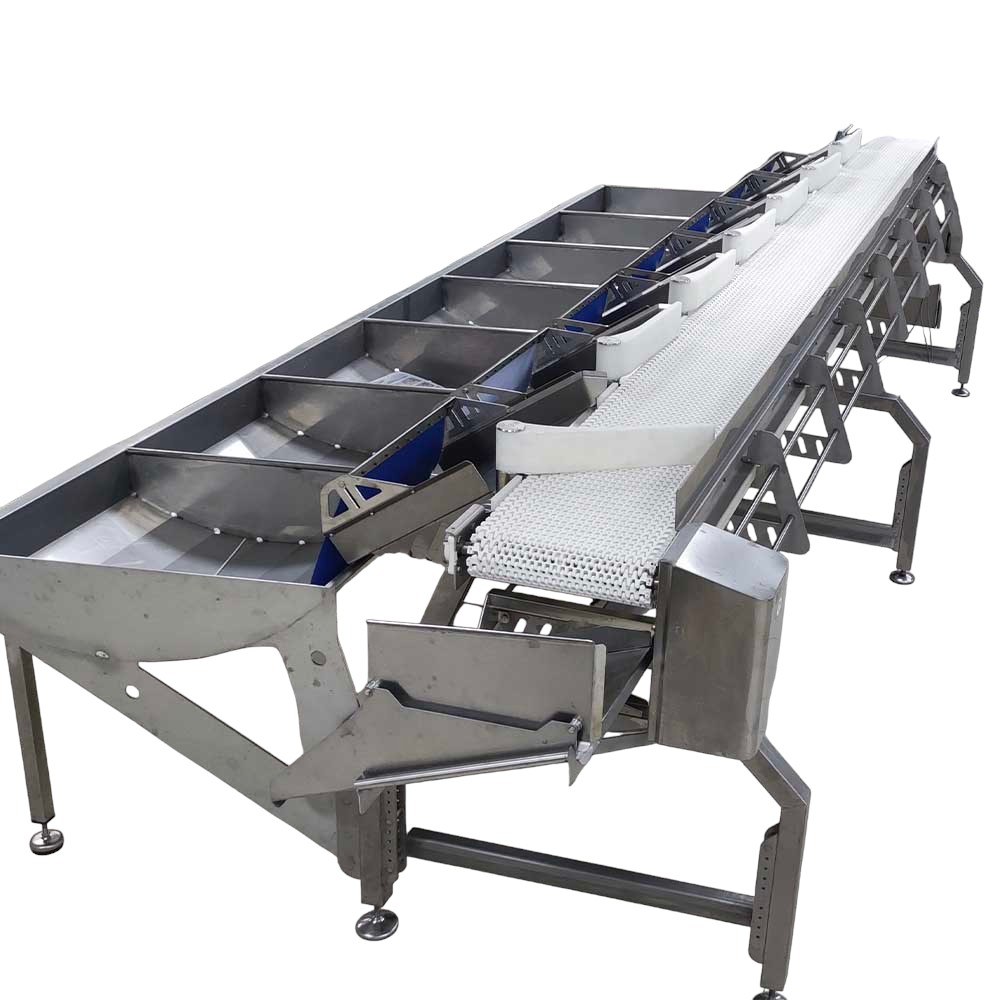
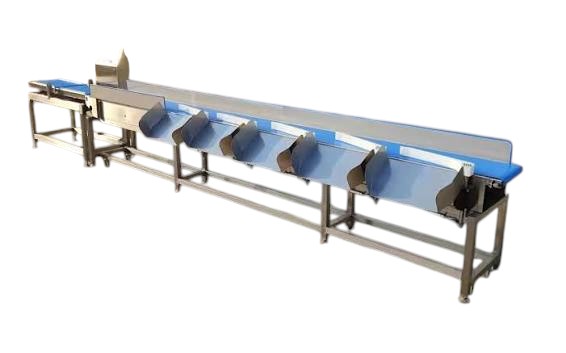
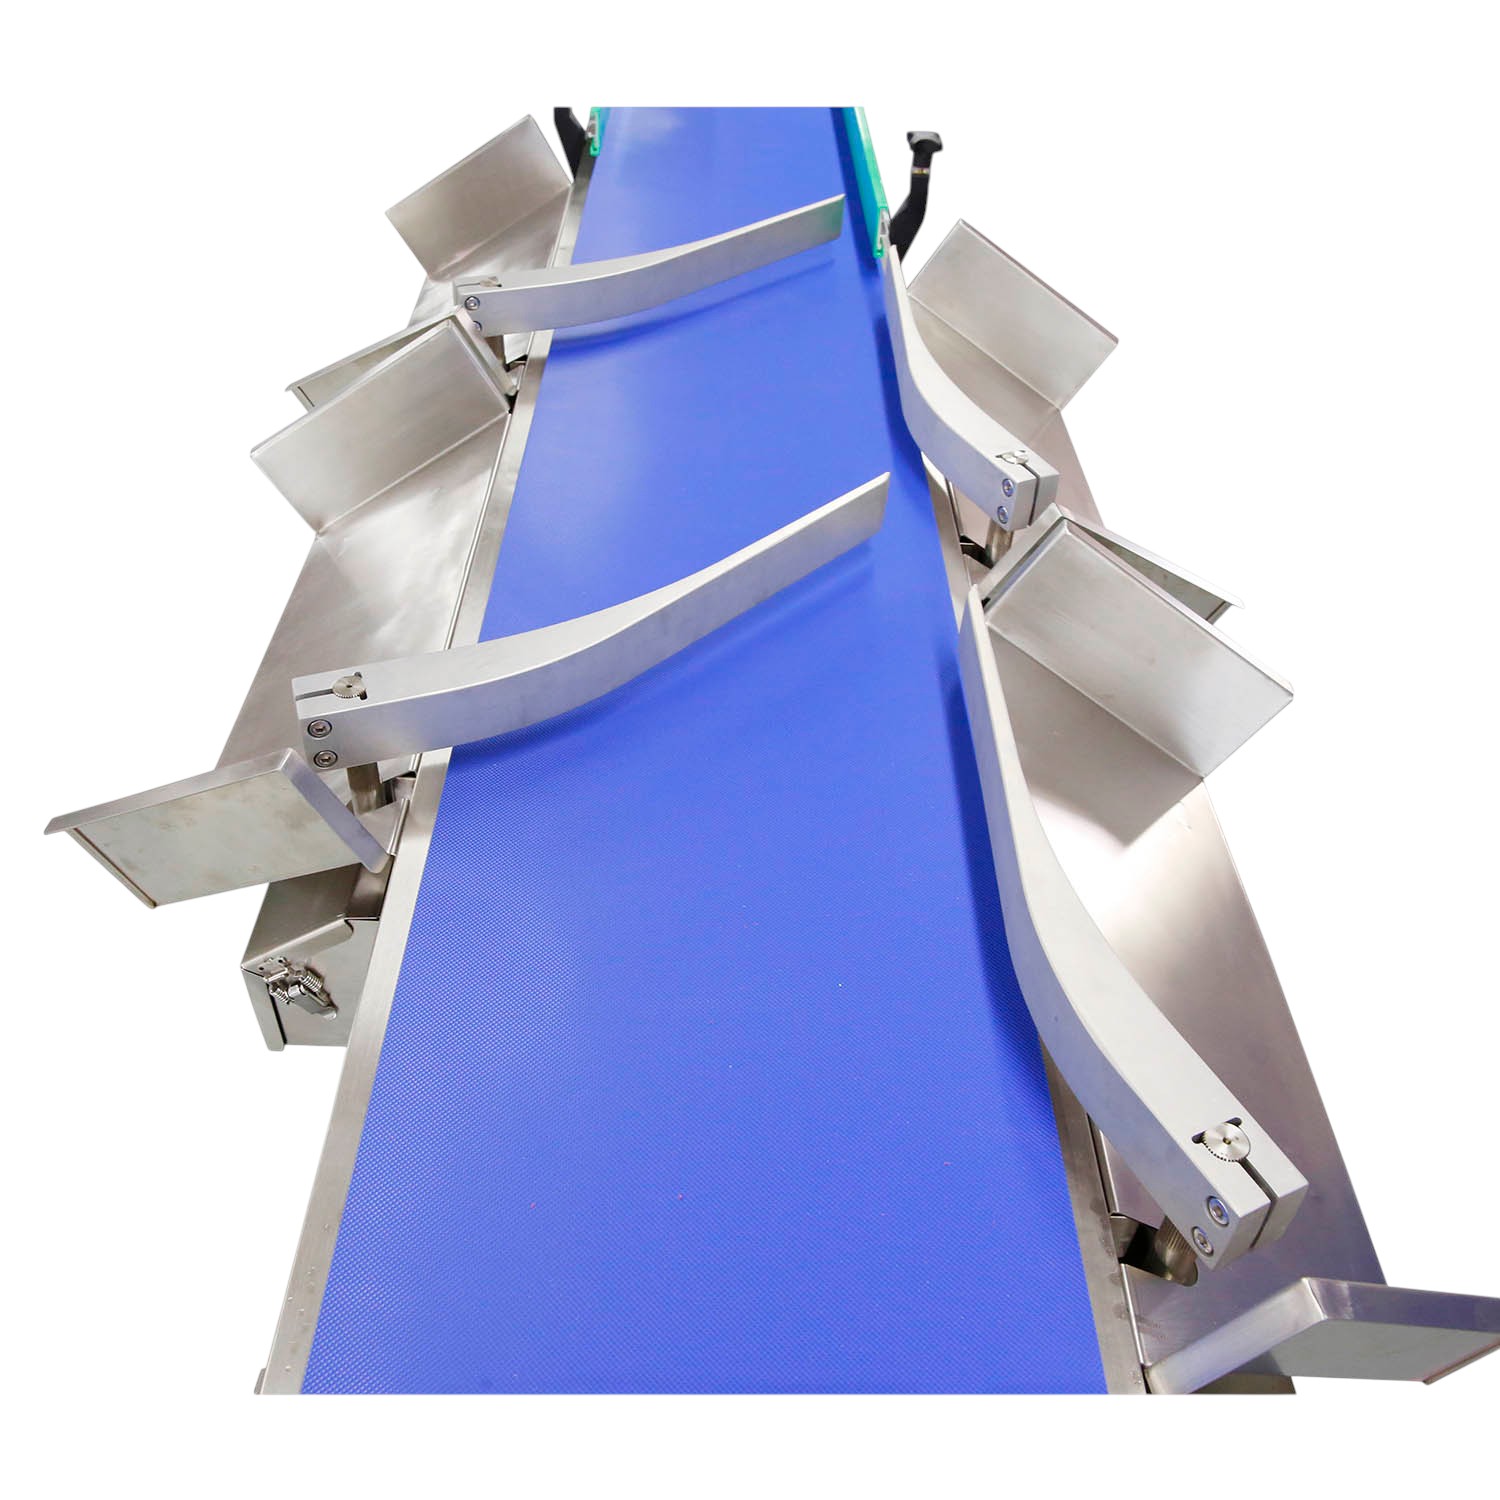
Saturn Grading Conveyor Systems are designed to automatically sort and distribute products into different weight classifications following an inline checkweigher. Each product is dynamically weighed, assigned to the appropriate weight range, and transported along the grading conveyor to its designated discharge station.
The system can incorporate multiple grading stations along a single conveyor, allowing products to be separated into several predefined weight categories. The number of grades and weight ranges can be customized according to the application and production requirements.
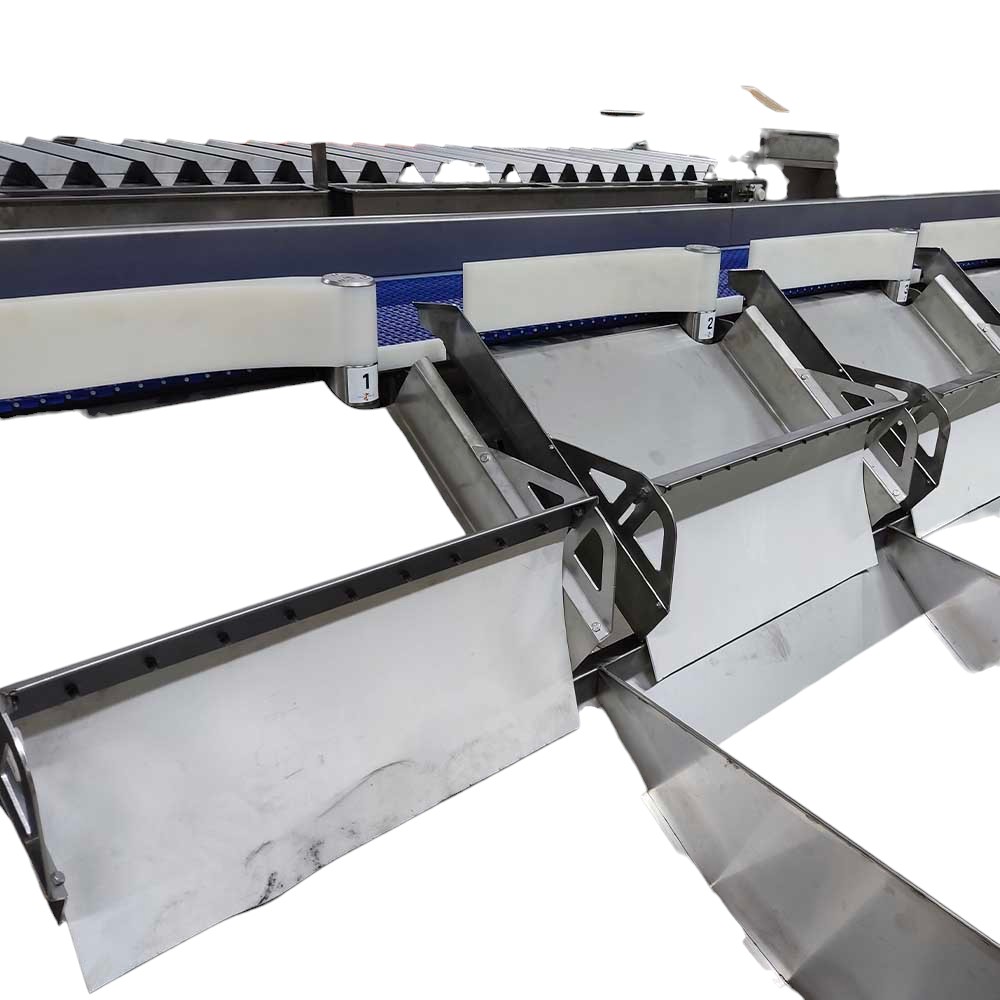
Swing-arm diverters positioned along the conveyor automatically redirect products when they reach their assigned grading station. Each swing arm is controlled according to the weight information received from the upstream checkweigher, providing accurate and repeatable product distribution.
Diverted products can be discharged into collection bins, totes or dedicated chutes. Chutes can also transfer products to downstream conveyors, packing stations, containers or additional processing equipment.
The grading conveyor and checkweigher operate as an integrated system. Product tracking ensures that the weight classification determined at the checkweigher remains associated with the correct product as it travels toward the appropriate discharge location.
Grading systems can be designed for a variety of food and industrial products, with conveyor dimensions, belt technology, number of grading stations and discharge arrangements customized around the product and required production capacity.
For food applications, systems can be supplied with stainless steel construction, food-grade belting and washdown configurations. Product-specific guides, chutes and handling components can be incorporated to provide controlled transfer while minimizing unnecessary product impact.
A separate discharge can also be incorporated for products that are outside the programmed grading ranges or otherwise rejected, depending on the application.
Saturn Grading Conveyor Systems can be supplied together with the checkweigher, grading conveyor, swing-arm diverters, bins or chutes, controls and product tracking as a complete integrated solution.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad