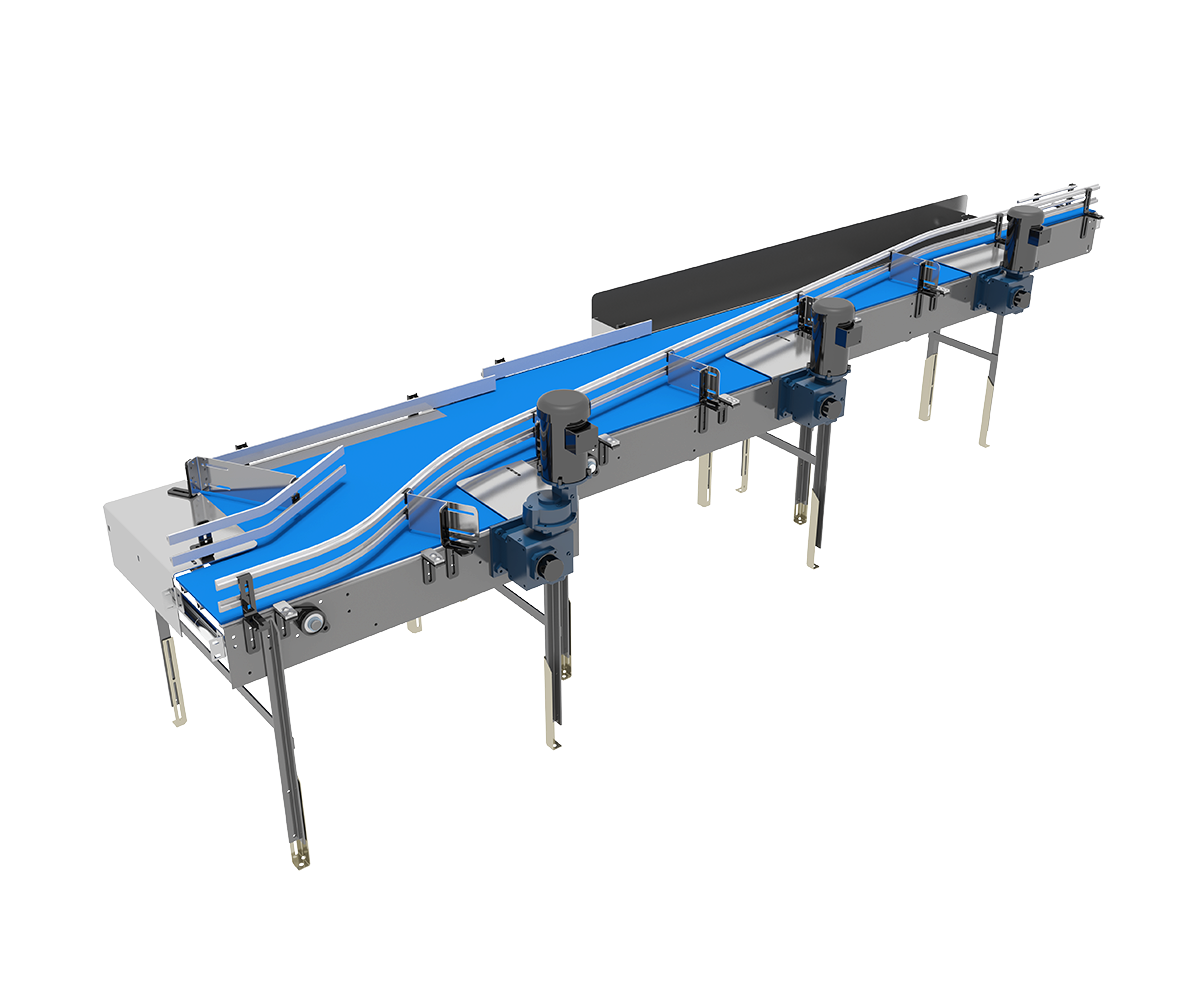
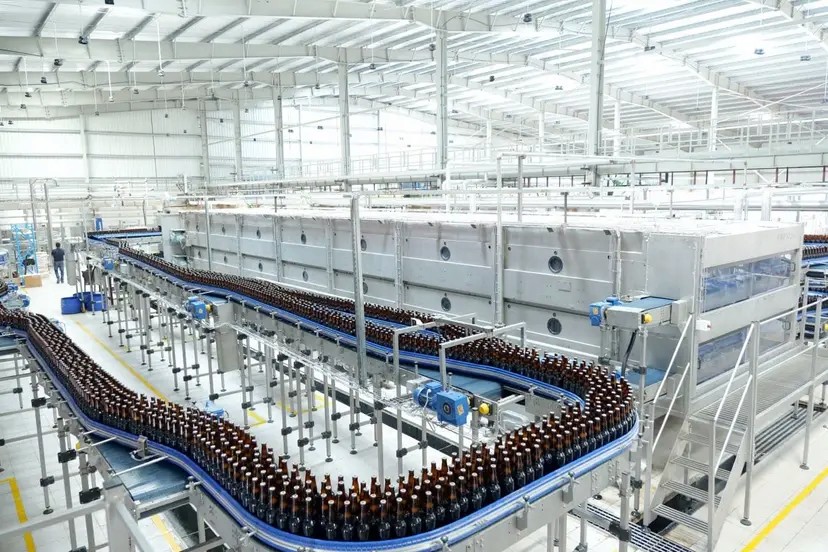
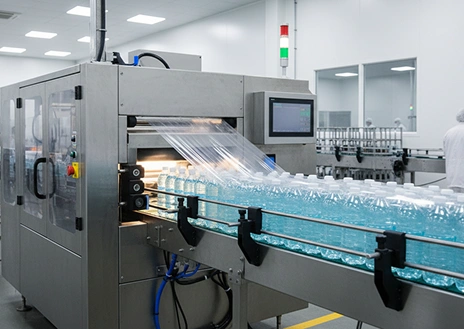
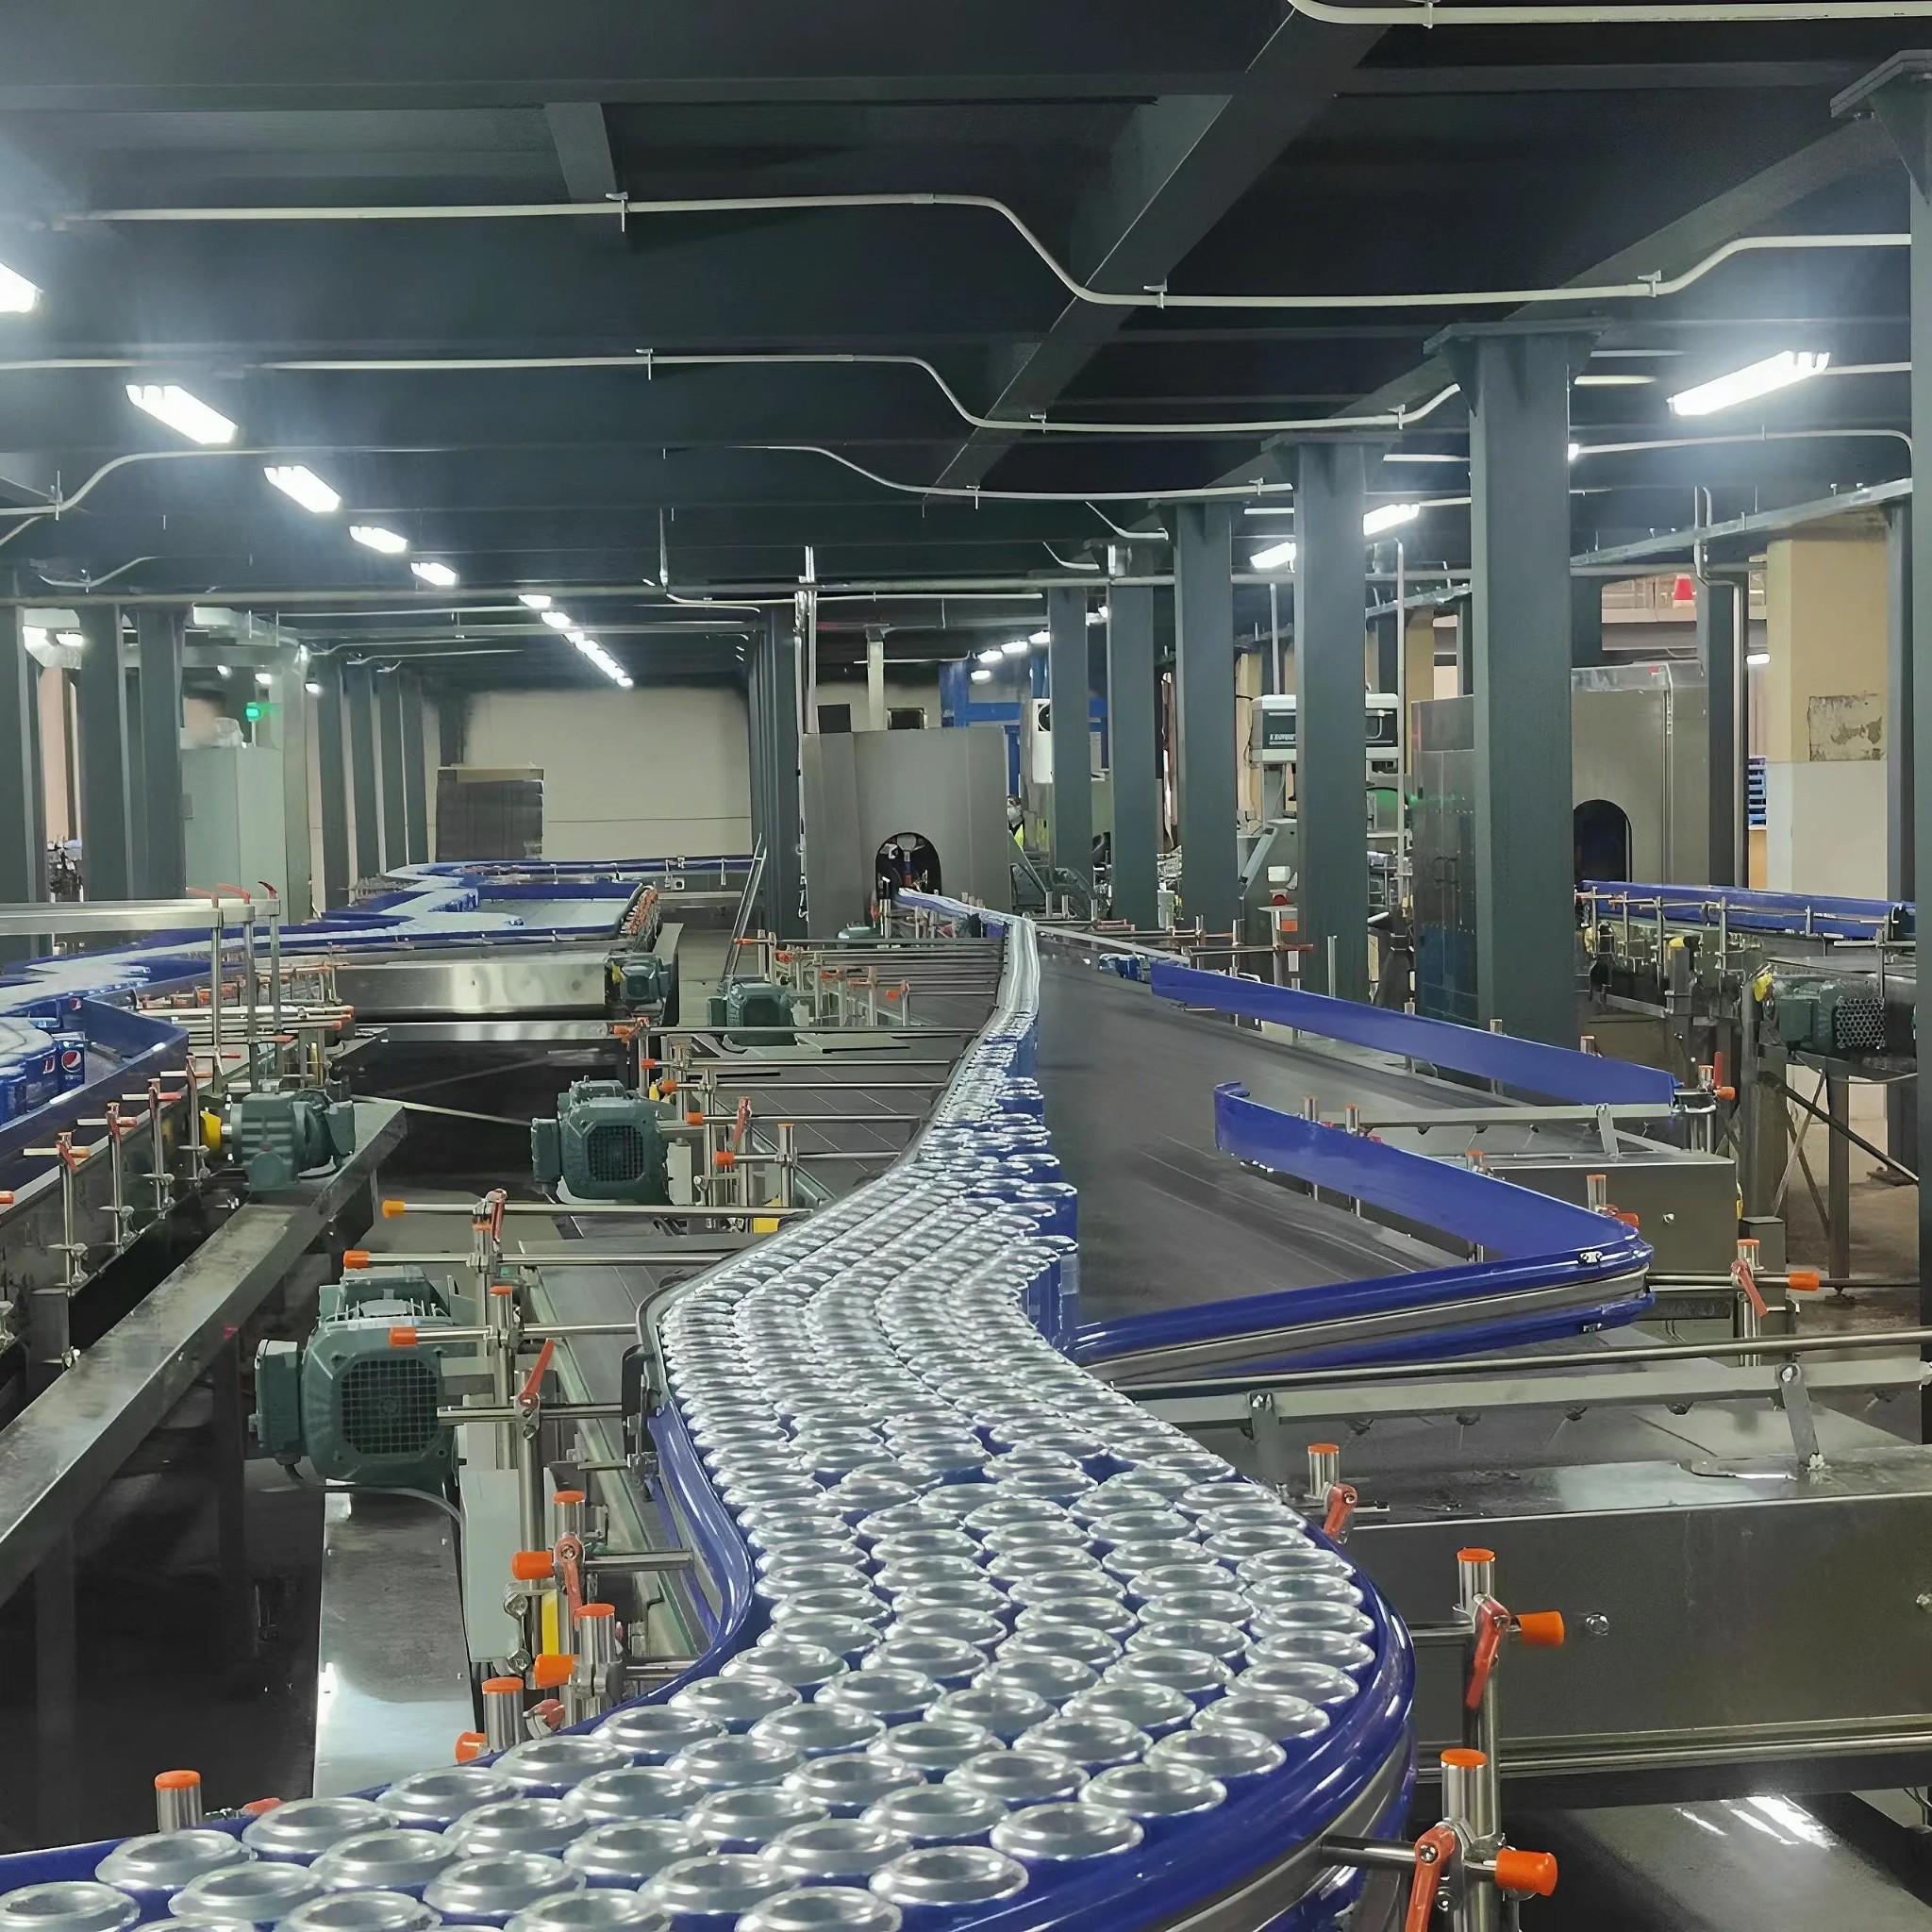
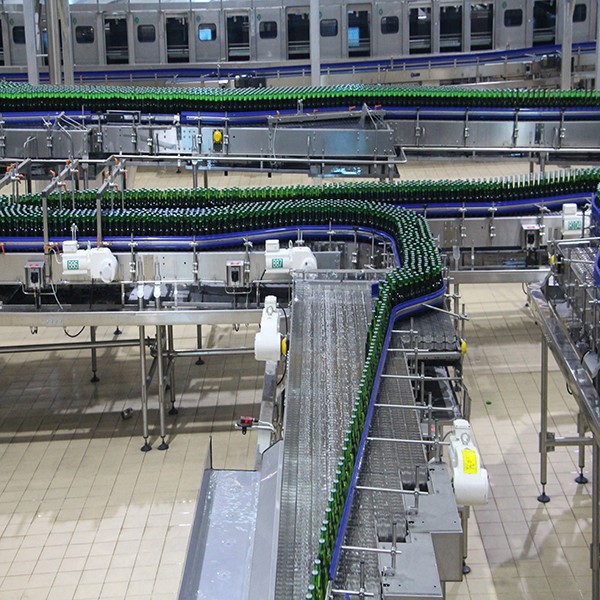
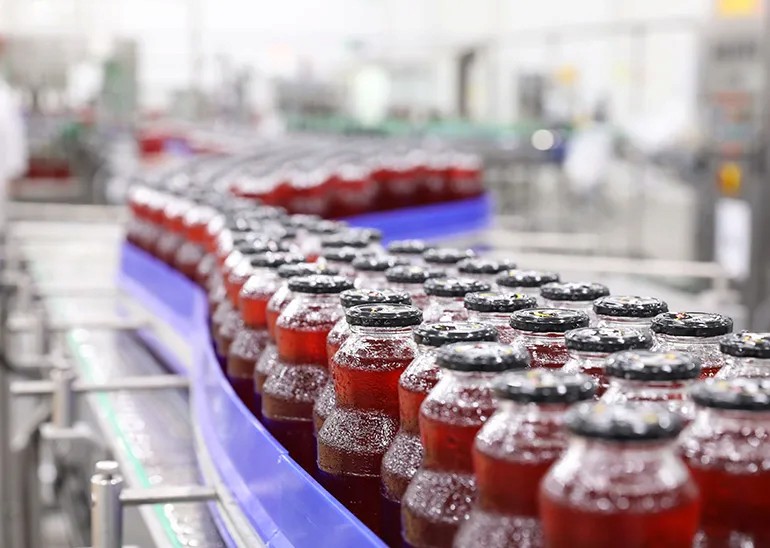
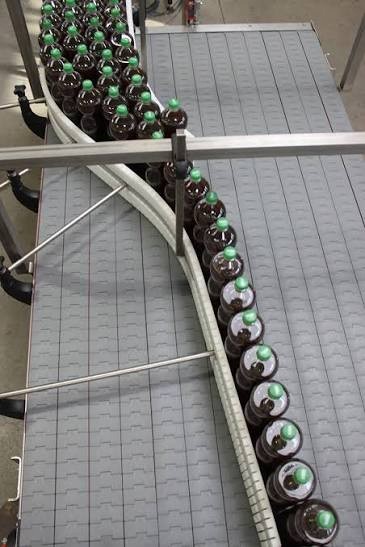
Saturn Mass Flow & Single Filing Conveyors are designed for high-capacity handling of bottles, cans, jars and other rigid containers throughout production, filling and packaging lines.
The system allows products to transition between single-file and mass-flow configurations according to the requirements of the surrounding equipment. Products can expand from a single lane onto a wider conveyor where multiple containers travel side-by-side, then progressively return to single file before entering downstream machinery. Commercial pressureless combining systems use this same mass-flow-to-single-file principle for machine infeeds.
Mass flow conveying provides increased product capacity and can create valuable accumulation between machines operating at different speeds. The wider conveying surface allows multiple containers to travel simultaneously while helping the line absorb short production interruptions and variations in equipment speed.
Single filing progressively organizes containers from mass flow into a controlled single-lane stream. Conveyor speeds, guide geometry and lane transitions are engineered around the container dimensions, stability and required production rate. Using different conveyor speeds to progressively separate container flow is an established approach for achieving stable single-file presentation.
Systems can be designed for low-pressure or pressureless product handling to minimize excessive container-to-container pressure during accumulation and single filing. This is particularly beneficial for lightweight, unstable or sensitive containers.
Mass Flow & Single Filing Conveyors can handle empty or filled PET bottles, glass bottles, cans, jars and other containers, with layouts customized for round, square and other suitable container geometries.
Multiple conveyor sections can operate at independently controlled speeds, allowing products to expand, accumulate, converge and single file smoothly. Sensors and PLC controls can automatically regulate conveyor speeds according to upstream and downstream production conditions.
Systems can incorporate tabletop chain, MatTop or plastic modular belt technologies, with custom side guides and transitions designed specifically for the product.
Construction is available in painted steel or stainless steel, with washdown configurations available for food, beverage and other wet production environments.
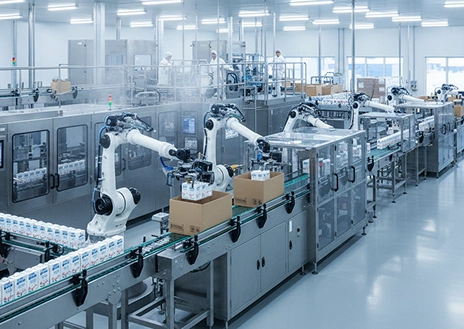
Saturn Mass Flow & Single Filing Conveyors can be integrated with depalletizers, rinsers, fillers, cappers, labelers, inspection systems, accumulation systems, packers and complete bottling or packaging lines.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad