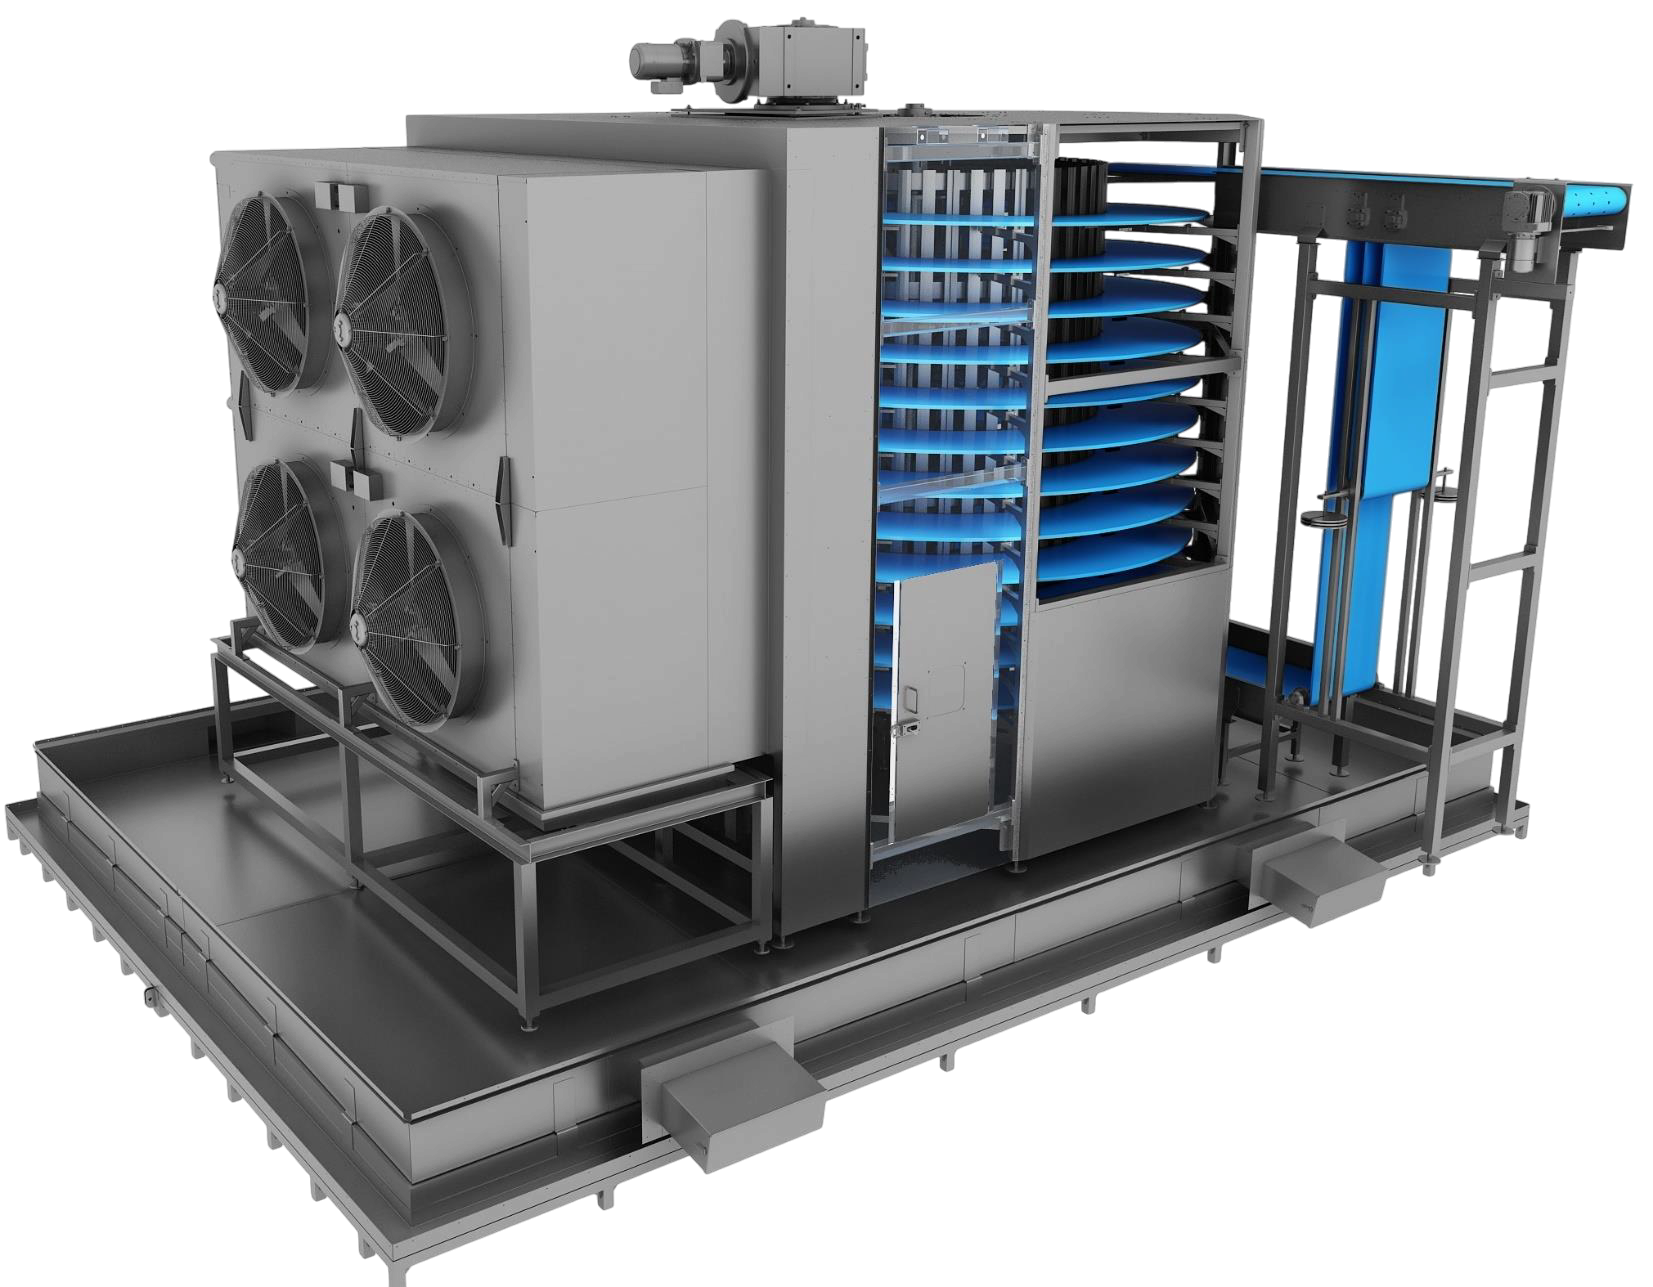
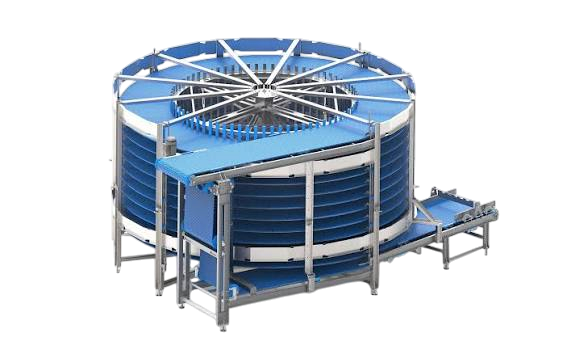
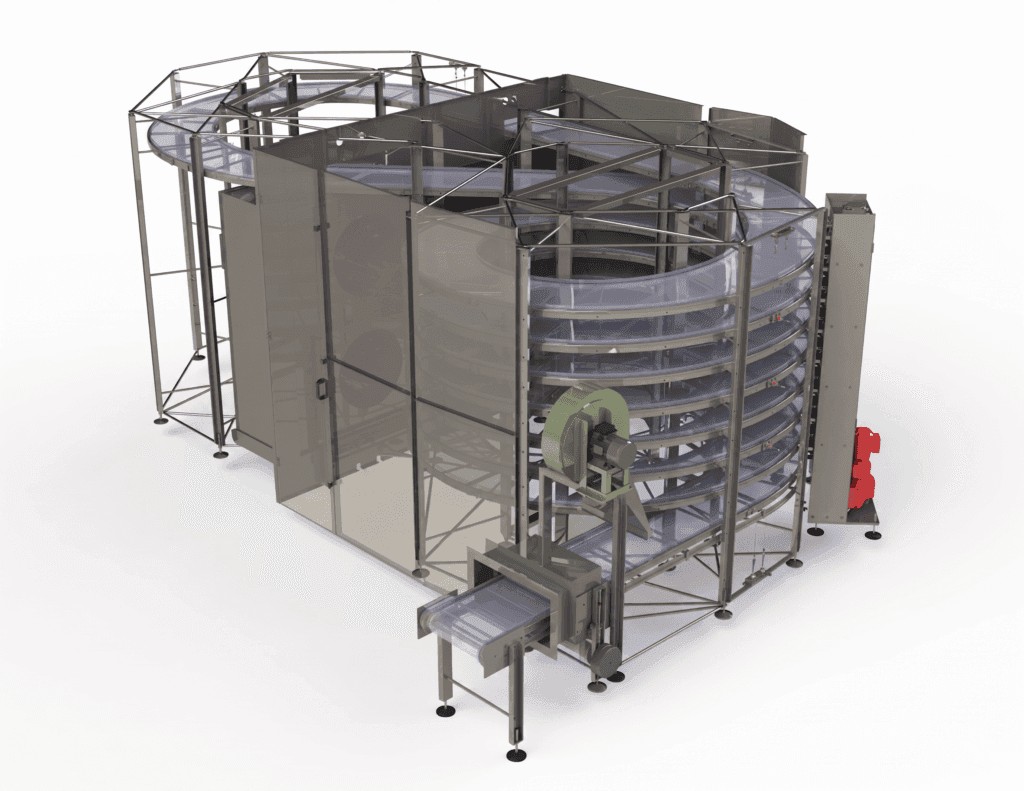
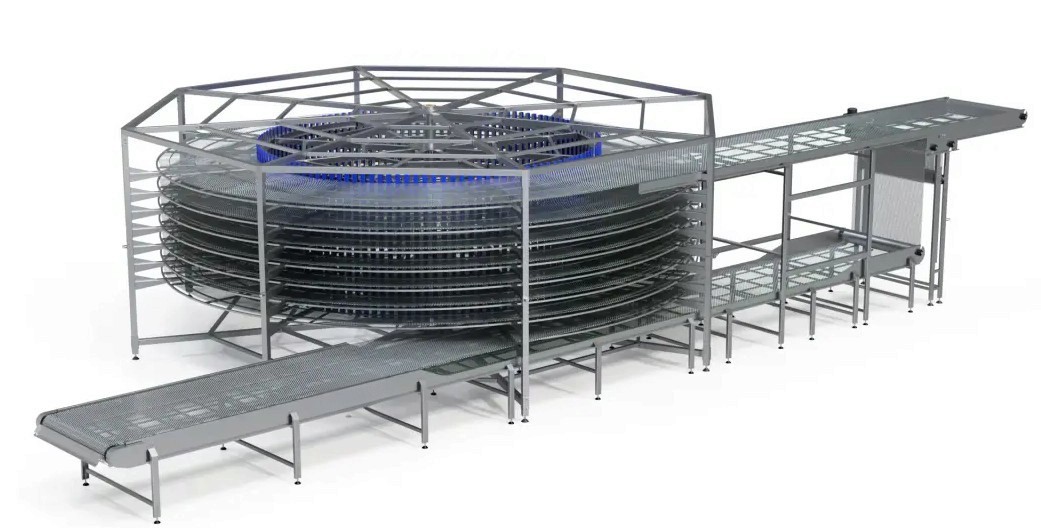
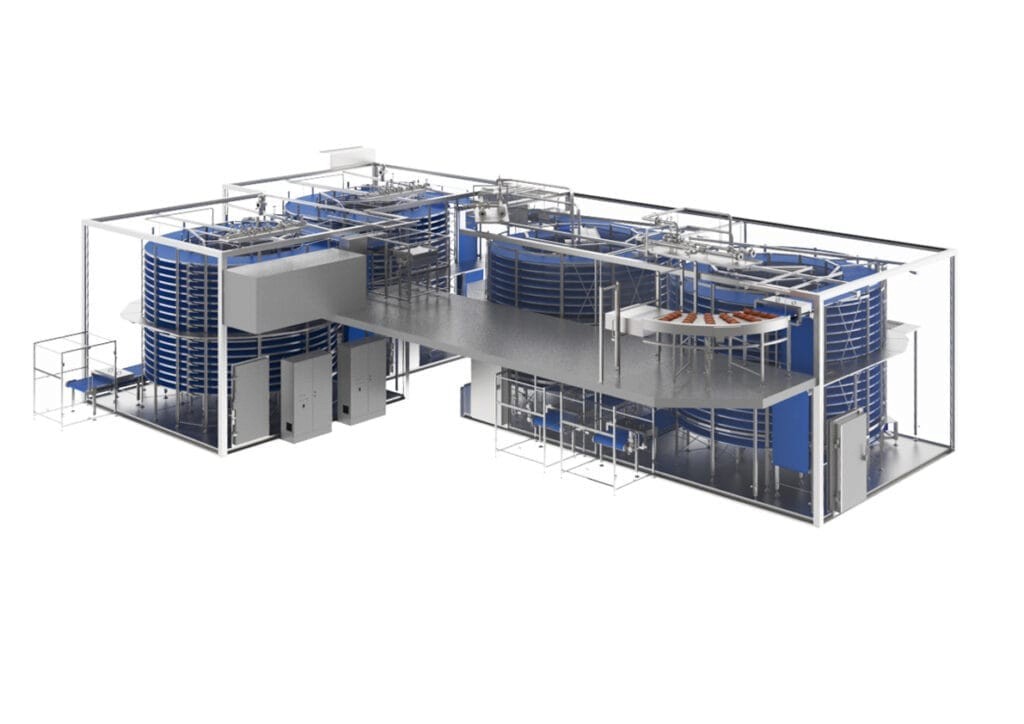
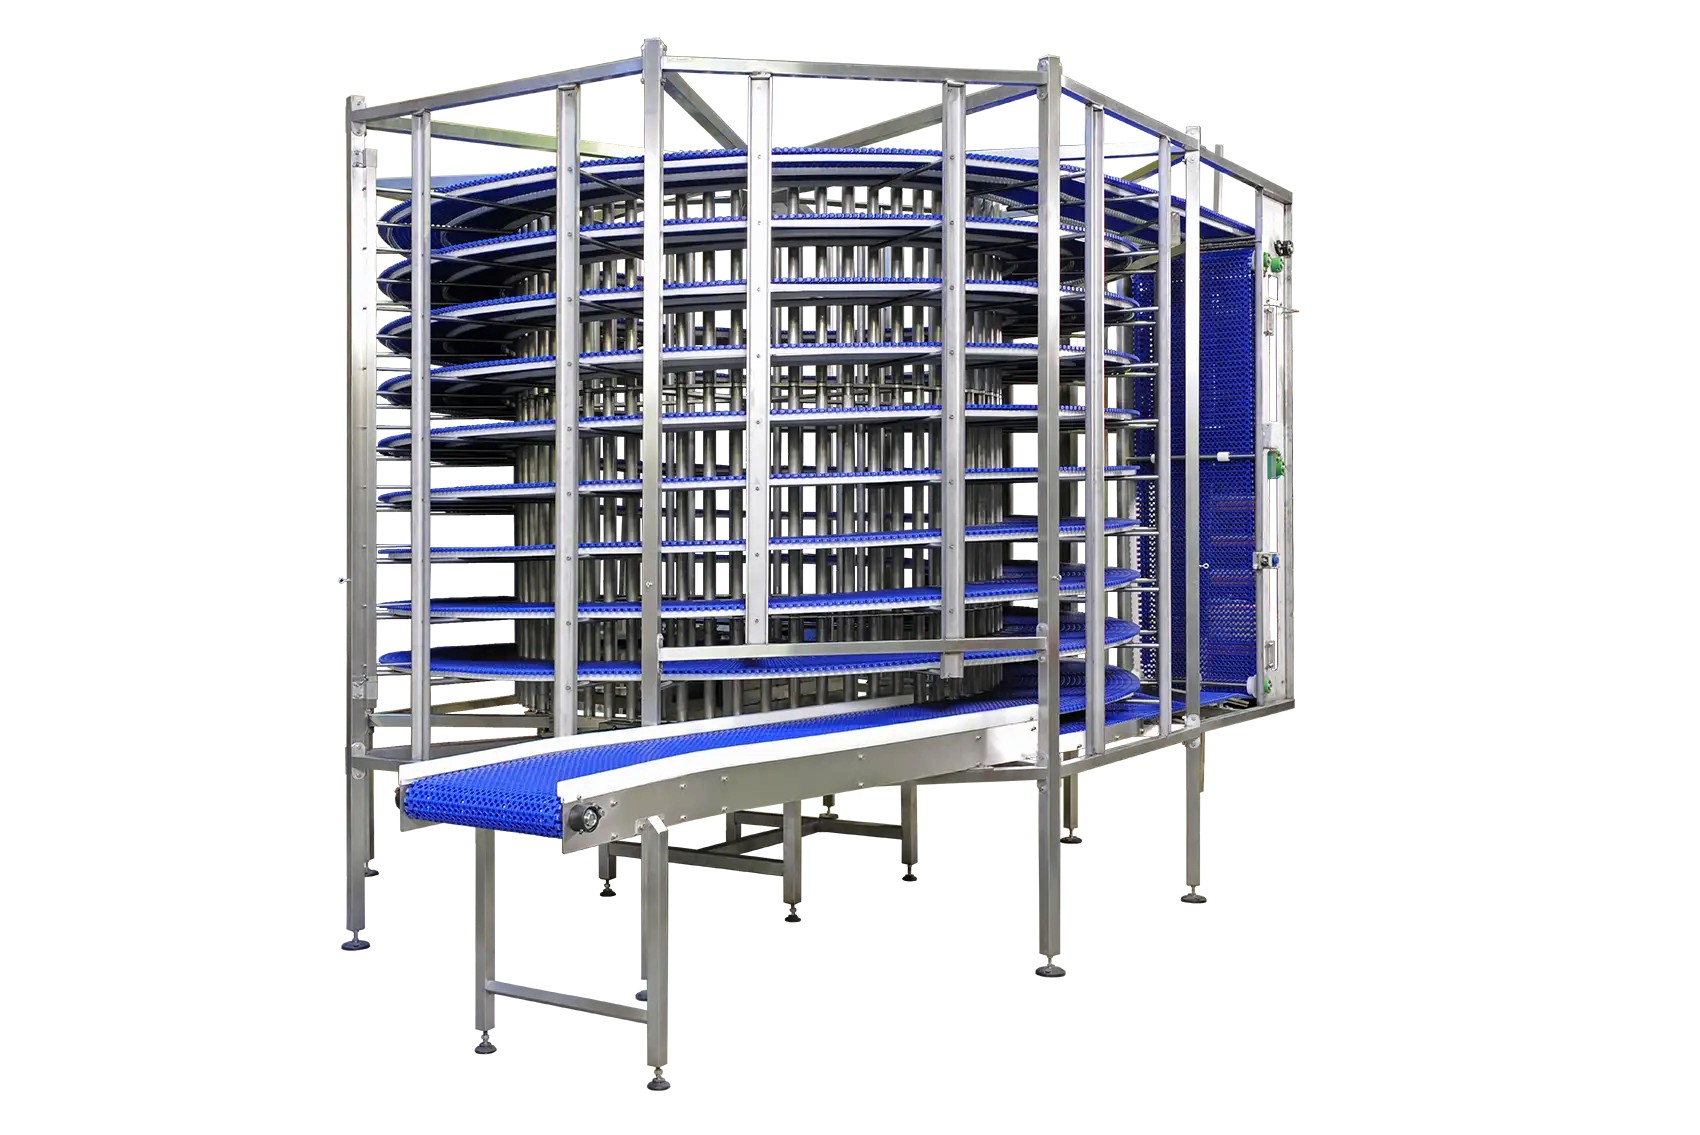
Saturn Cooling & Freezing Spirals provide continuous temperature-controlled conveying for food processing and packaging lines. Their compact, multi-tier design creates an extended conveyor path, allowing products to cool or freeze over longer residence times while minimizing the required floor space.
Systems can be configured for ambient cooling, forced-air cooling, refrigerated cooling, blast freezing or Individual Quick Freezing (IQF), depending on the product, production capacity and required discharge temperature.
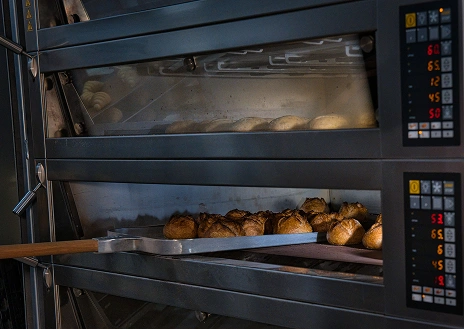
Cooling Spirals are designed to gradually reduce product temperature following baking, cooking or frying. Open ambient cooling spirals use surrounding air, while forced-air configurations incorporate fans and controlled airflow to accelerate cooling. Enclosed systems can provide more controlled cooling conditions for temperature-sensitive products.
Freezing Spirals incorporate insulated enclosures and industrial refrigeration systems to rapidly reduce product temperatures. High-velocity cold air circulates around the products to provide consistent freezing performance. Systems can also be configured for IQF applications, allowing suitable individual food products to be frozen quickly while minimizing product clumping and adhesion.
Spirals can be equipped with stainless steel metal mesh belts or plastic modular belts. Metal mesh belts provide excellent airflow and heat transfer, while modular plastic belts offer various open-area configurations, belt pitches and product-handling surfaces.
Cooling and freezing spirals are suitable for a wide range of products, including bread, pastries, donuts, tortillas, pizza, pasta, meat, poultry, seafood, vegetables, prepared meals and frozen food products.
Each system can be customized with different spiral diameters, belt widths, number of tiers, conveyor speeds and airflow configurations to achieve the required production capacity and residence time. Refrigeration and airflow systems can be engineered according to the product characteristics and target temperatures.
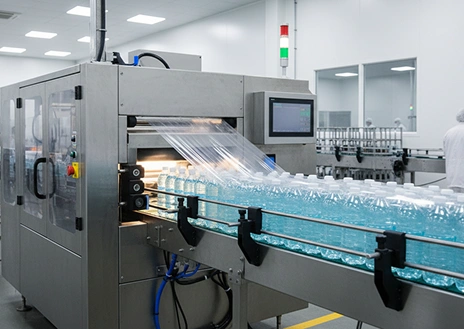
Available with stainless steel sanitary construction, accessible conveyor components, washdown designs and optional automated cleaning systems, Saturn Cooling & Freezing Spirals are designed for demanding food production environments.
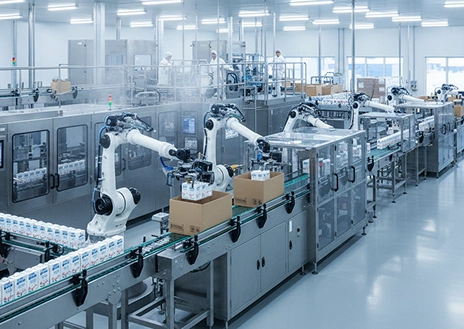
Systems can be supplied as standalone equipment or integrated with ovens, fryers, processing machinery, cooling conveyors, inspection systems, packaging equipment and complete automated production lines.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad