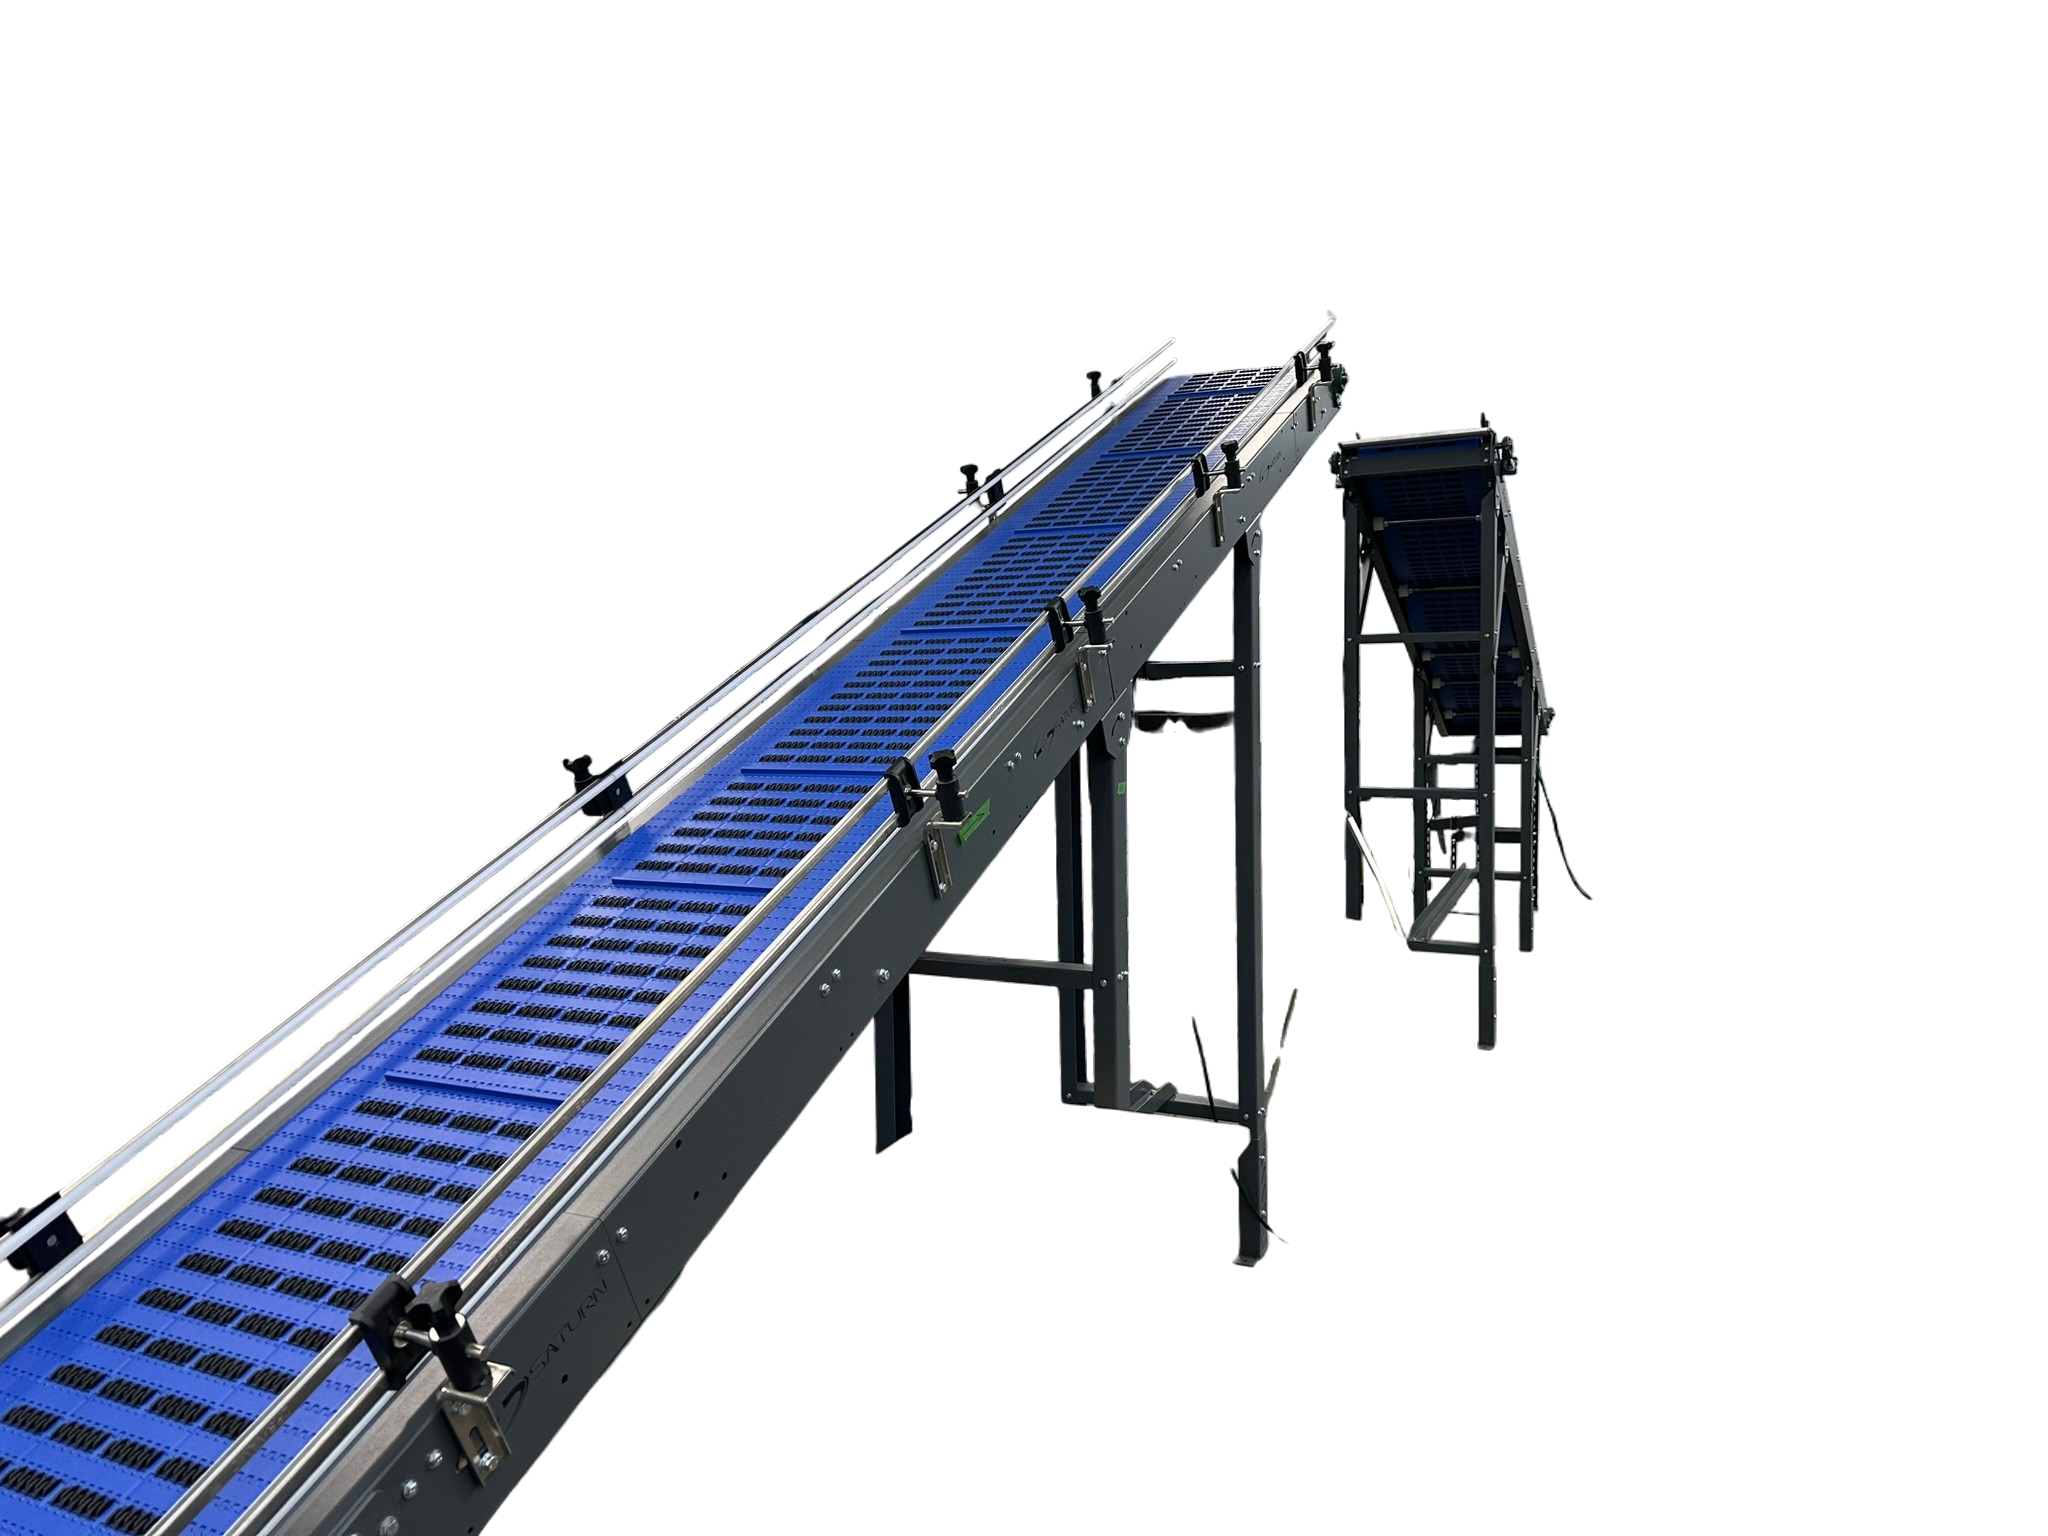
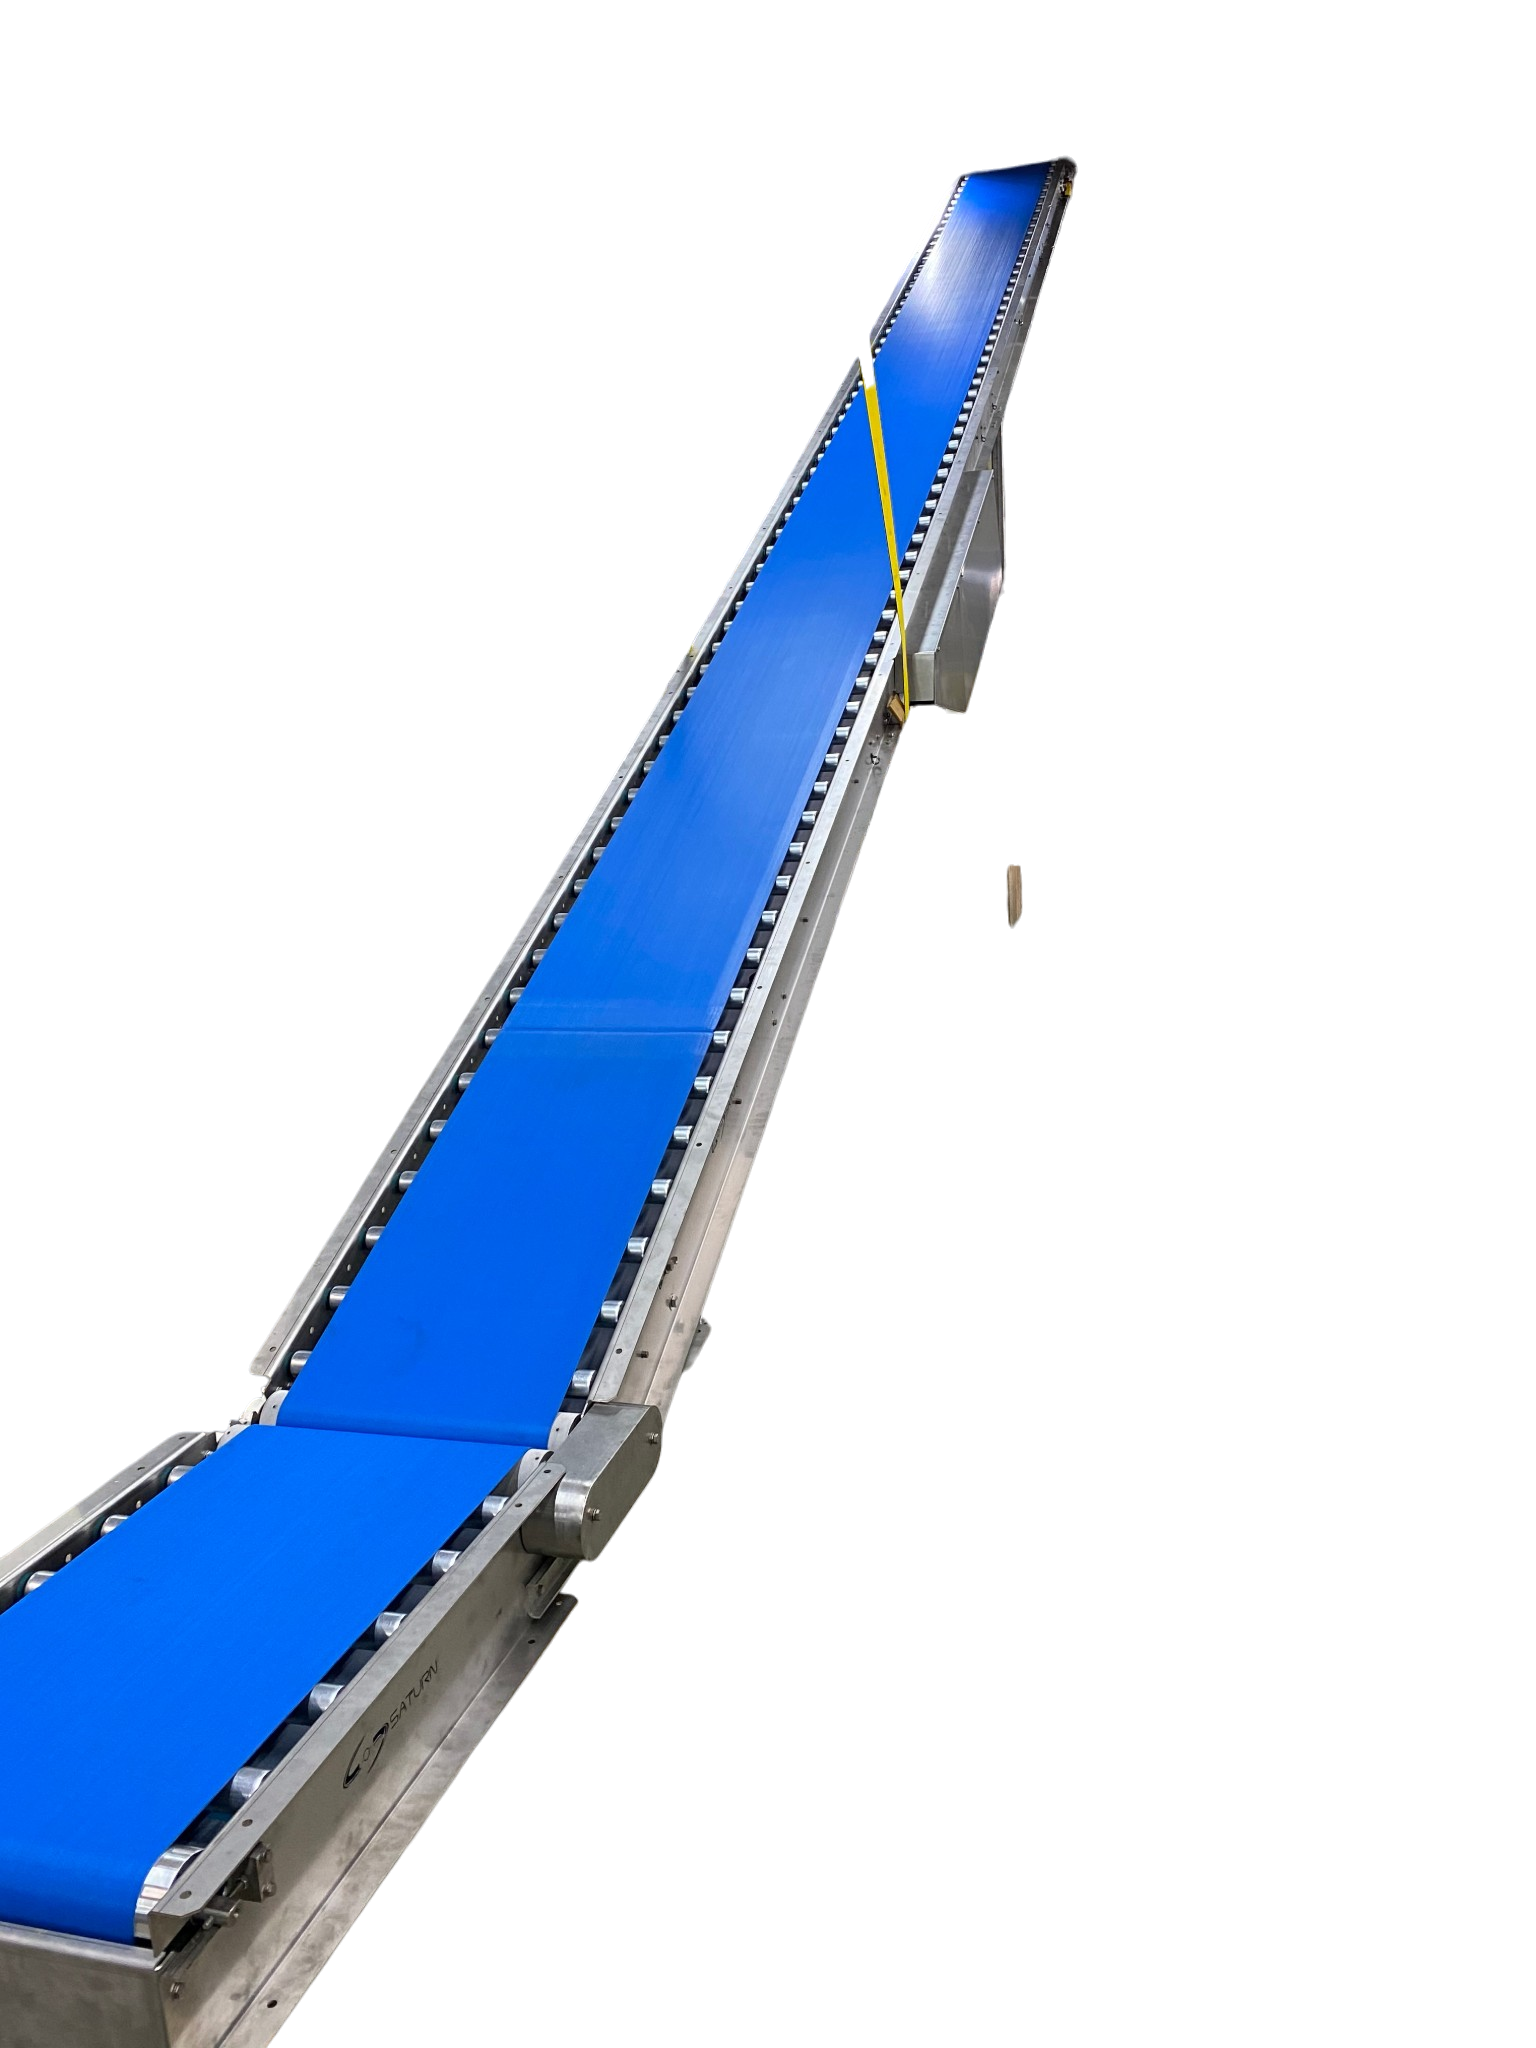
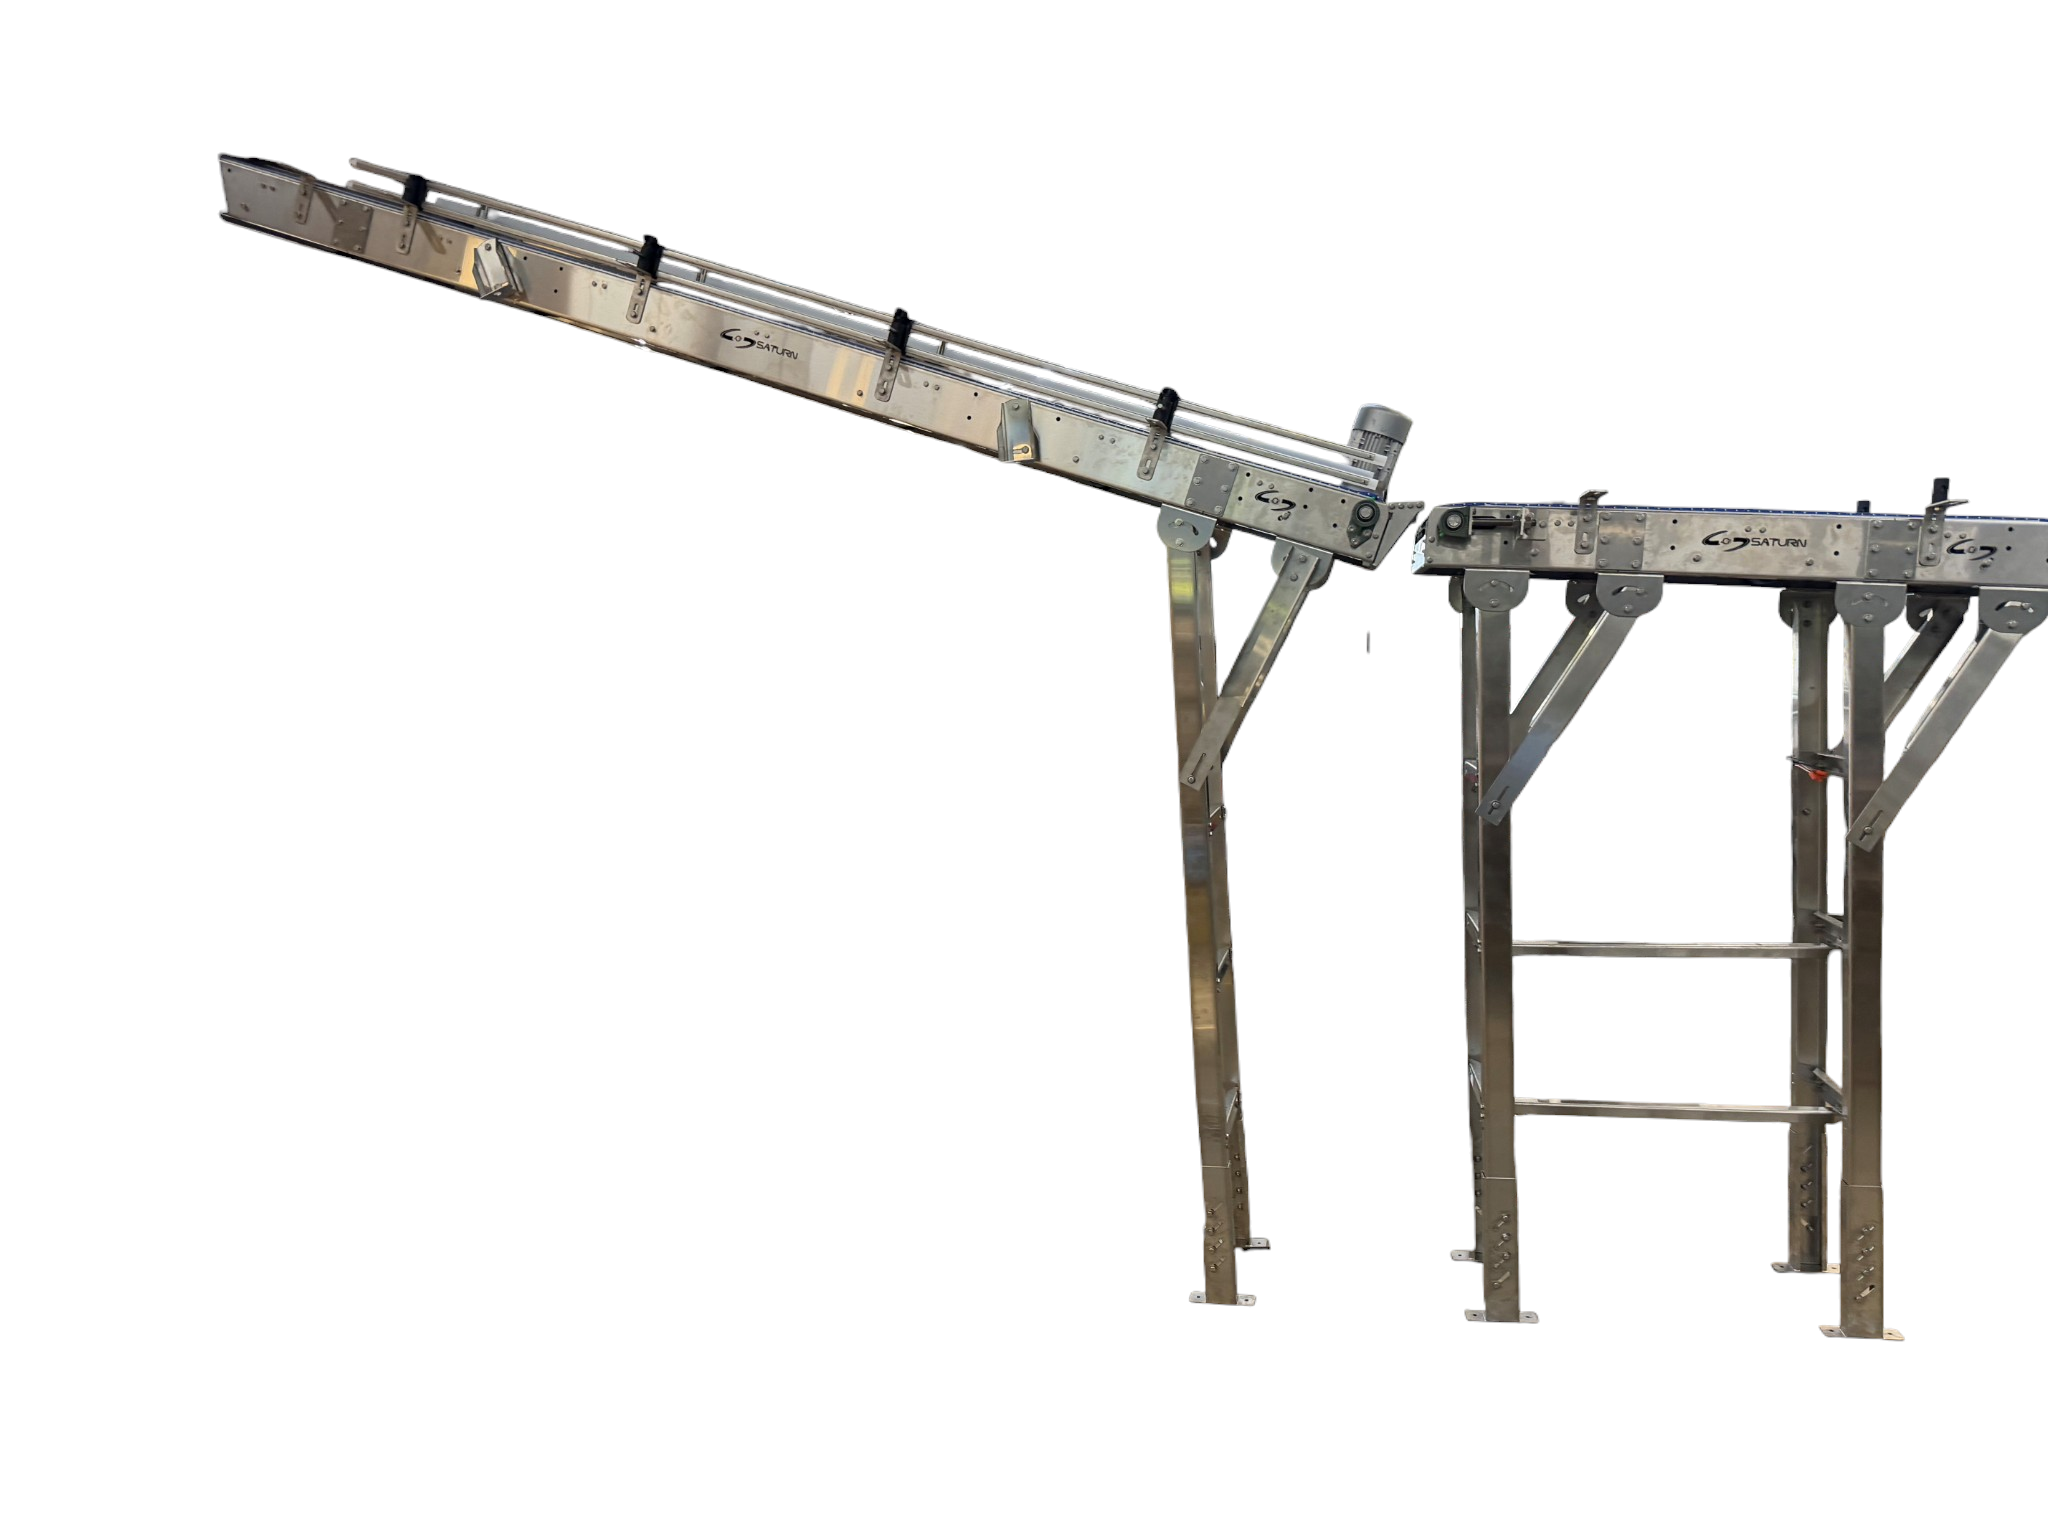
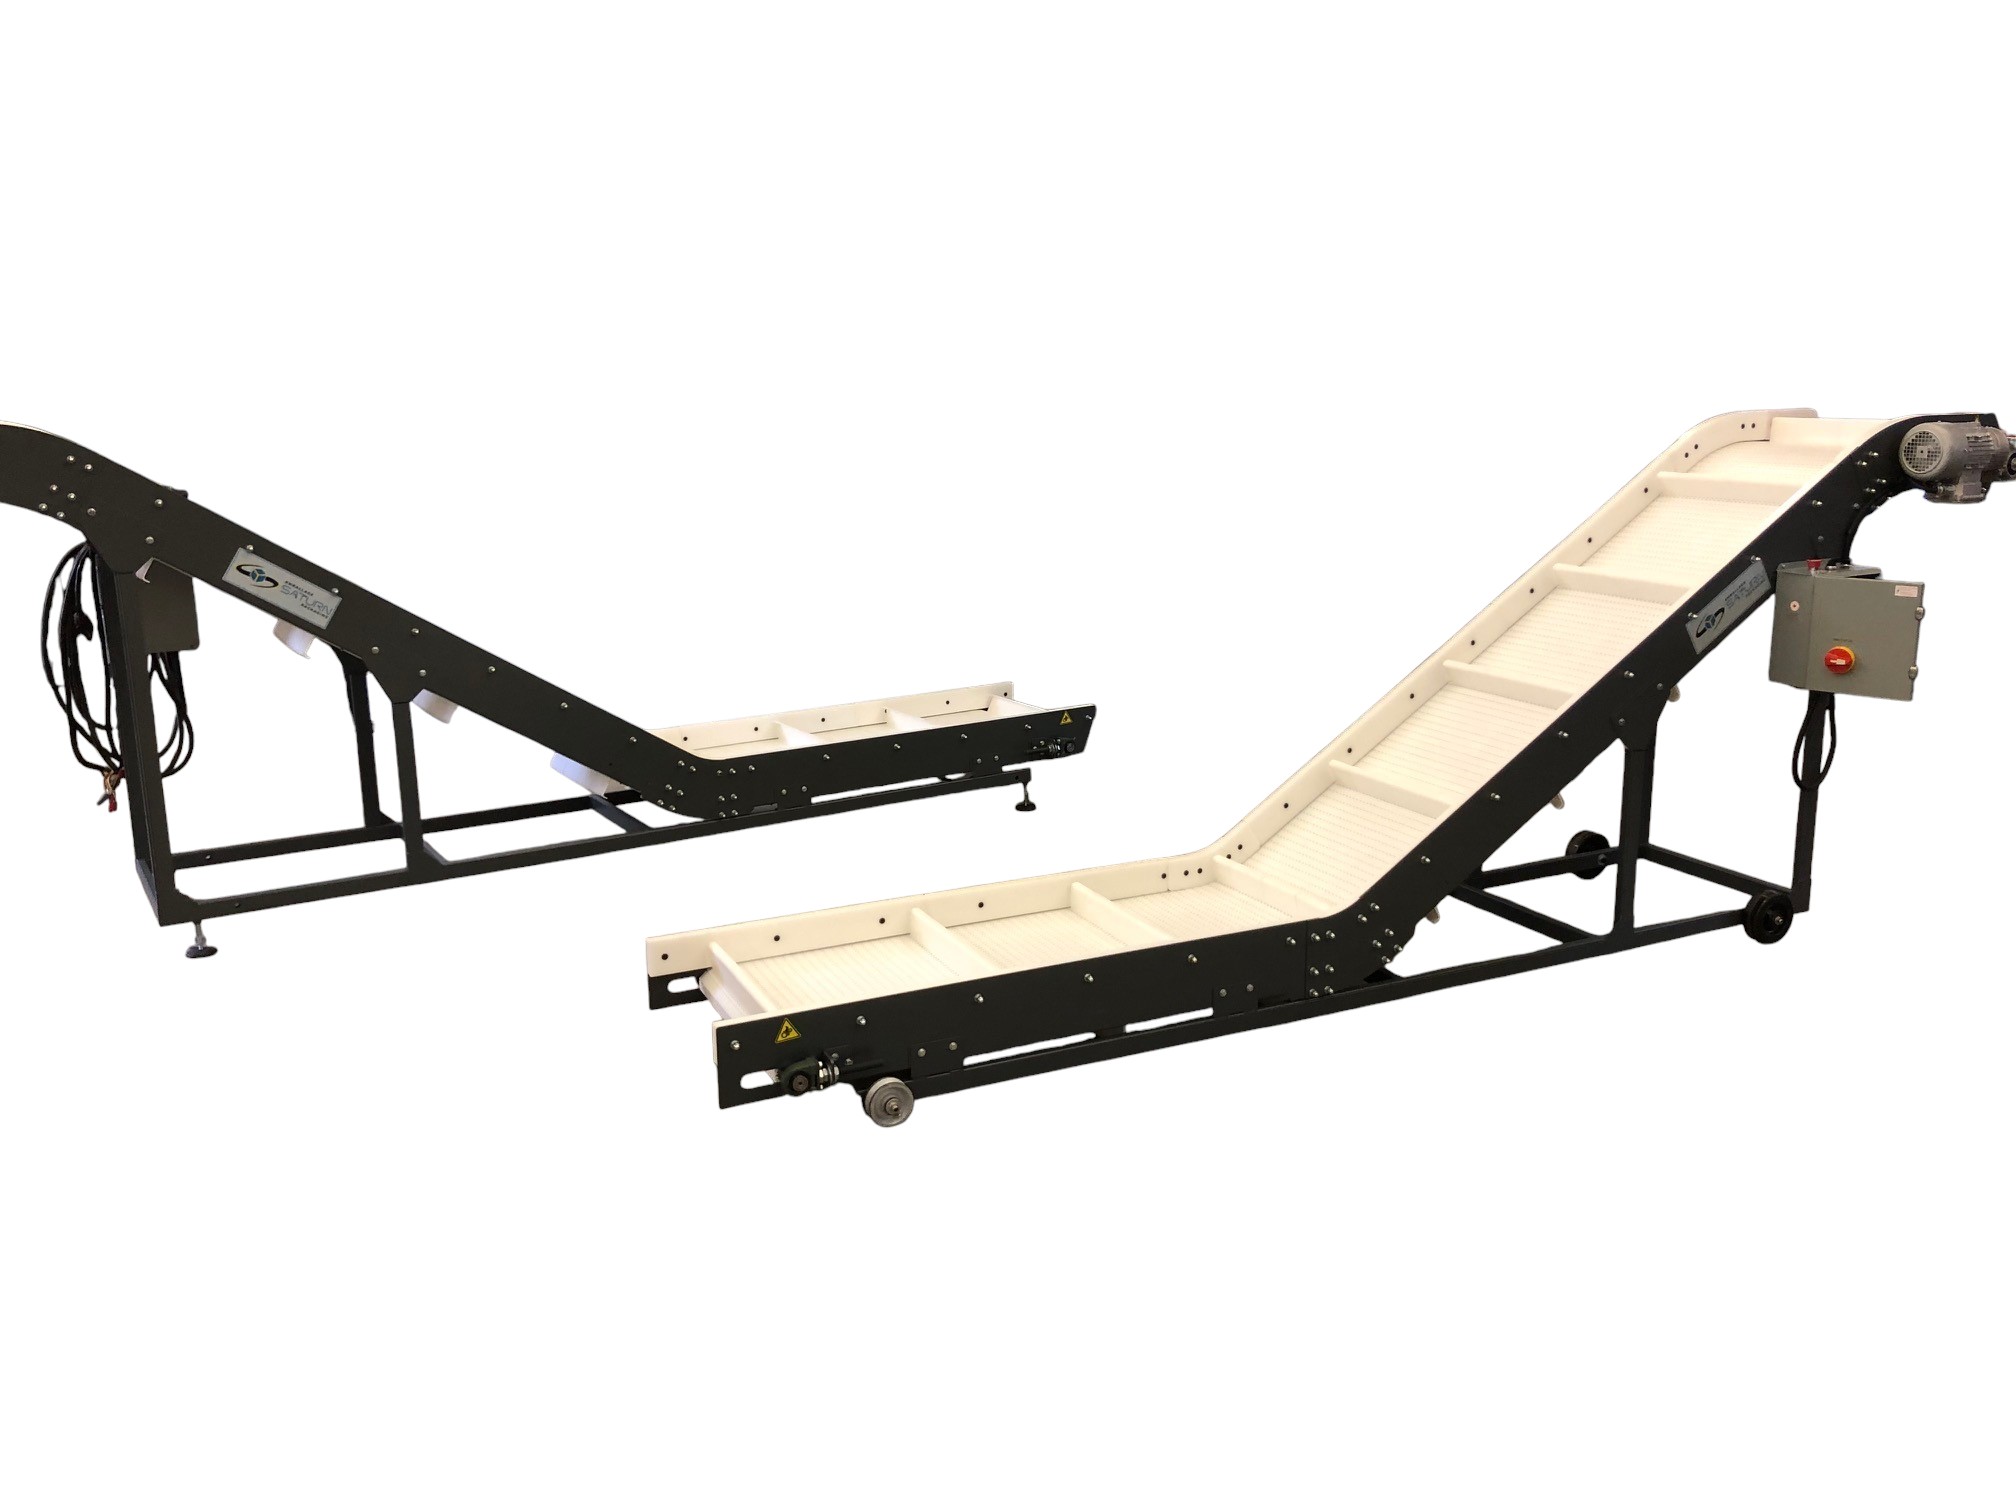
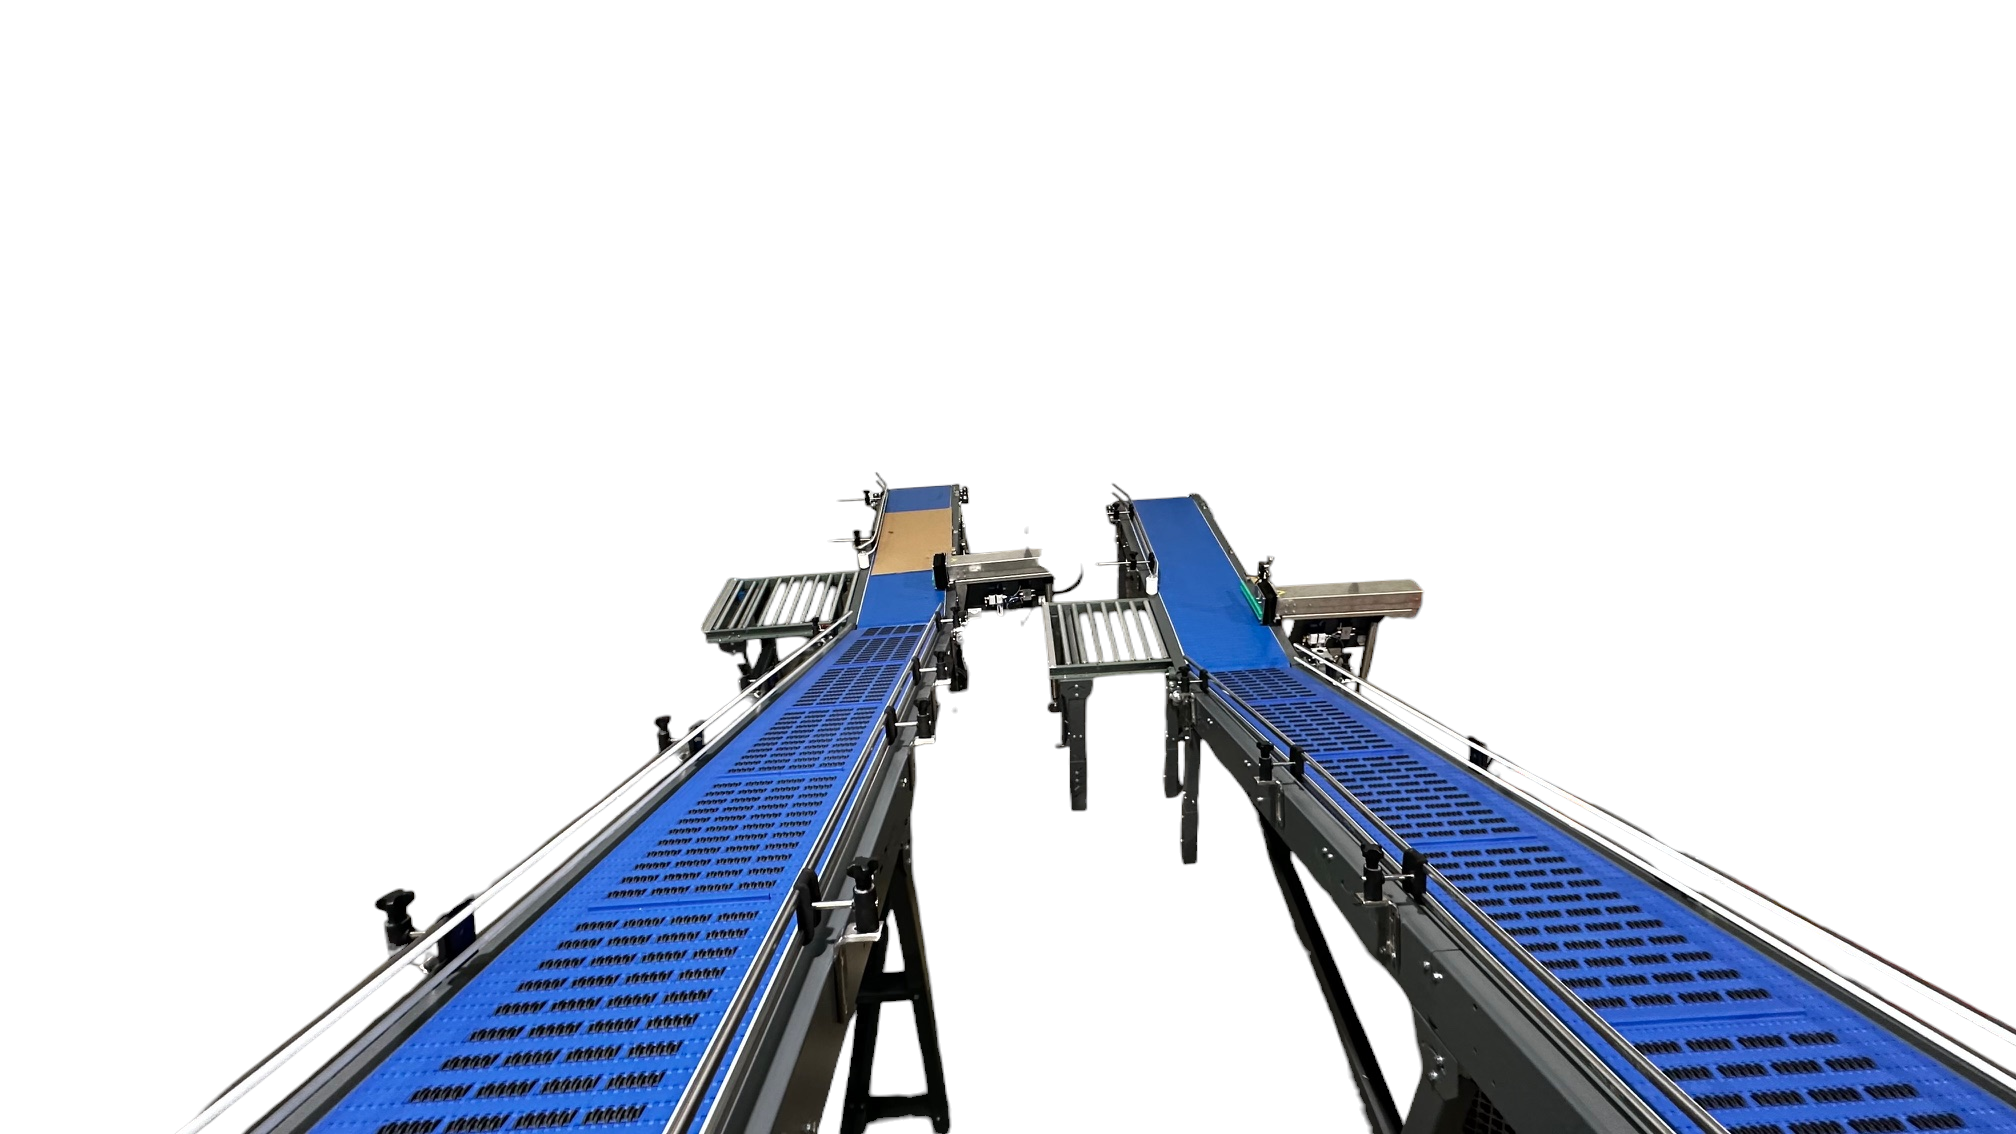
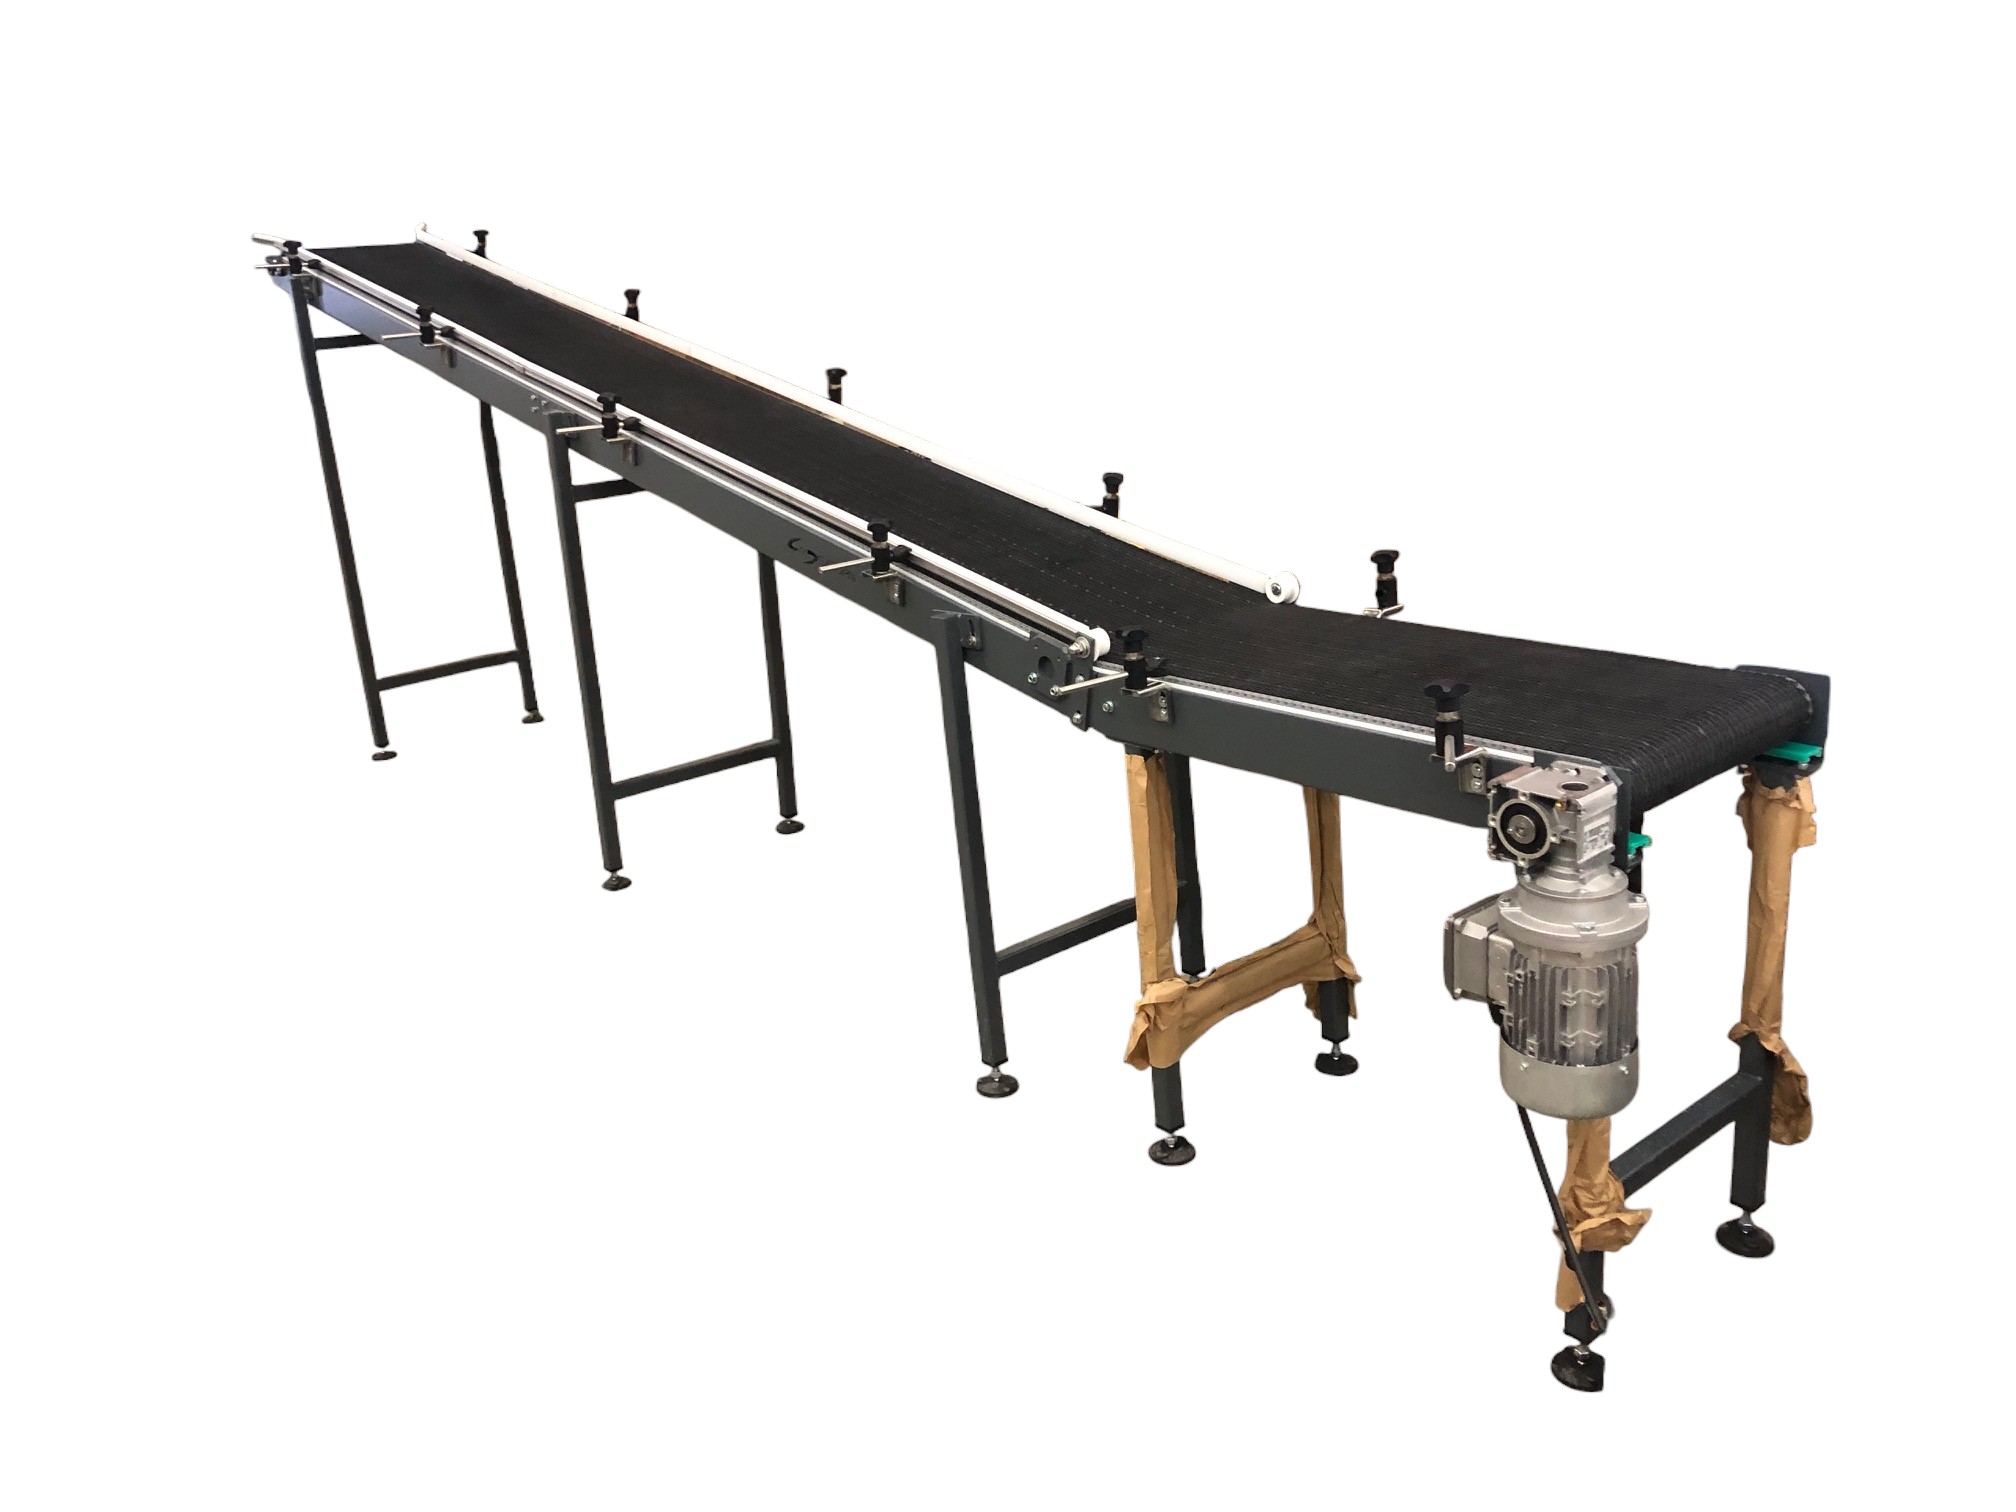
Saturn Incline / Decline Conveyors are custom-designed to transport products smoothly and efficiently between different elevations within production and packaging lines. Systems can be configured to elevate products to downstream equipment, lower products to another conveyor level, or overcome height differences within complex production layouts.
Conveyors are available with plastic modular belts or continuous PVC belts, with the belt technology selected according to the product, incline angle, production environment and required handling characteristics.
Modular belt configurations can incorporate high-grip surfaces and flights or cleats to provide additional product control on steeper inclines. Flights help positively carry products uphill, while high-grip belt surfaces increase friction and help minimize product slipping during elevation changes.
PVC belt configurations are available with high-grip surfaces for applications where increased friction is required without flights. Different belt surfaces can be selected according to the product and required incline or decline angle.
Incline and decline conveyors can handle a broad range of products, including boxes, cartons, cases, trays, bags, pouches, packaged foods, containers and individual products. Conveyor width, length, elevation and angle are engineered around the product and available plant layout.
Systems can incorporate horizontal infeed and discharge sections to provide smooth transitions between the inclined conveyor and adjacent equipment. Custom transition points and product guides can be designed to maintain product stability as it enters and exits the incline or decline.
Frame construction is available in painted steel or stainless steel. Painted steel provides a durable solution for general industrial and dry environments, while stainless steel is available for food, wet or corrosion-resistant applications.
Fixed or adjustable side guides can be incorporated to maintain product positioning throughout the elevation change. For products requiring additional containment, guide height and configuration can be customized according to the product.
Conveyors can operate at fixed or variable speeds and can be synchronized with upstream and downstream machinery. Sensors, product detection and PLC controls can also be incorporated when required for automated line operation.
Saturn Incline / Decline Conveyors can be supplied as standalone equipment or integrated with horizontal conveyors, packaging machines, accumulation systems, elevators, inspection equipment and complete turnkey production lines.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad