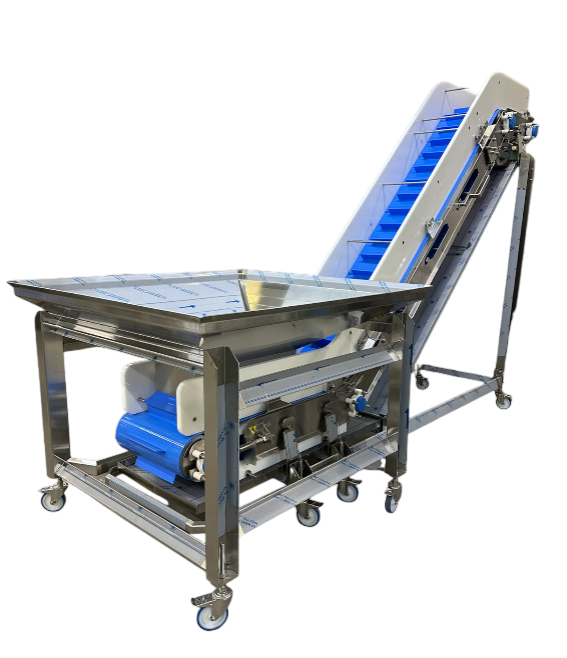
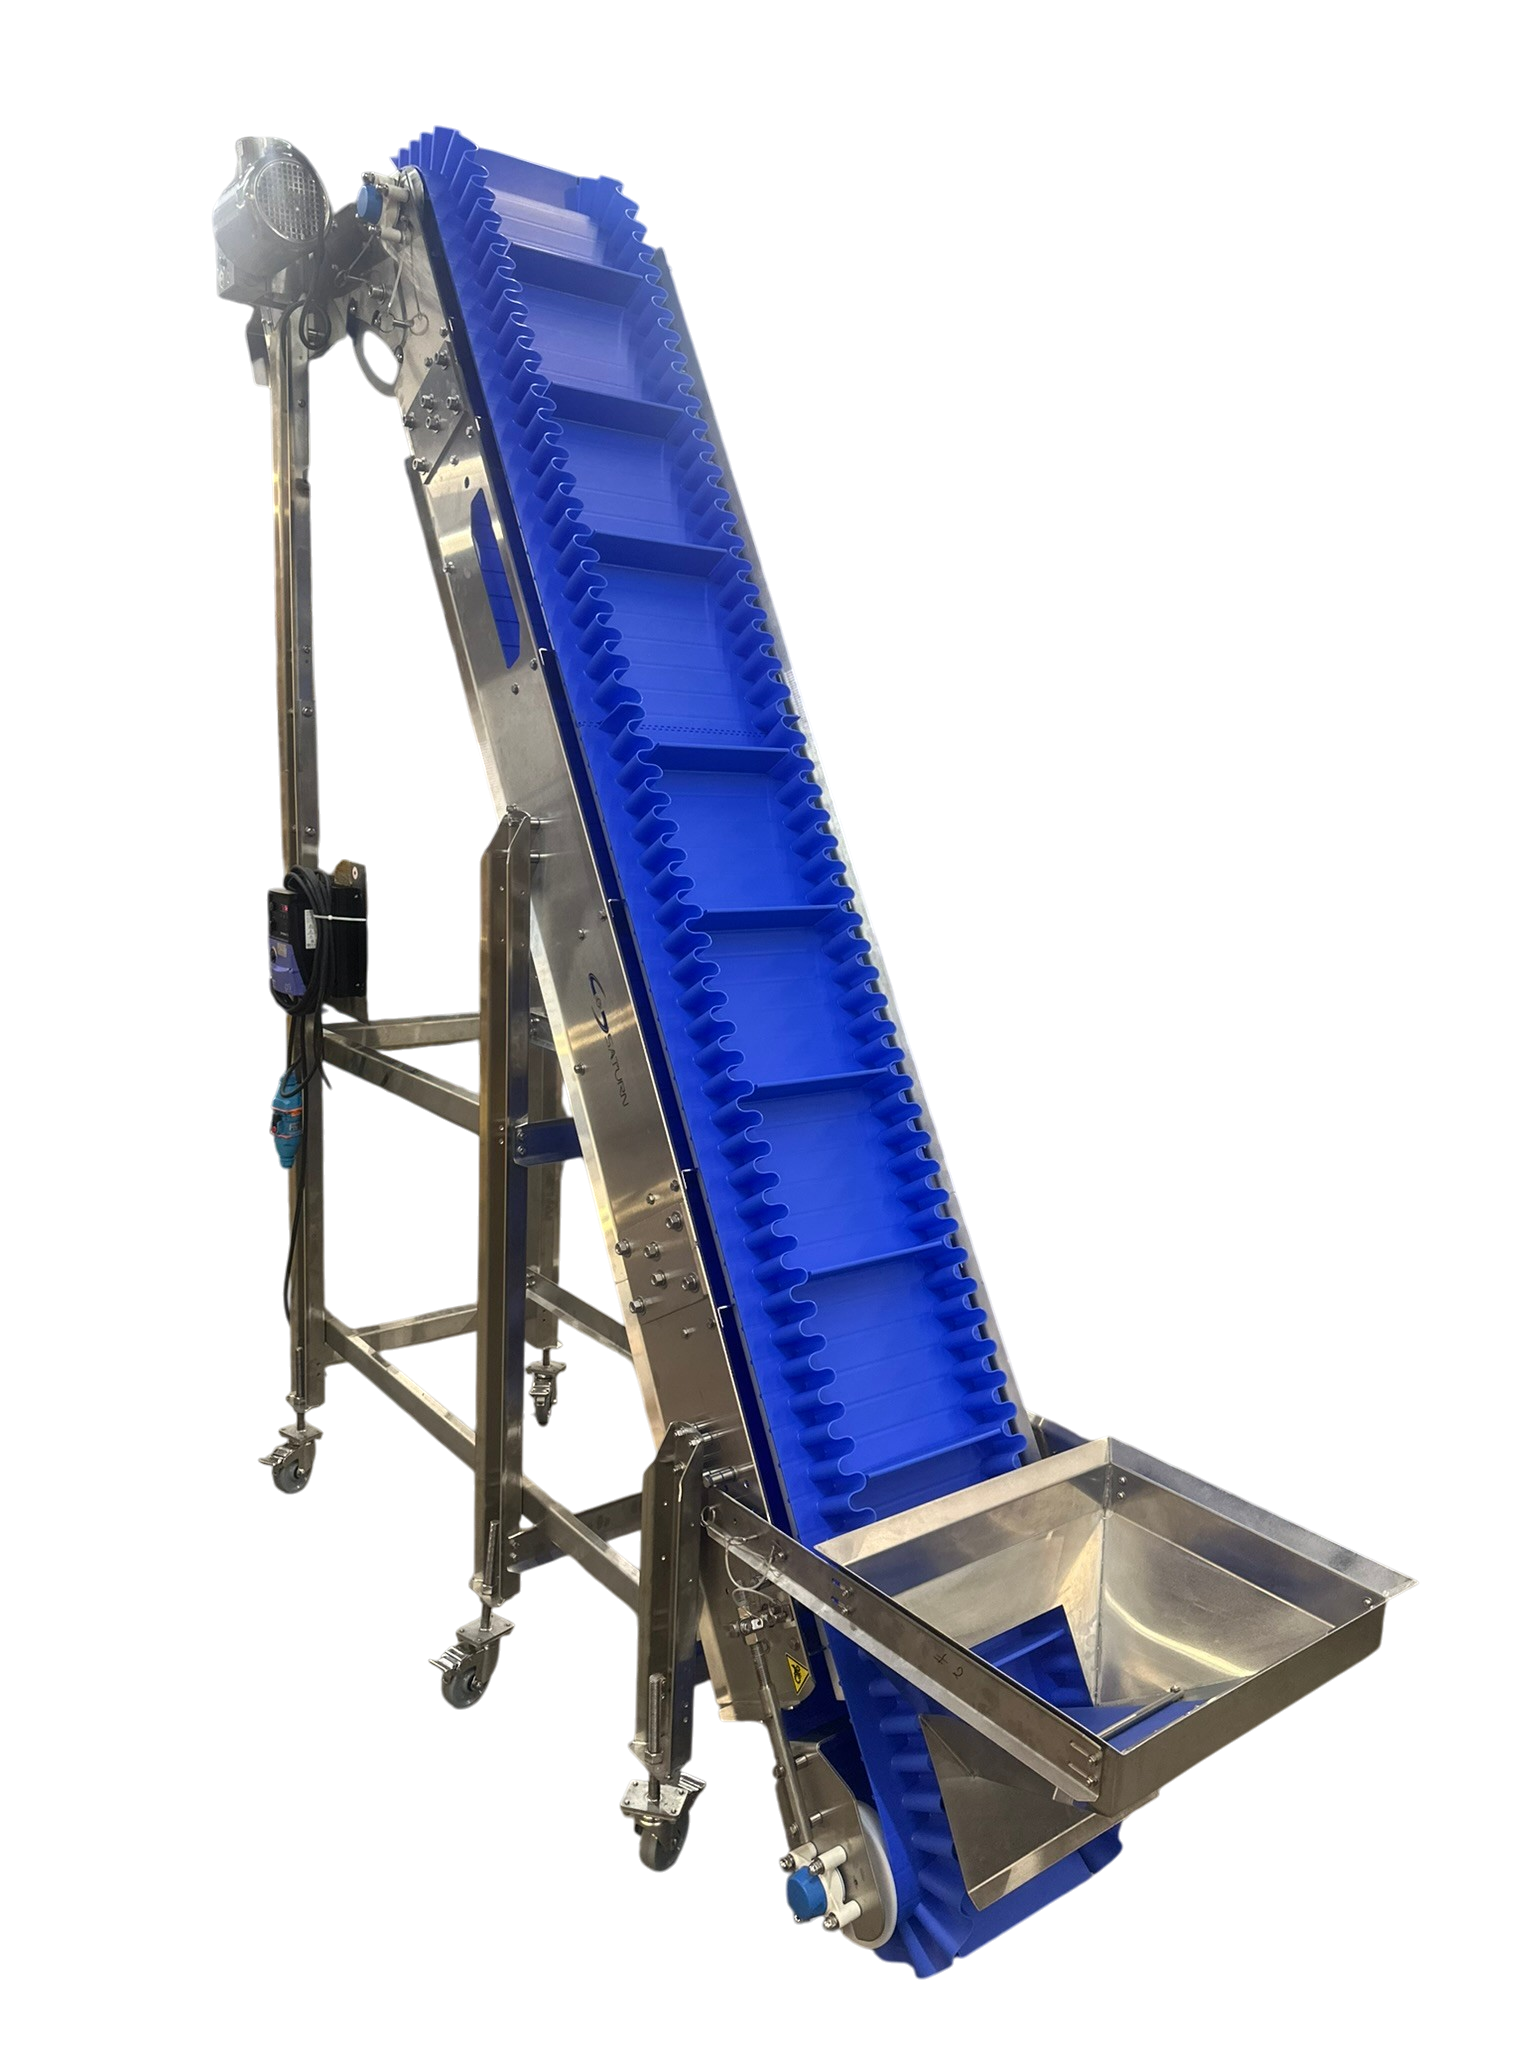
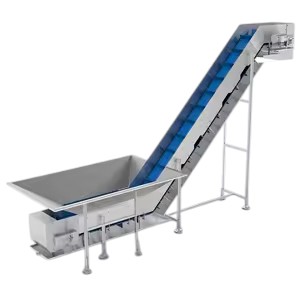
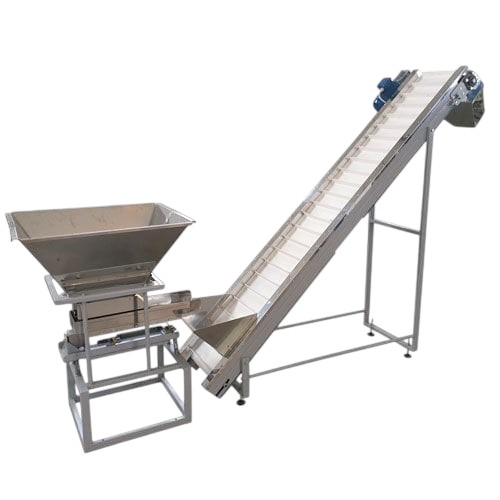
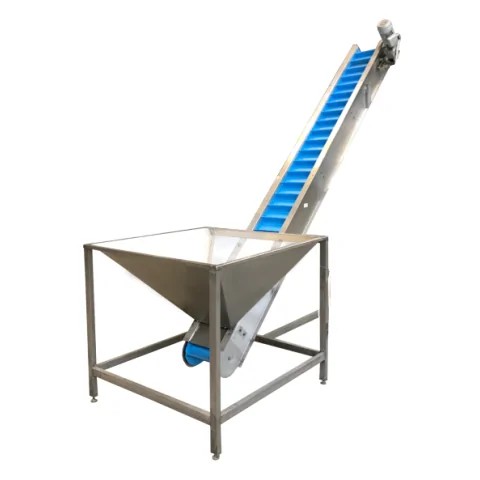
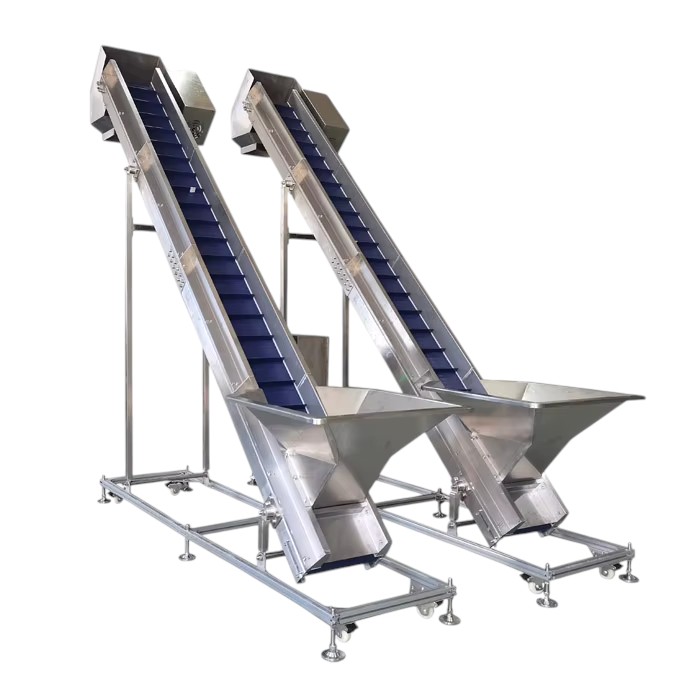
Saturn Bulk / Hopper Incline Conveyors are designed to receive, buffer and elevate loose or bulk products to downstream processing and packaging equipment. The combination of an infeed hopper and inclined conveyor provides controlled product transfer while reducing manual handling and maintaining a consistent supply of product to the next machine.
Products are loaded directly into the bulk hopper, which provides temporary storage and helps accommodate variations in upstream product supply. The product is then progressively picked up by the conveyor and elevated to the required discharge height. Hopper dimensions and capacity can be customized according to the product, required buffer capacity and available floor space.
Incline conveyors can be equipped with cleats or flights to create individual product pockets and prevent products from sliding backward during elevation. Cleat height, spacing and belt configuration can be selected according to product size, flow characteristics, required capacity and incline angle. Cleated belts are commonly used for feeding bulk products to elevated packaging and processing equipment because they provide more controlled transport than conventional flat belts on steeper inclines.
Systems can handle a wide range of products including powders, granules, grains, nuts, snacks, confectionery, frozen foods, vegetables, ingredients, small parts and other loose products.
Multiple conveyor technologies can be provided depending on the application, including PVC/PU cleated belts, food-grade belts and plastic modular belts. Sidewalls, skirts or high side guides can be incorporated to help contain loose products and minimize product loss during loading and elevation.
For food applications, conveyors can be supplied with stainless steel construction and food-grade belt materials. Sanitary configurations can also be engineered where increased accessibility and washdown capability are required.
Bulk / Hopper Incline Conveyors are commonly used to automatically feed multi-head weighers, volumetric fillers, pouch baggers, VFFS machines, sorting systems, processing equipment and other elevated machinery.
Variable-speed operation allows the product feed rate to be coordinated with downstream demand. Product sensors, hopper level sensors and PLC controls can also be incorporated to automatically start, stop or regulate the conveyor according to production requirements.
Saturn Bulk / Hopper Incline Conveyors can be supplied as standalone equipment or integrated with dumpers, feeders, weighing systems, baggers, packaging machines and complete turnkey production lines.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad