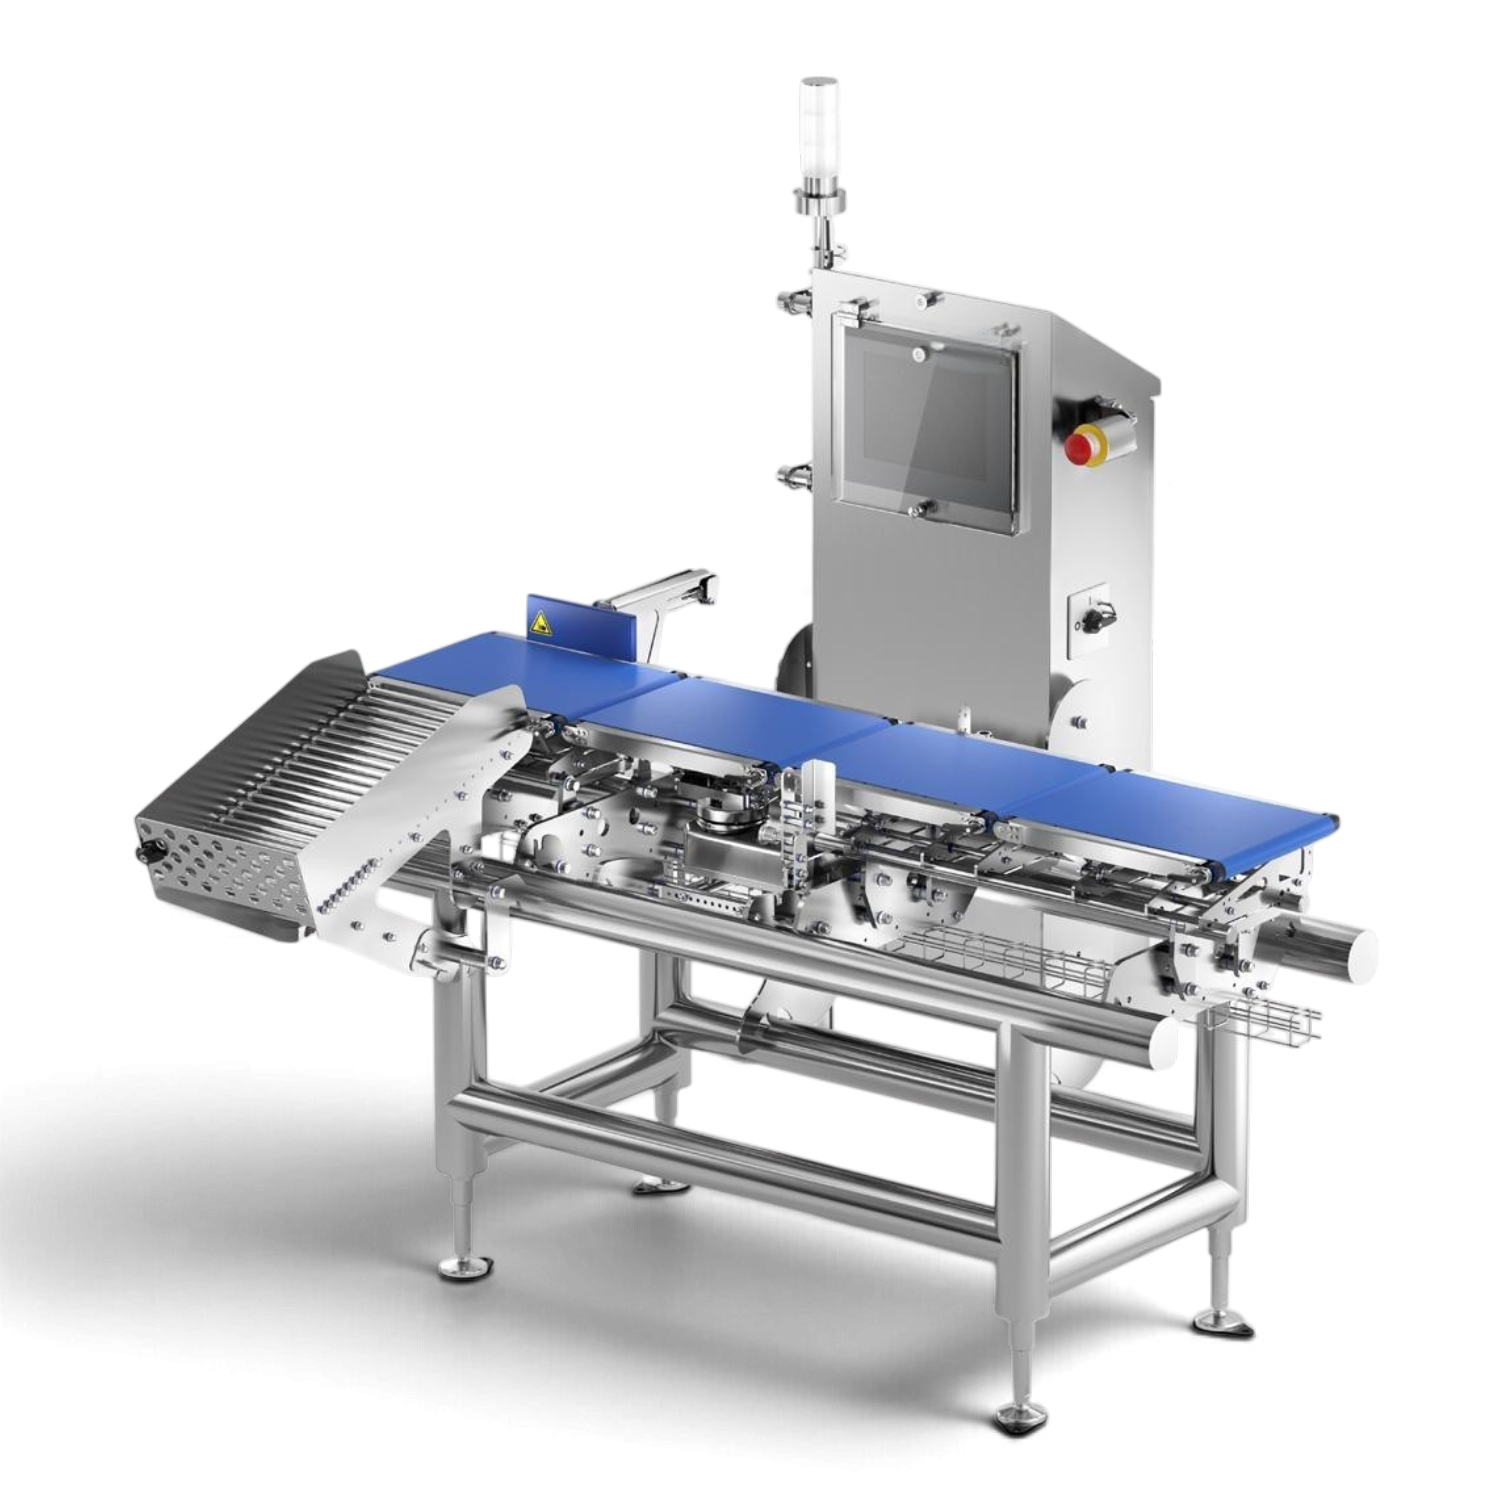
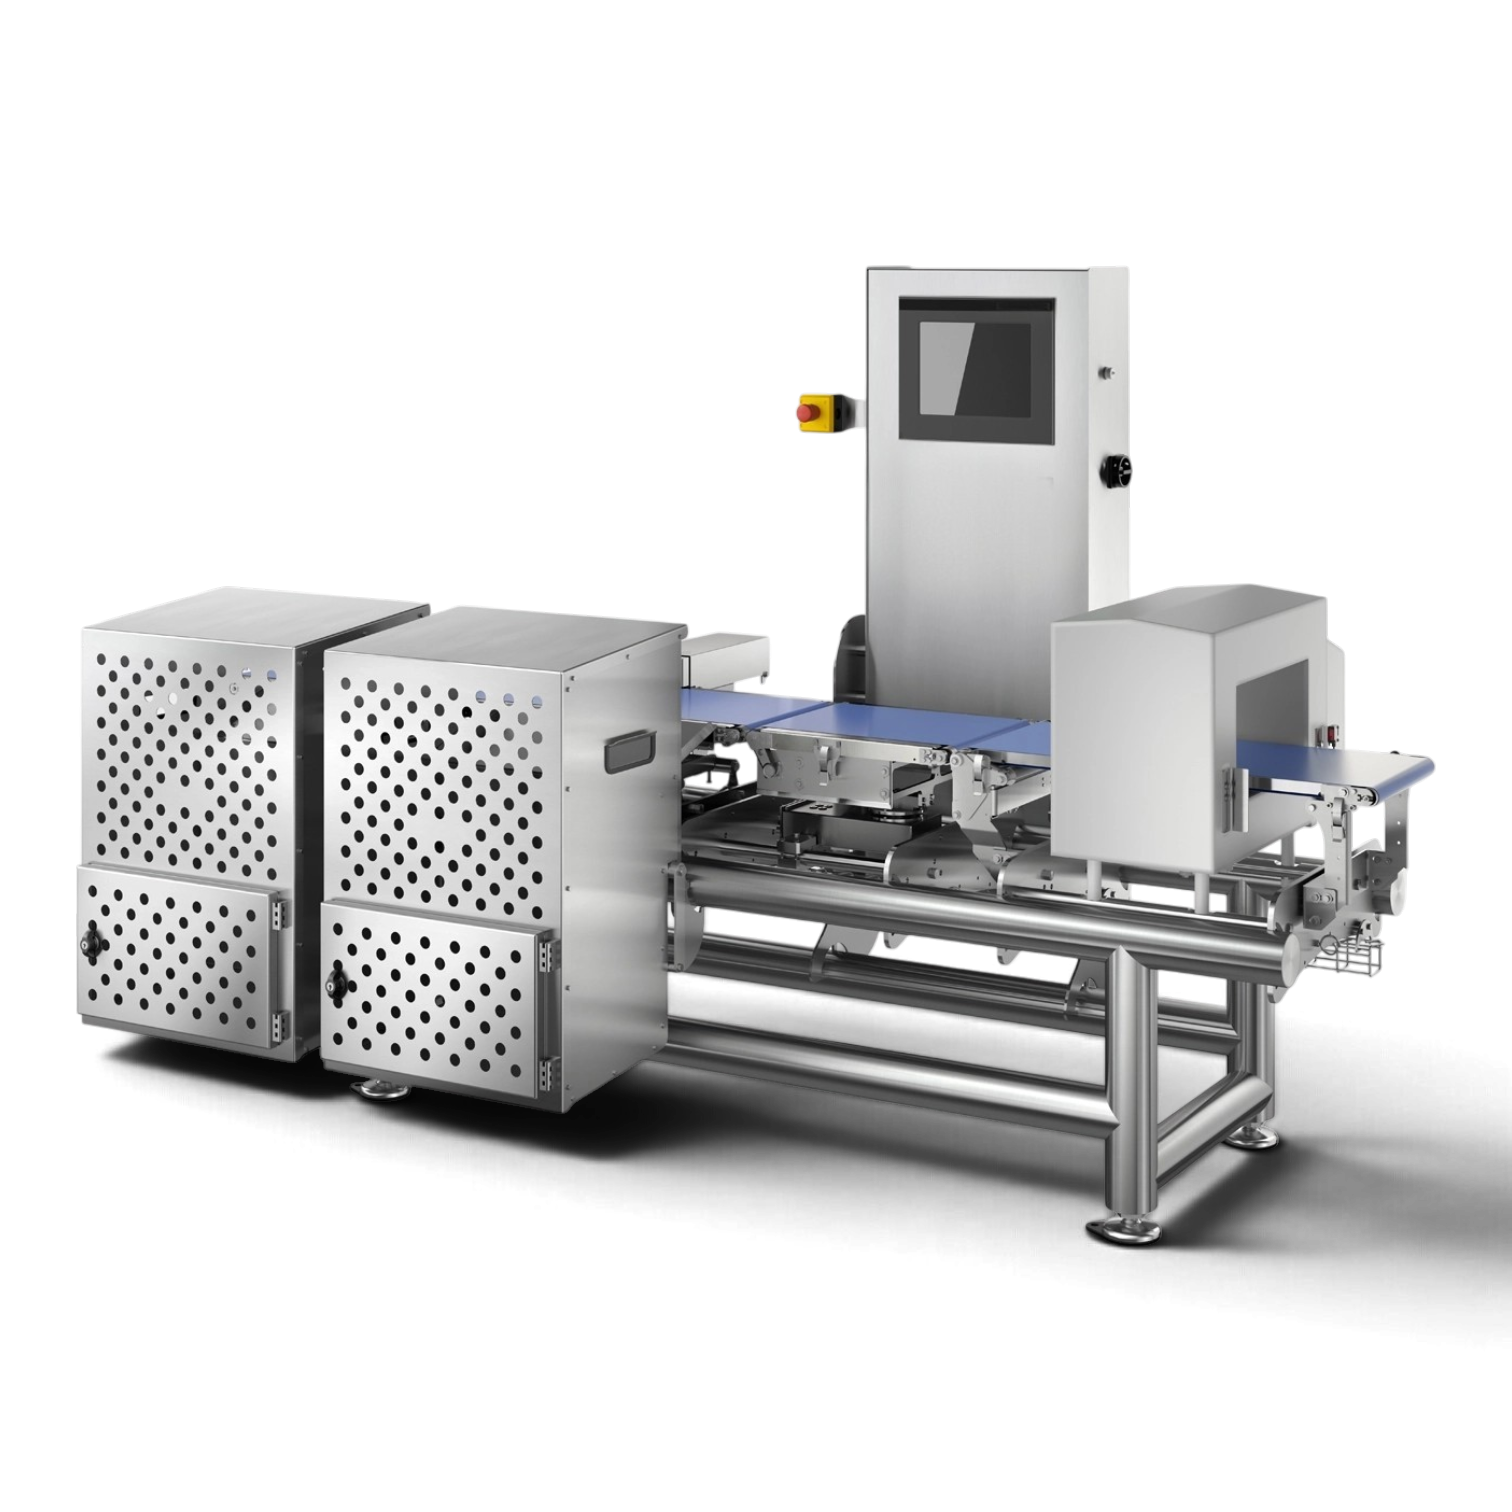
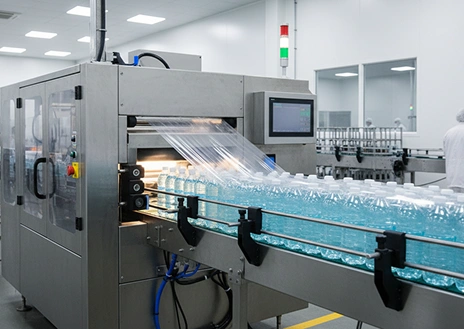
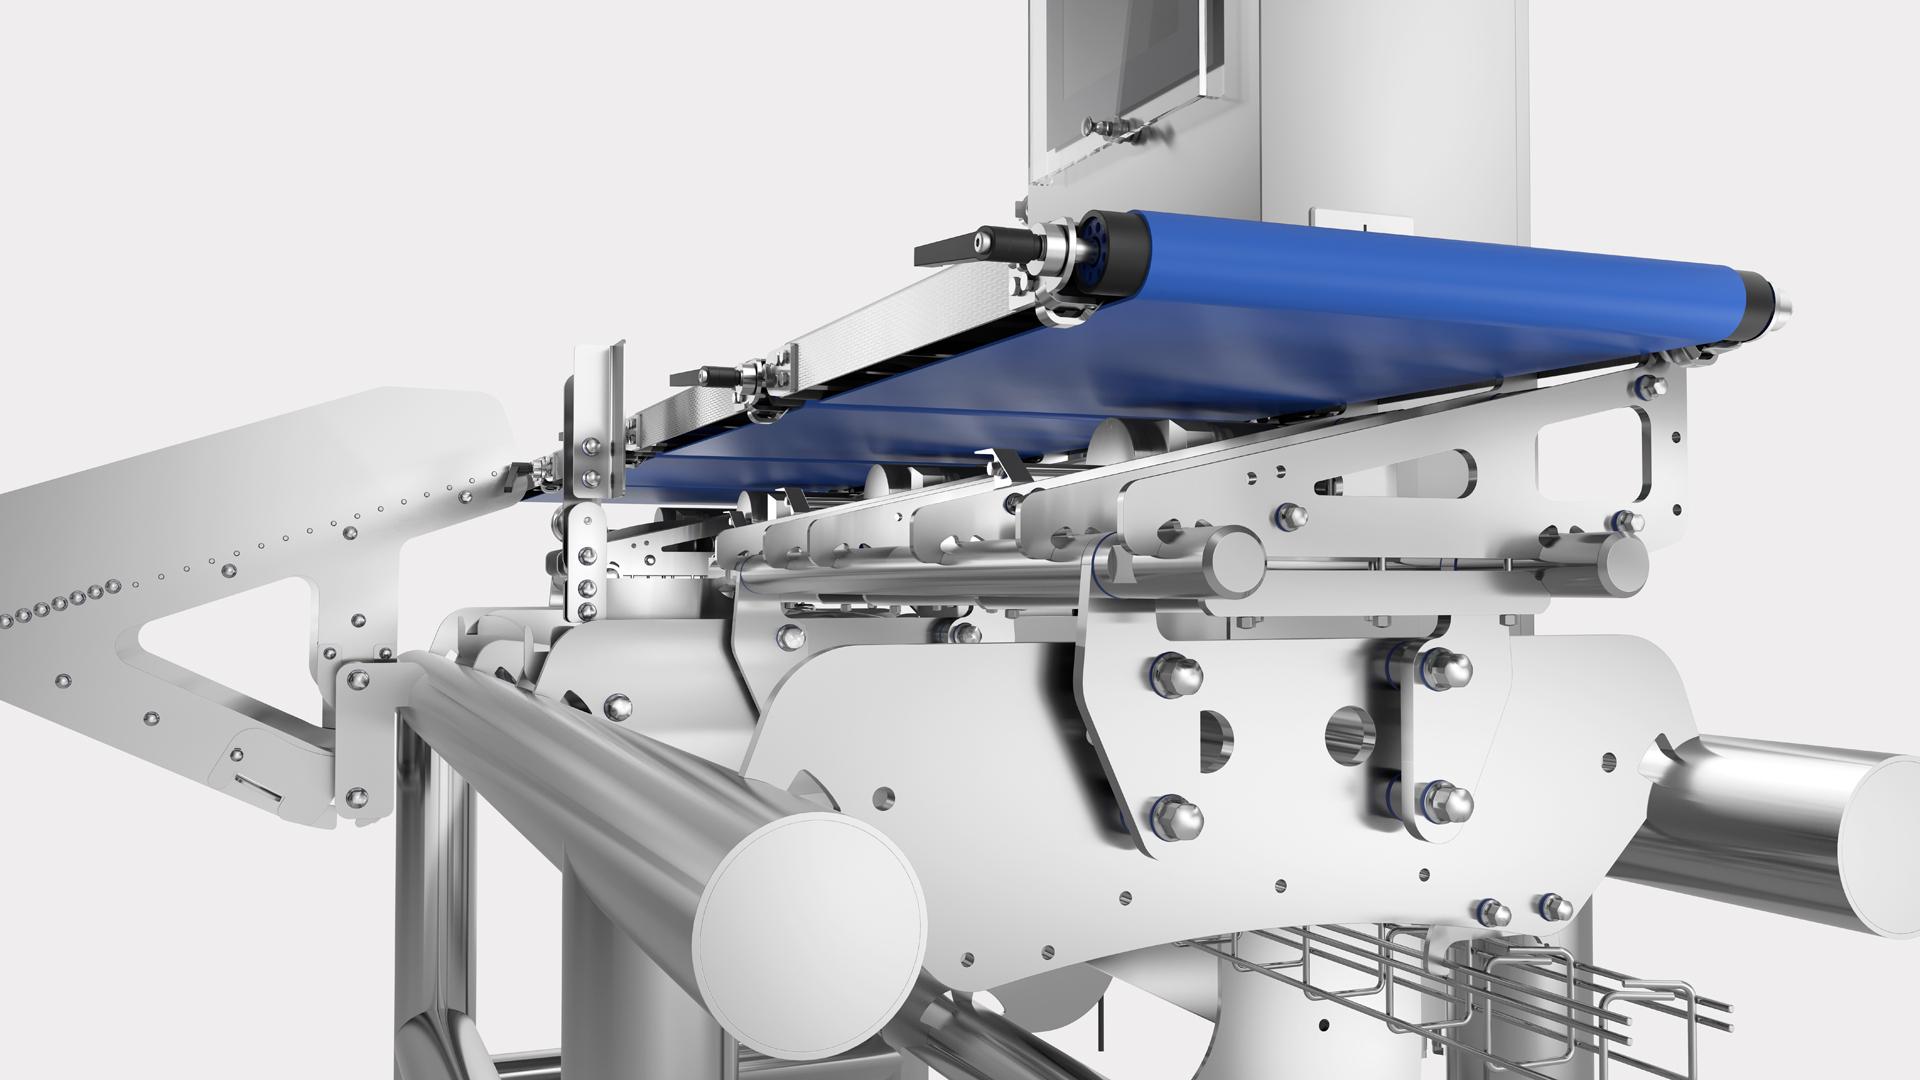
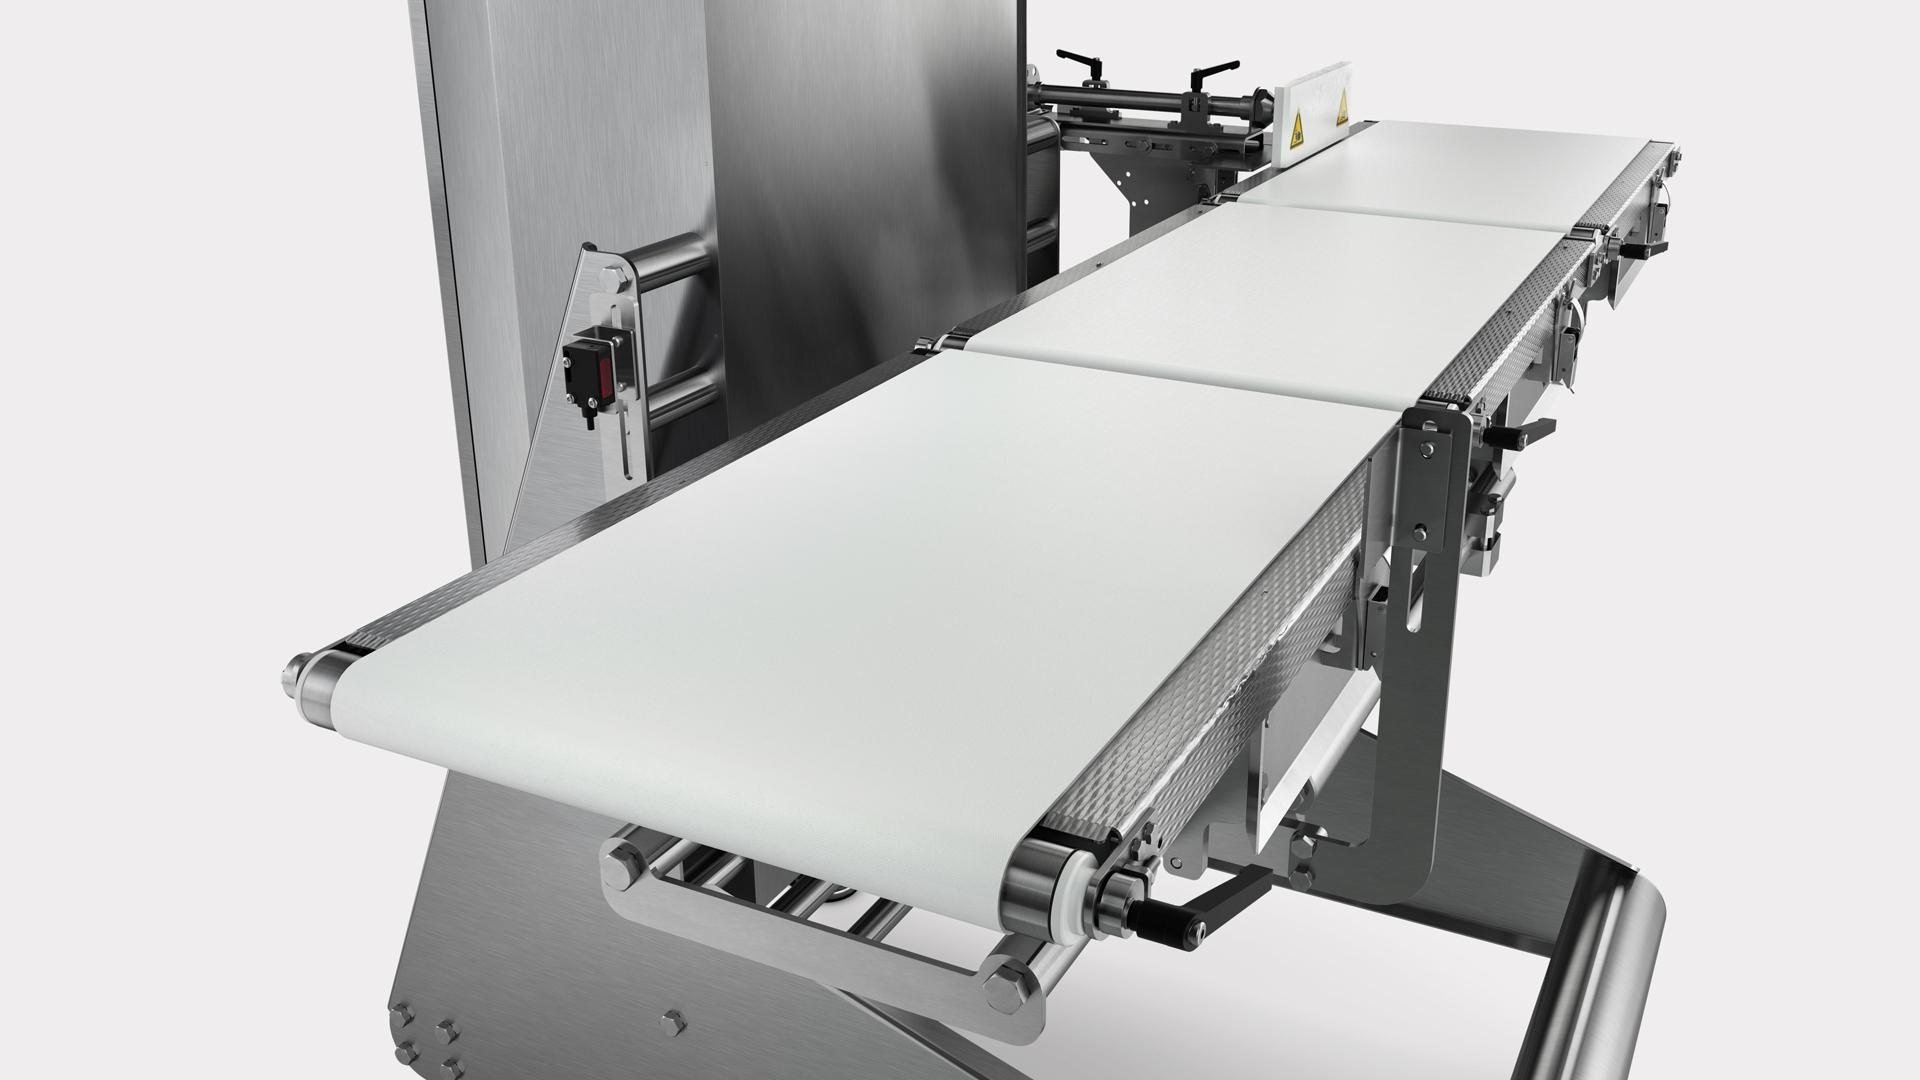
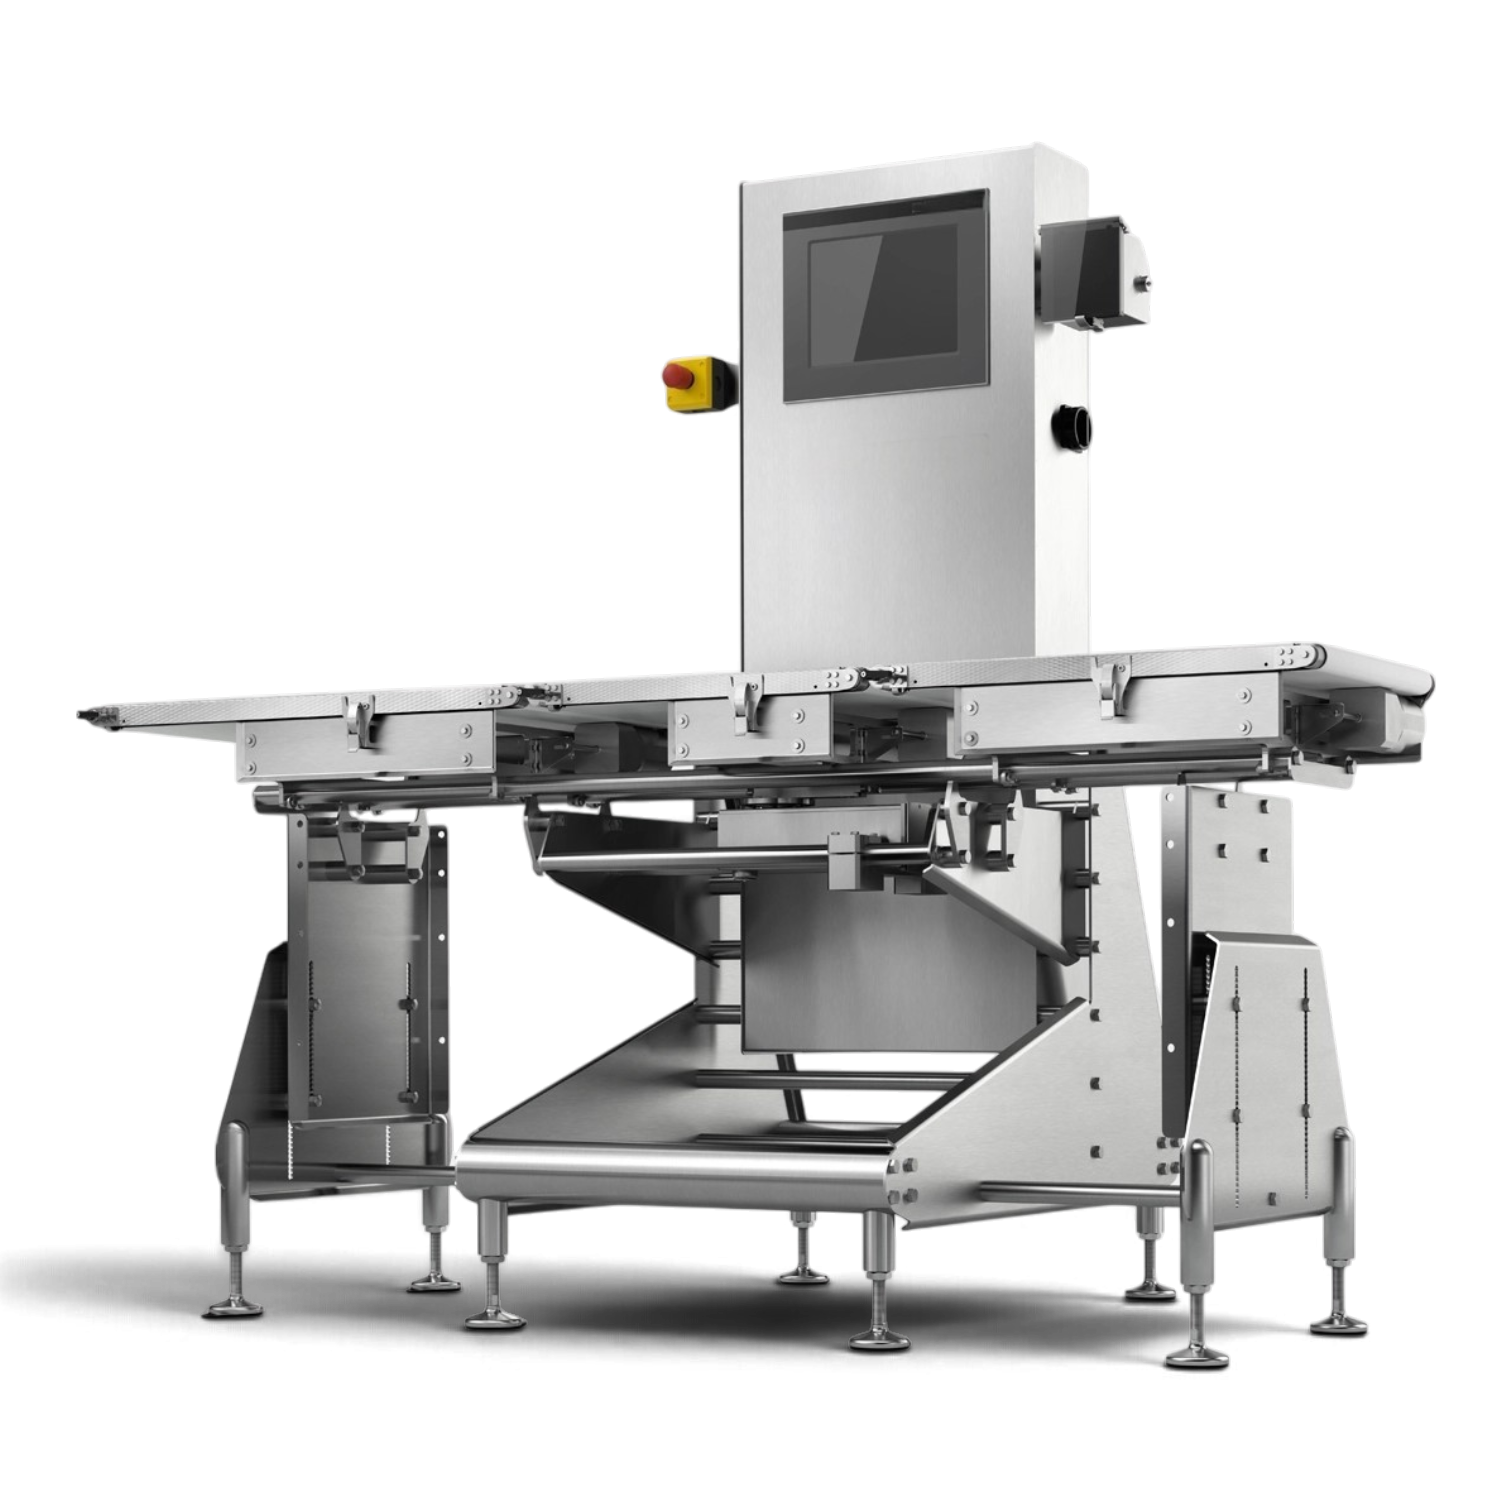
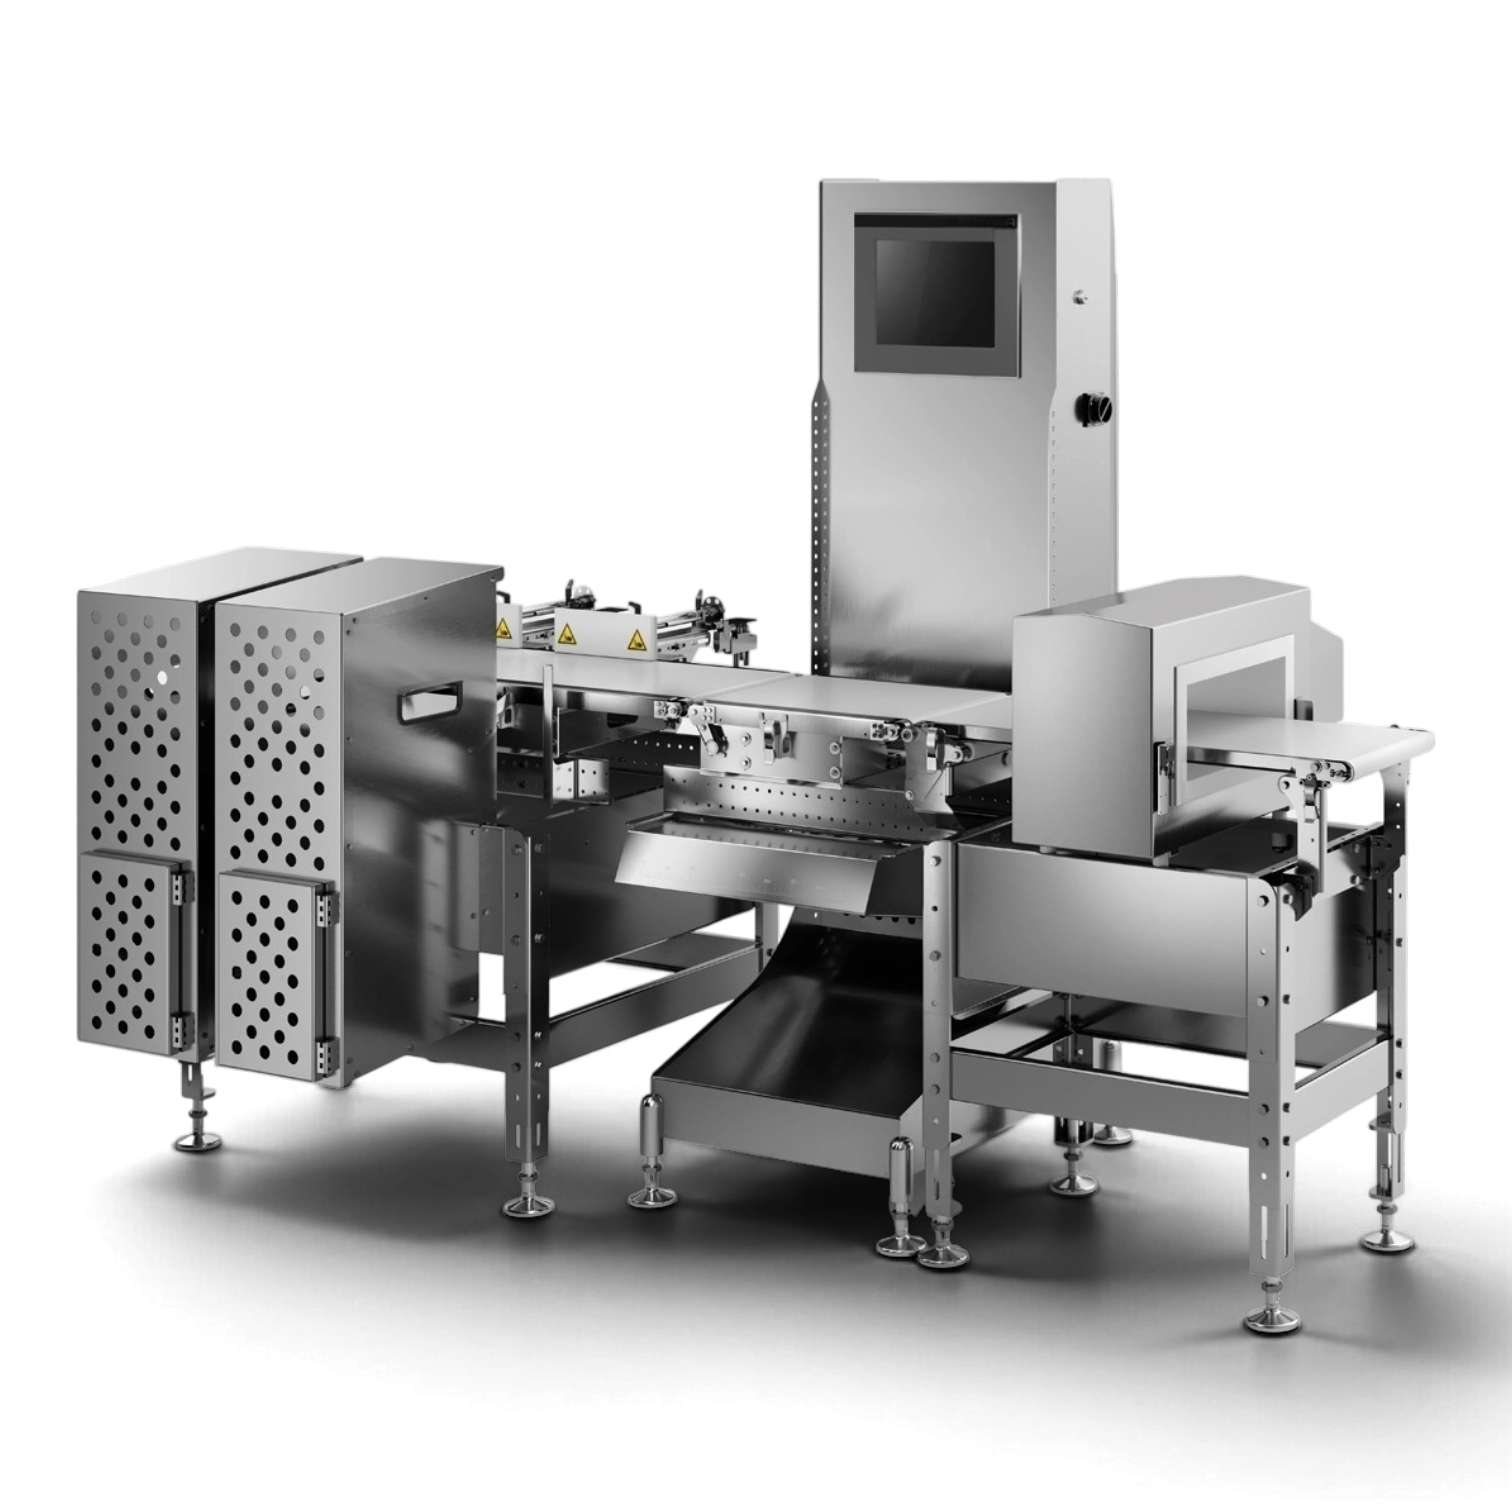
Our Automatic Checkweigher Systems provide continuous, in-motion weight verification for a wide range of food, beverage, pharmaceutical and industrial products. Every product is automatically weighed as it travels through the system, allowing 100% weight control without stopping production. Dynamic checkweighing helps identify underweight and overweight products while maintaining production throughput.
A wide range of models, conveyor dimensions and weighing capacities can accommodate products such as trays, cups, bowls, flow packs, pouches, sachets, bottles, cans, jars, boxes, cartons and other packaged or unpackaged products. Systems can be configured for both lower-speed precision applications and high-speed production lines, depending on product size, weight and accuracy requirements. Bizerba, for example, offers configurations reaching up to 600 products per minute for certain product sizes and weights.
Products outside the programmed weight tolerances can be automatically removed using a product-specific reject system. Depending on the application, reject methods can include air blast, pusher, flap, drop/lift systems, dividers and other mechanisms, allowing the handling system to be matched to the product, package and production speed.
Checkweighers provide more than simple pass/fail weight inspection. Production data can be collected and analyzed to monitor weight trends, identify filling inconsistencies and help reduce unnecessary product giveaway caused by overfilling. Real-time weight information can also be used to support upstream process adjustments and improve overall production consistency.
For food and washdown environments, systems can be supplied with stainless steel hygienic construction, open-frame designs and easy-access or quick-removal conveyor components to simplify sanitation. Depending on the selected model and application, IP65 and IP69 configurations can also be available for demanding cleaning environments.
Checkweighers can also be combined with integrated metal detection, providing weight control and contaminant inspection within a compact system. They can operate as standalone inspection machines or be fully integrated with conveyors, reject verification, upstream packaging equipment and complete production lines.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad