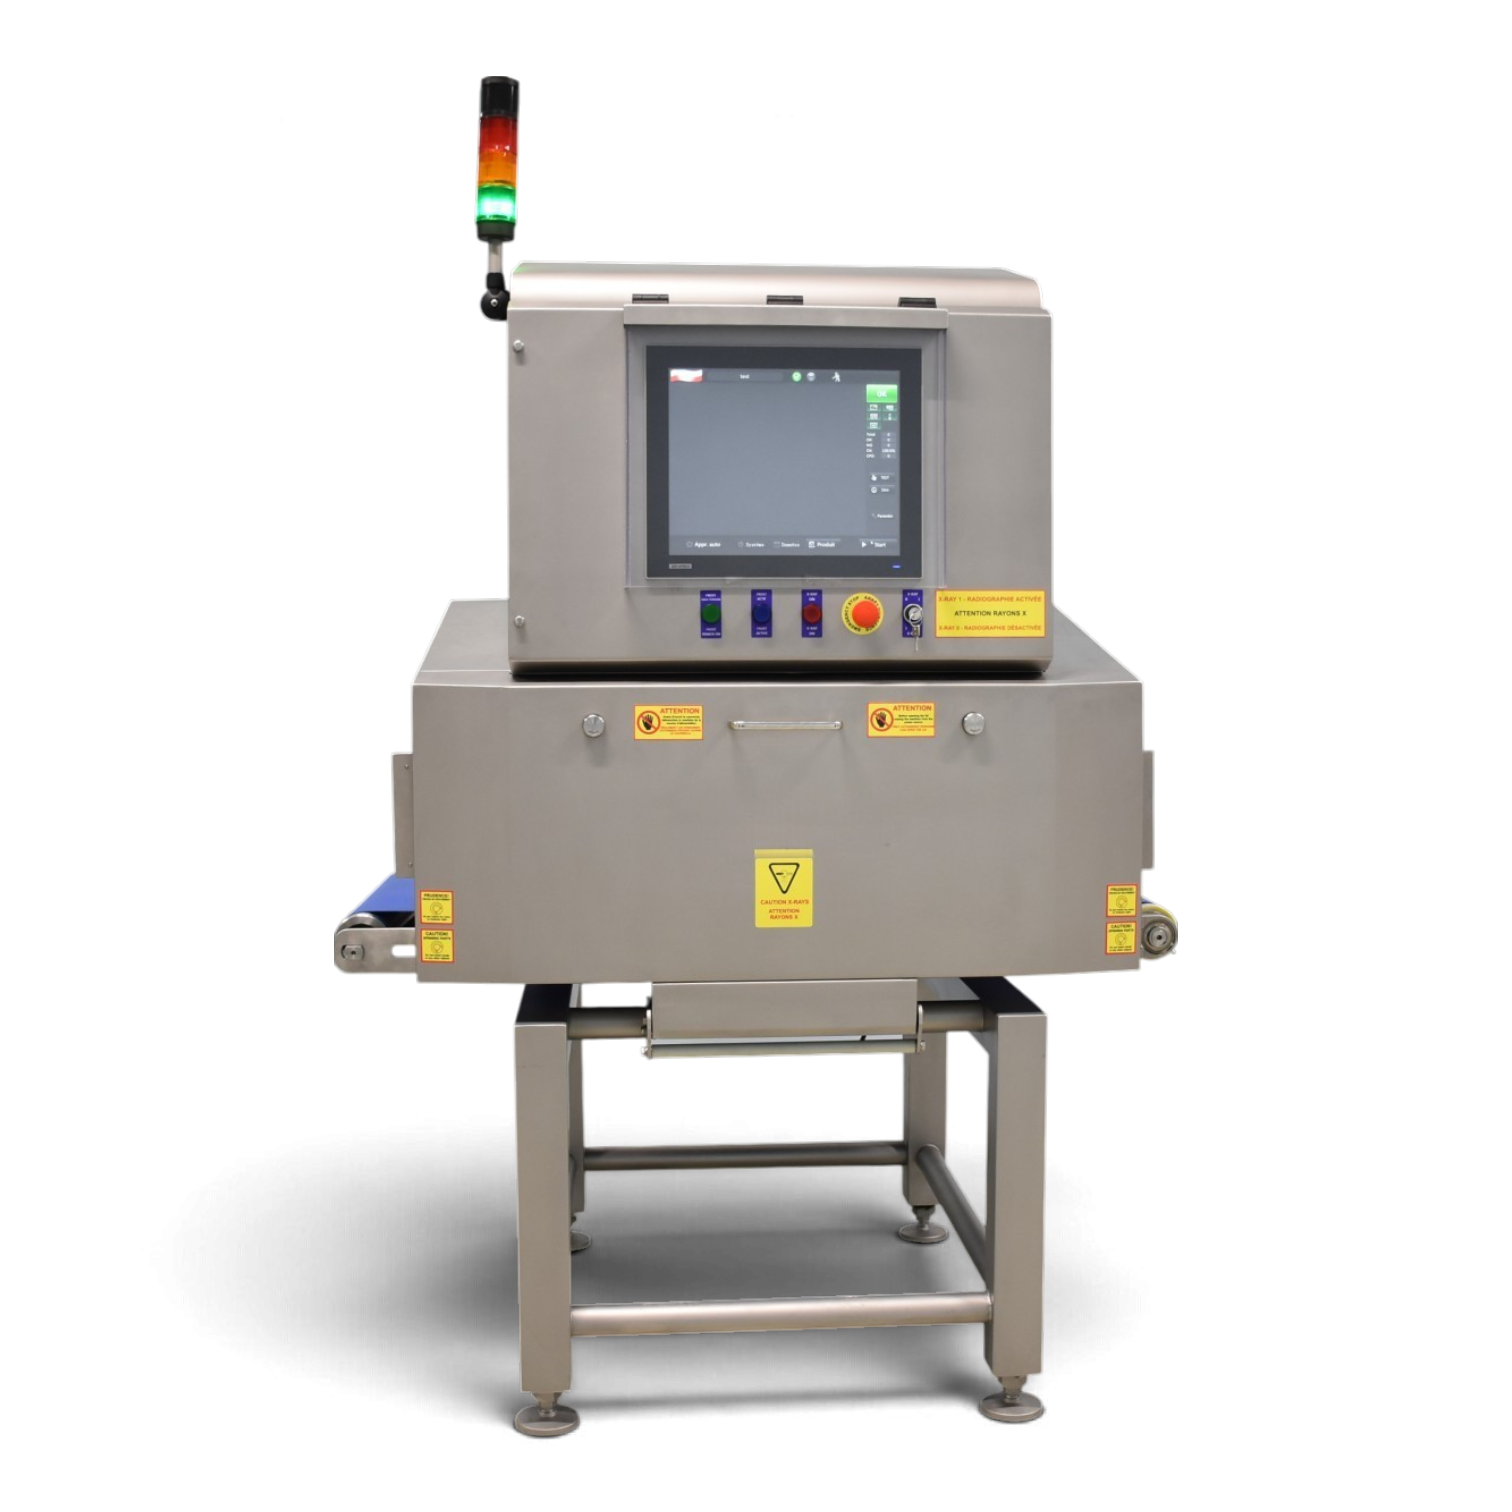
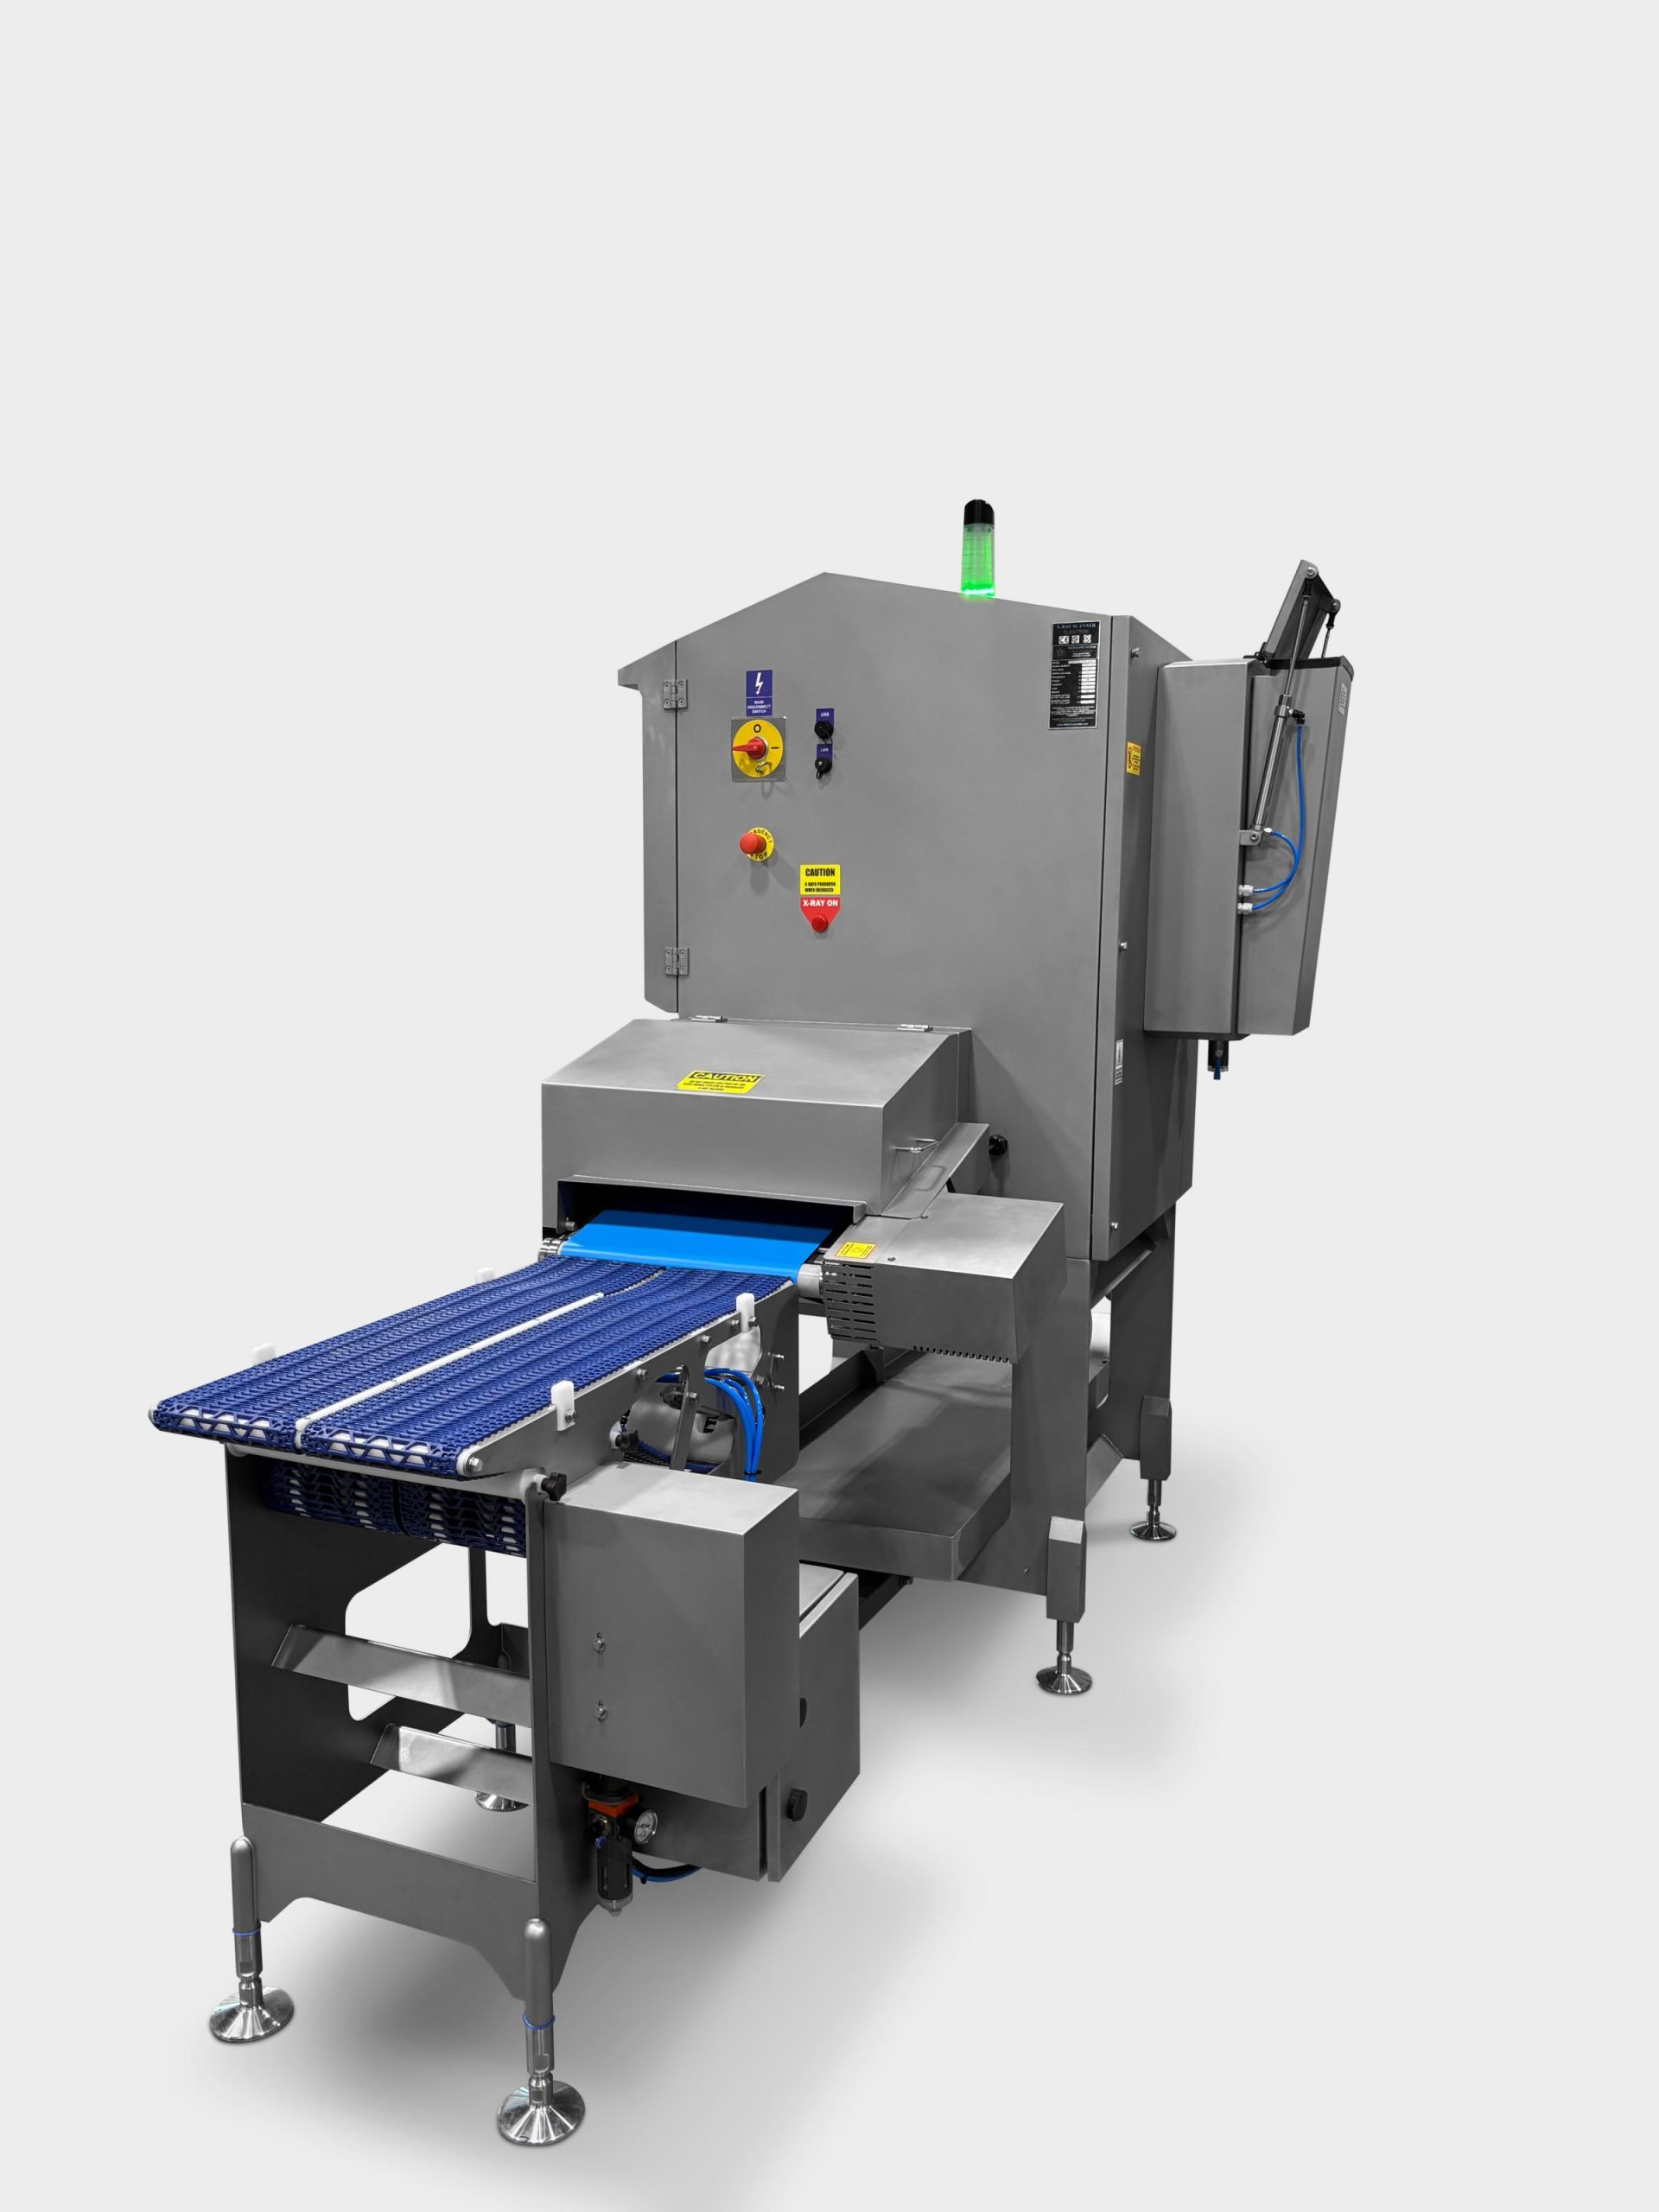
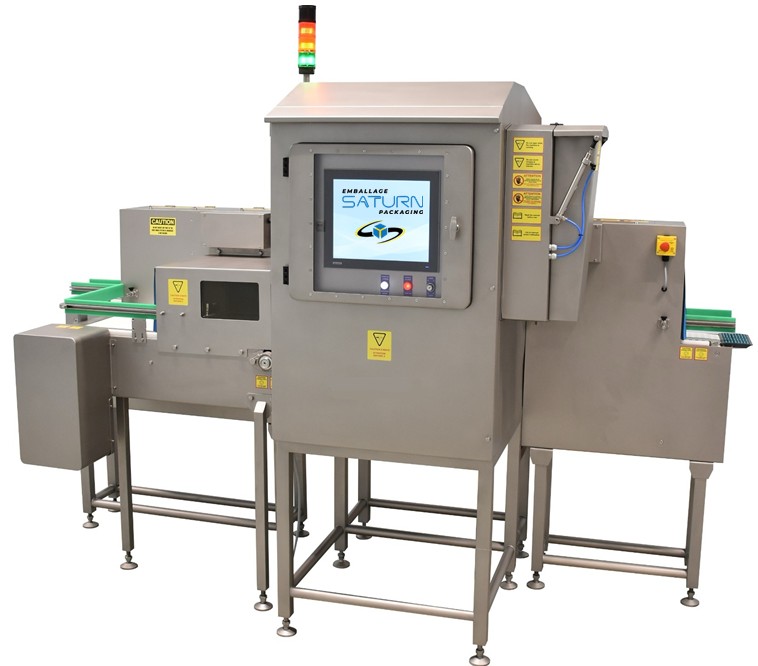
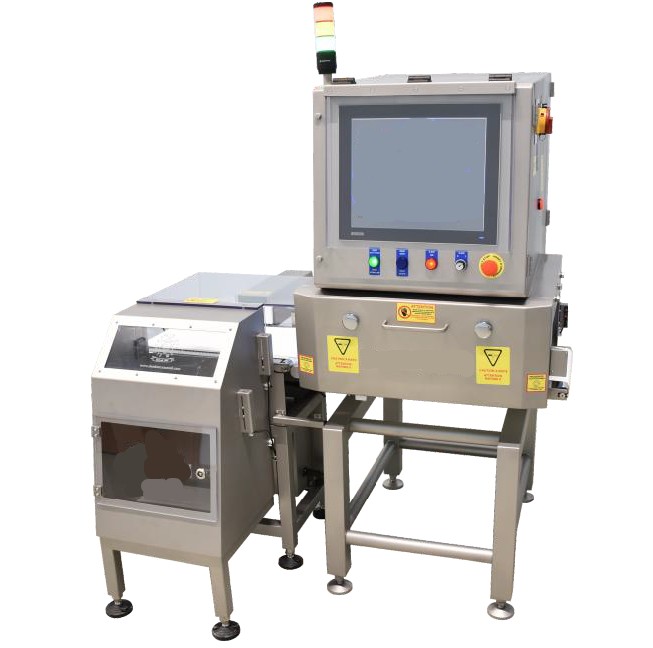
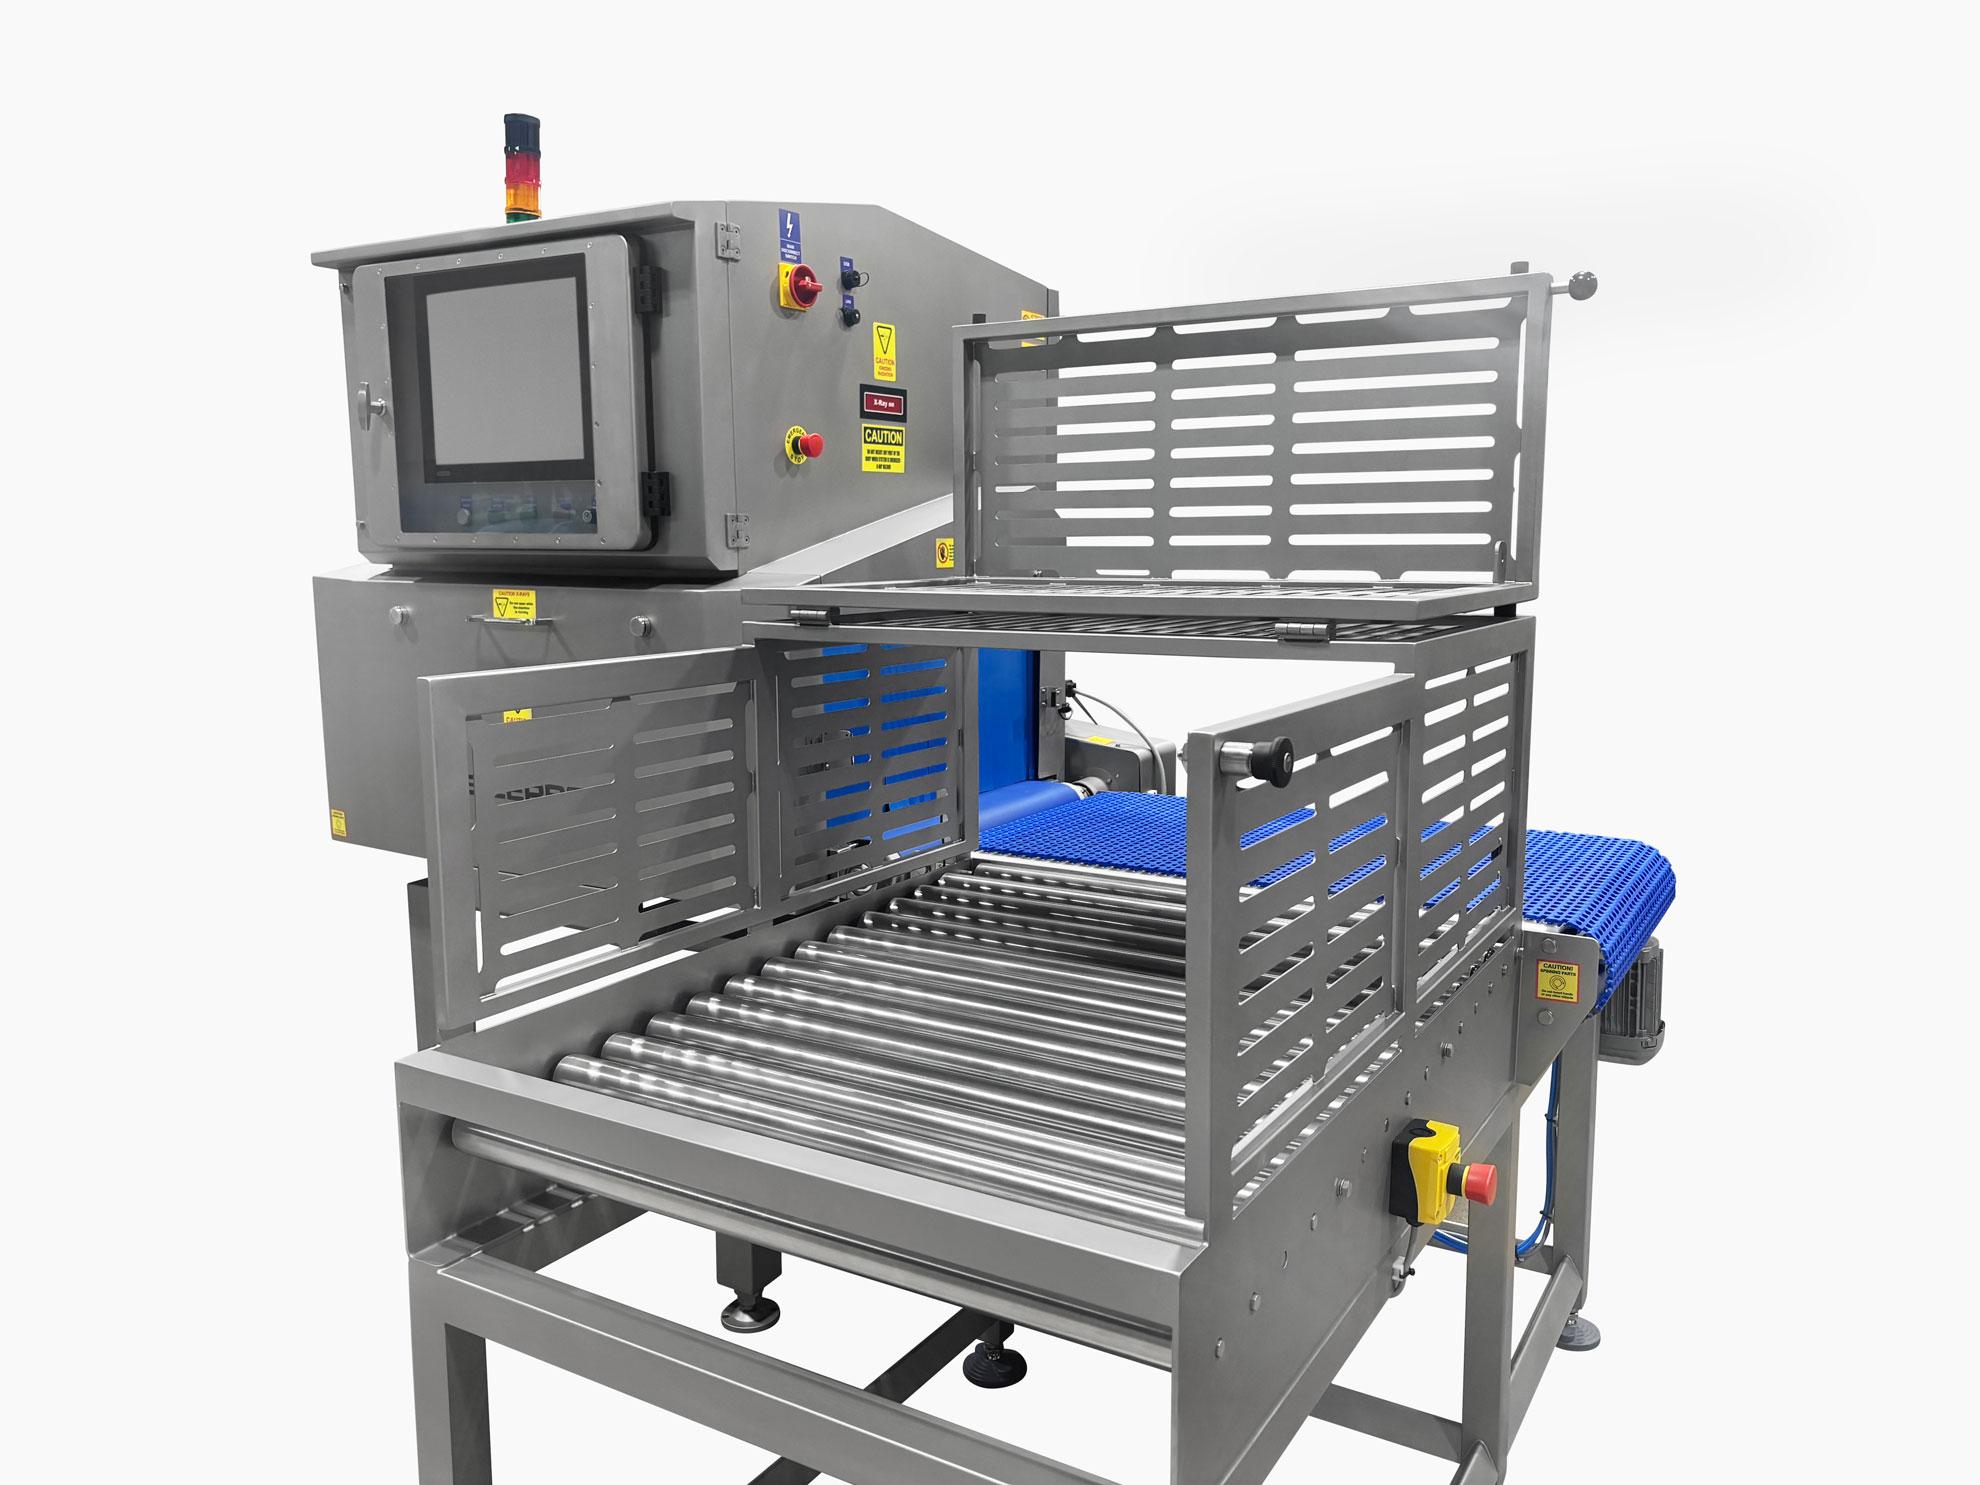
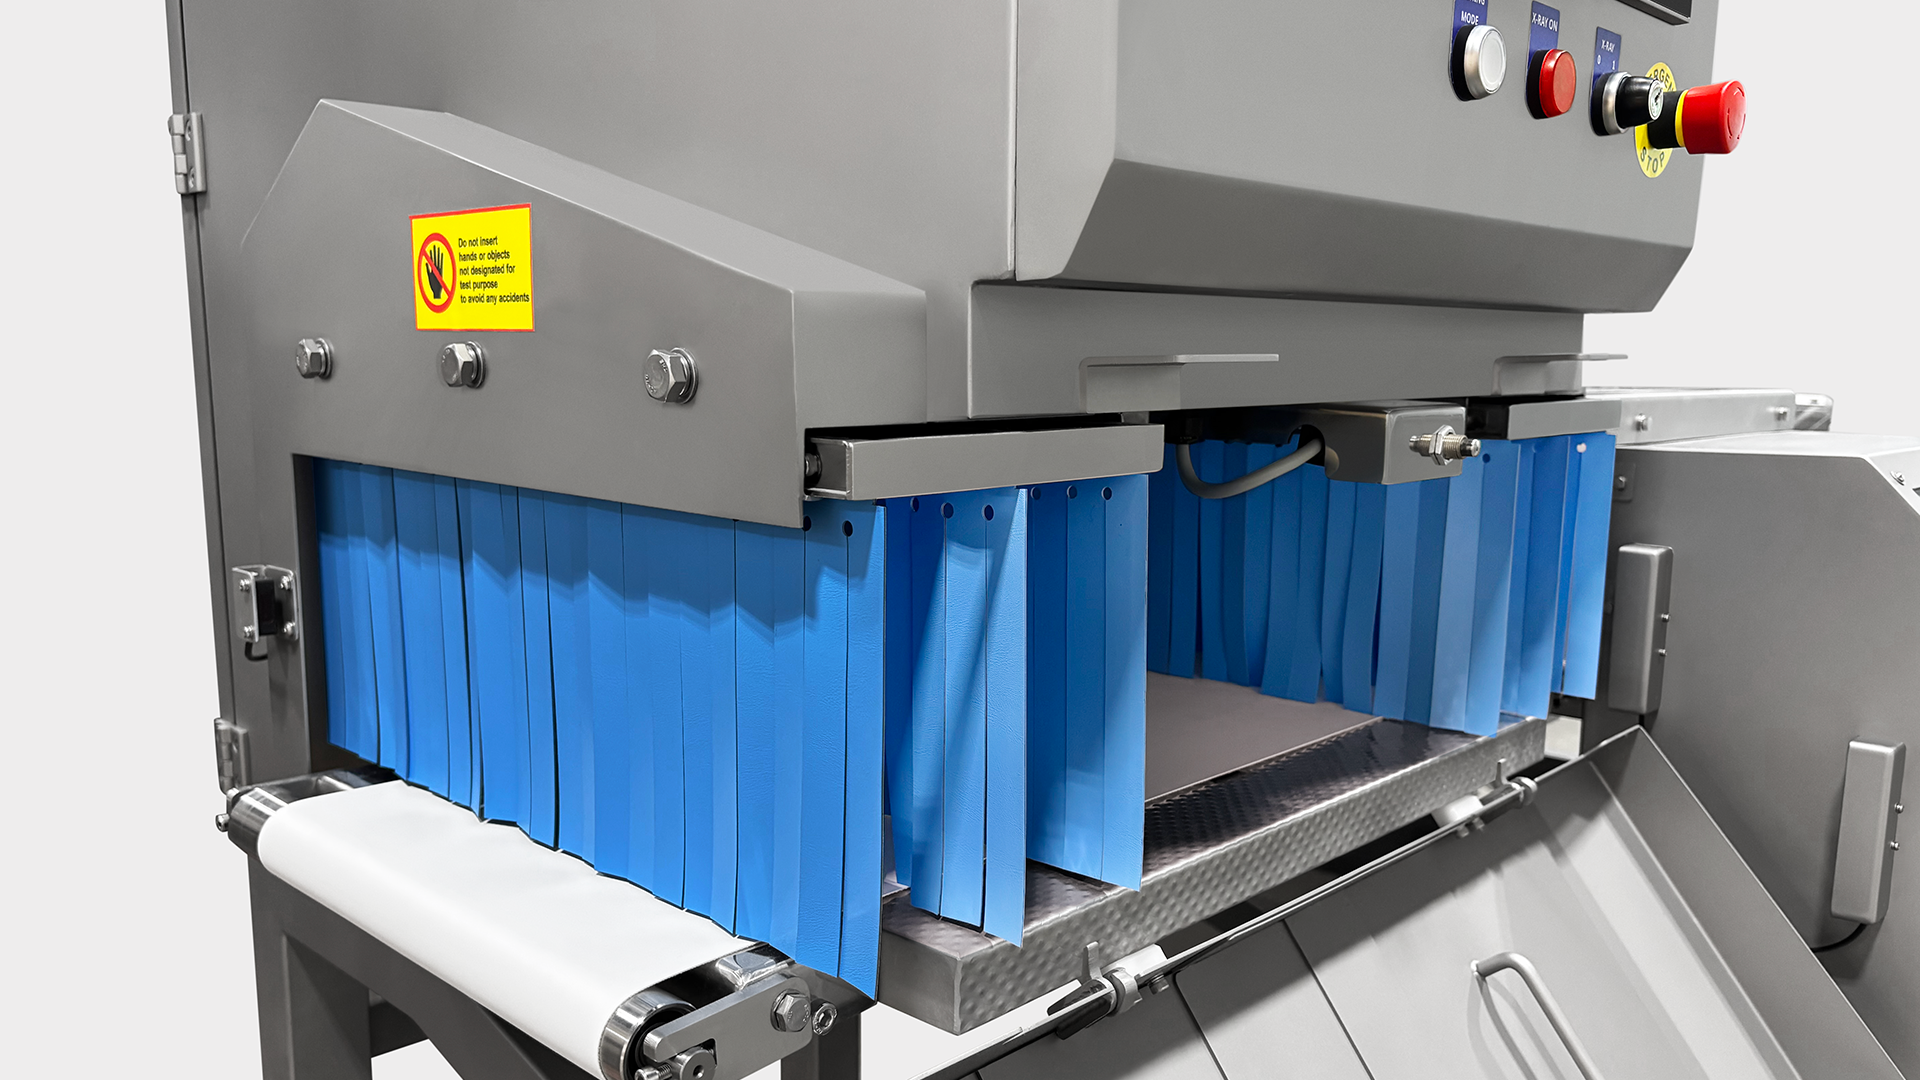
Our X-Ray Inspection Systems provide advanced inspection and foreign material detection for a wide range of food, beverage and packaged products. With a broad selection of models, conveyor widths and inspection configurations, systems can be engineered for everything from low-speed production lines to high-speed applications.
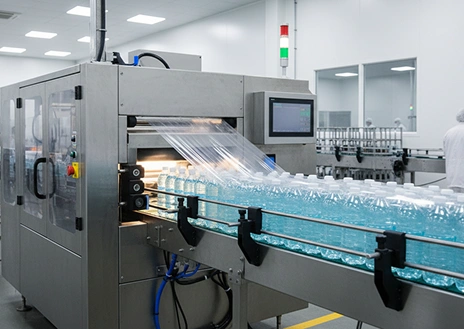
X-ray systems can inspect products in a variety of formats, including bottles, cans, jars, cartons, boxes, pouches, bags, trays, bulk products and unpackaged foods. Depending on the application, the system can detect foreign materials such as metal, glass, stone, bone and other high-density contaminants.
Different X-ray configurations are available to optimize inspection according to the product and container. These include top-beam, side-beam and chute-style X-ray systems. Side inspection configurations are particularly suited to containers such as bottles, cans and jars, while chute systems can be used for bulk and free-falling products.
Specialized models are also available for challenging food applications, including systems designed specifically for bone detection in chicken and poultry products.
Each system can be equipped with a product-specific automatic reject system, selected according to the product type, speed, weight and production requirements. Reject options can be configured for individual packages, containers or continuous product flow.
For demanding food processing environments, X-ray systems are available with IP65 or IP69 protection, along with hygienic designs focused on accessibility and easy washdown and sanitation. A Frost Option is also available, incorporating control-panel temperature management for operation in cold, refrigerated or challenging production environments.
Whether inspecting individual packages at lower speeds or bottles, cans and packaged products on high-speed production lines, the X-ray system can be supplied as a standalone inspection unit or fully integrated with conveyors, reject systems, controls and other packaging equipment.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad