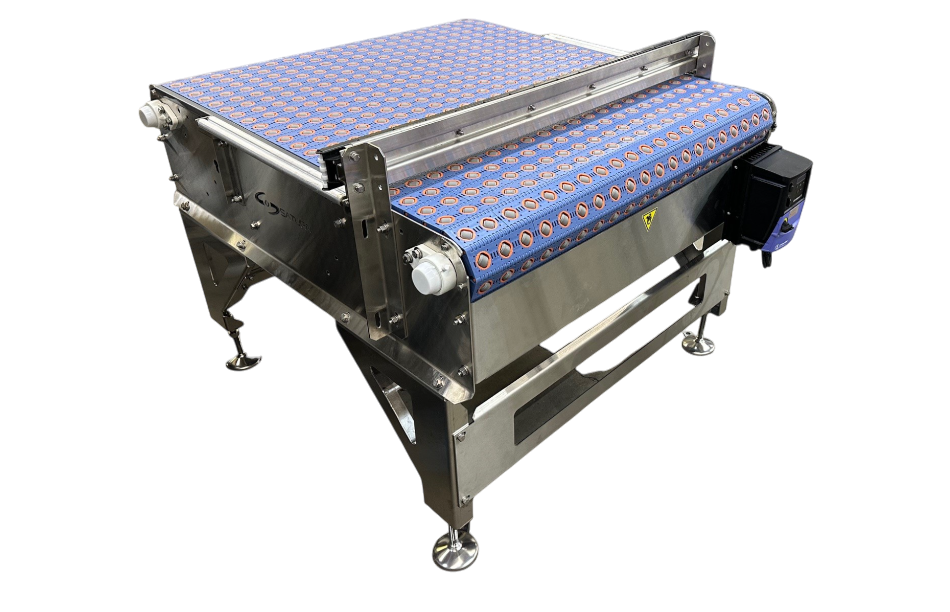
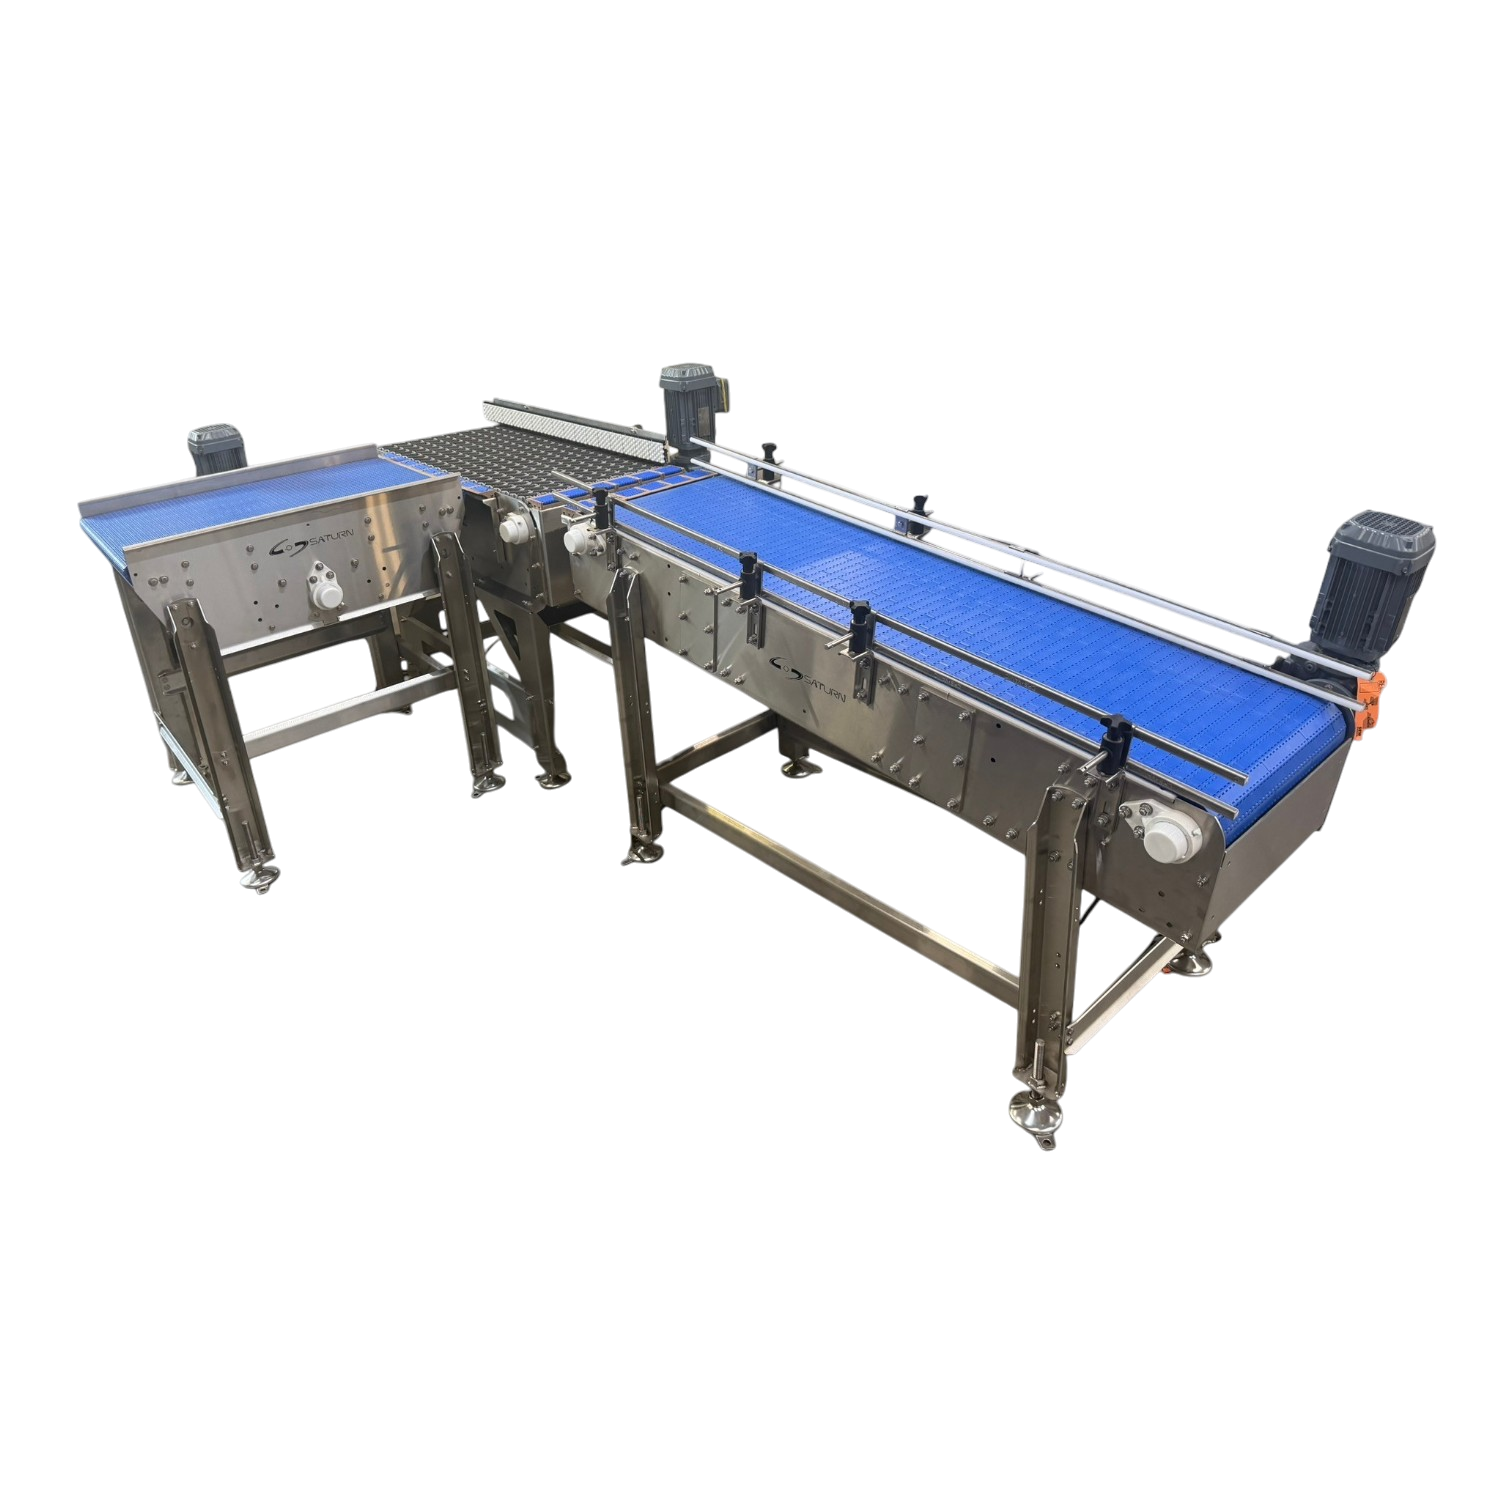
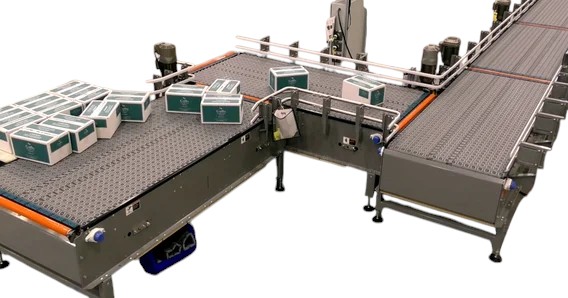
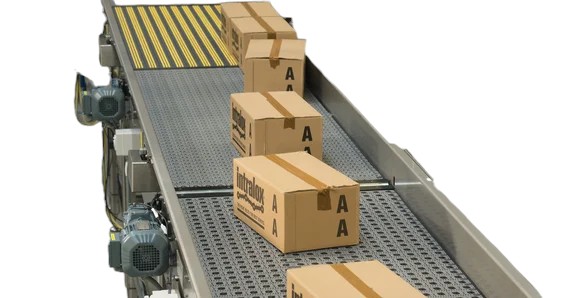
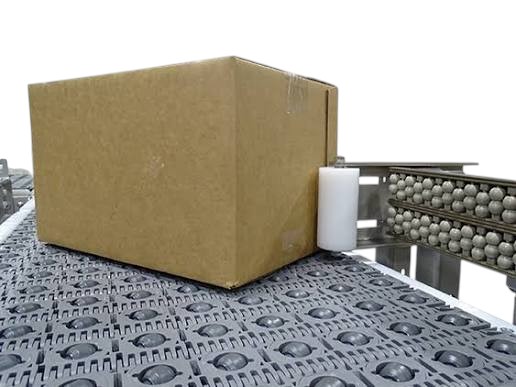
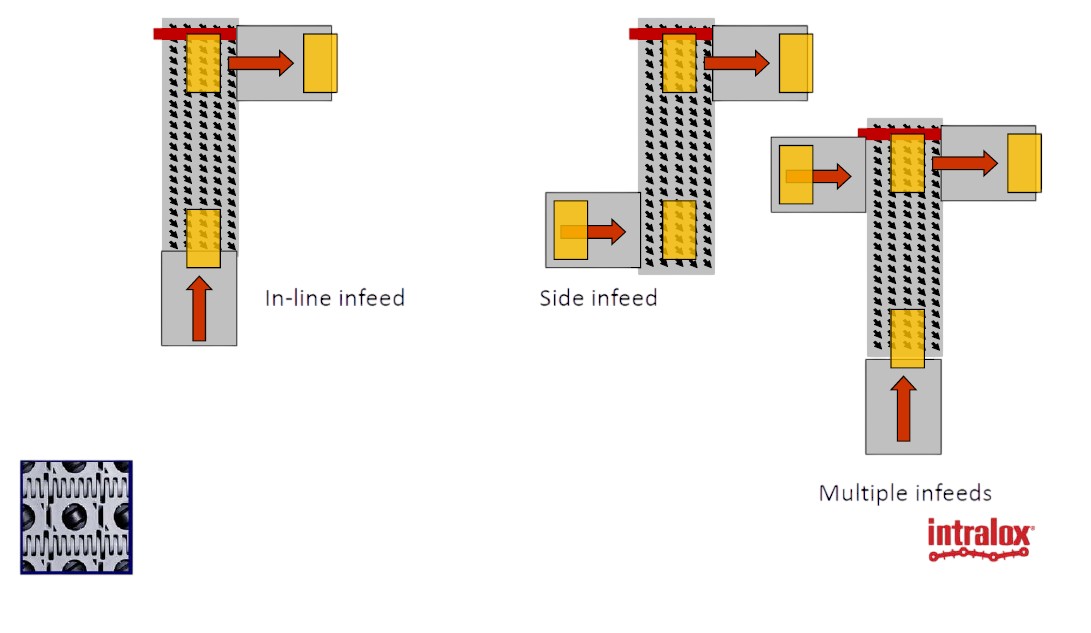
Saturn ARB Systems – Activated Roller Belt Conveyors provide advanced product handling using modular belts with integrated angled rollers that allow products to move laterally while continuing to travel forward.
This technology makes it possible to perform multiple product-handling functions including alignment, merging, diverting, switching, sorting, turning and 90° transfers within compact conveyor layouts. These are established applications of ARB technology.
Systems can incorporate passive or active ARB technologies depending on the required product movement and application. Passive configurations use the movement of the conveyor and roller interaction to redirect products with relatively simple mechanics, while active configurations provide additional control for more complex sorting, diverting and routing applications.
ARB systems are particularly useful when products need to be repositioned or redirected without conventional pushers, pop-up transfers or large mechanical diverting devices. This can provide smooth product movement while reducing the amount of equipment required around the conveyor.
Products entering in different positions can be automatically aligned or justified to create consistent presentation for downstream equipment. Multiple product streams can also be merged into a common conveyor, or a single stream can be divided and switched between multiple downstream lanes.
For perpendicular transfers, ARB systems can redirect products 90° from the original direction of travel while maintaining controlled product movement. Products can also be selectively turned or reoriented, which is useful when cases or trays must enter downstream packaging or palletizing equipment in a specific orientation.
For automated sorting applications, products can be identified using photoeyes, barcode readers, vision systems, checkweighers or other inspection equipment. The control system can then automatically route each product to the appropriate conveyor, lane or reject destination.
ARB Systems can handle a broad range of packaged products including cases, cartons, trays, totes, bags, pouches, shrink-wrapped bundles and other packages. ARB technology is particularly valuable where different product sizes and formats must be handled on the same line.
Saturn ARB Systems can be supplied as standalone conveyor modules or integrated with accumulation systems, inspection equipment, case packers, labeling systems, palletizers and complete automated conveyor lines.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad