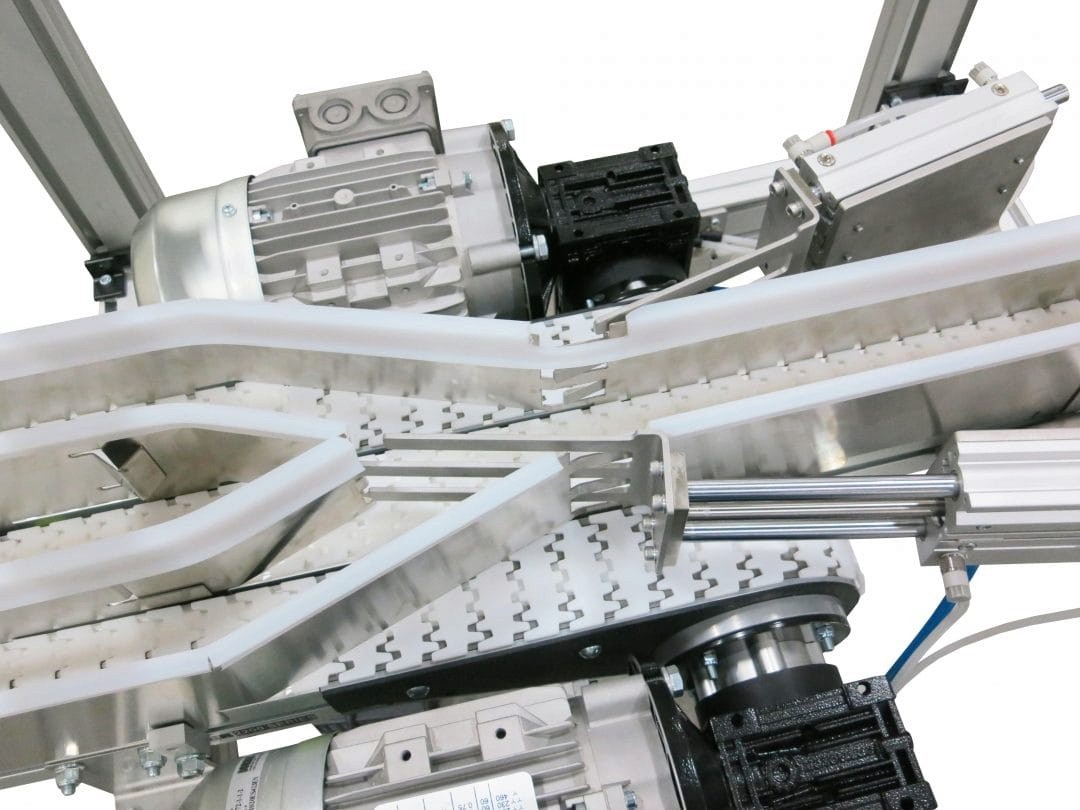
Saturn Diverting Systems are custom-engineered conveyor solutions designed to automatically redirect products from one production stream to one or multiple downstream lanes, machines or destinations. Diverting can be used for line distribution, sorting, production balancing, product routing and process selection.
A wide range of diverting technologies can be selected according to the product dimensions, weight, stability, production speed, number of destinations and required transfer direction.
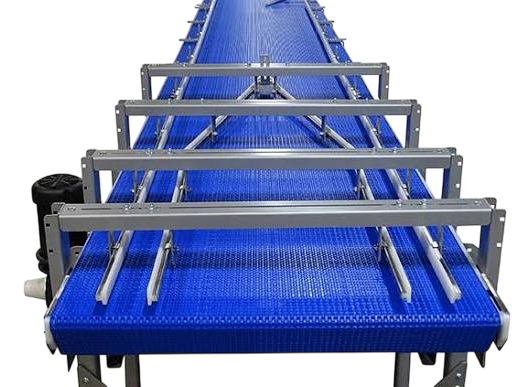
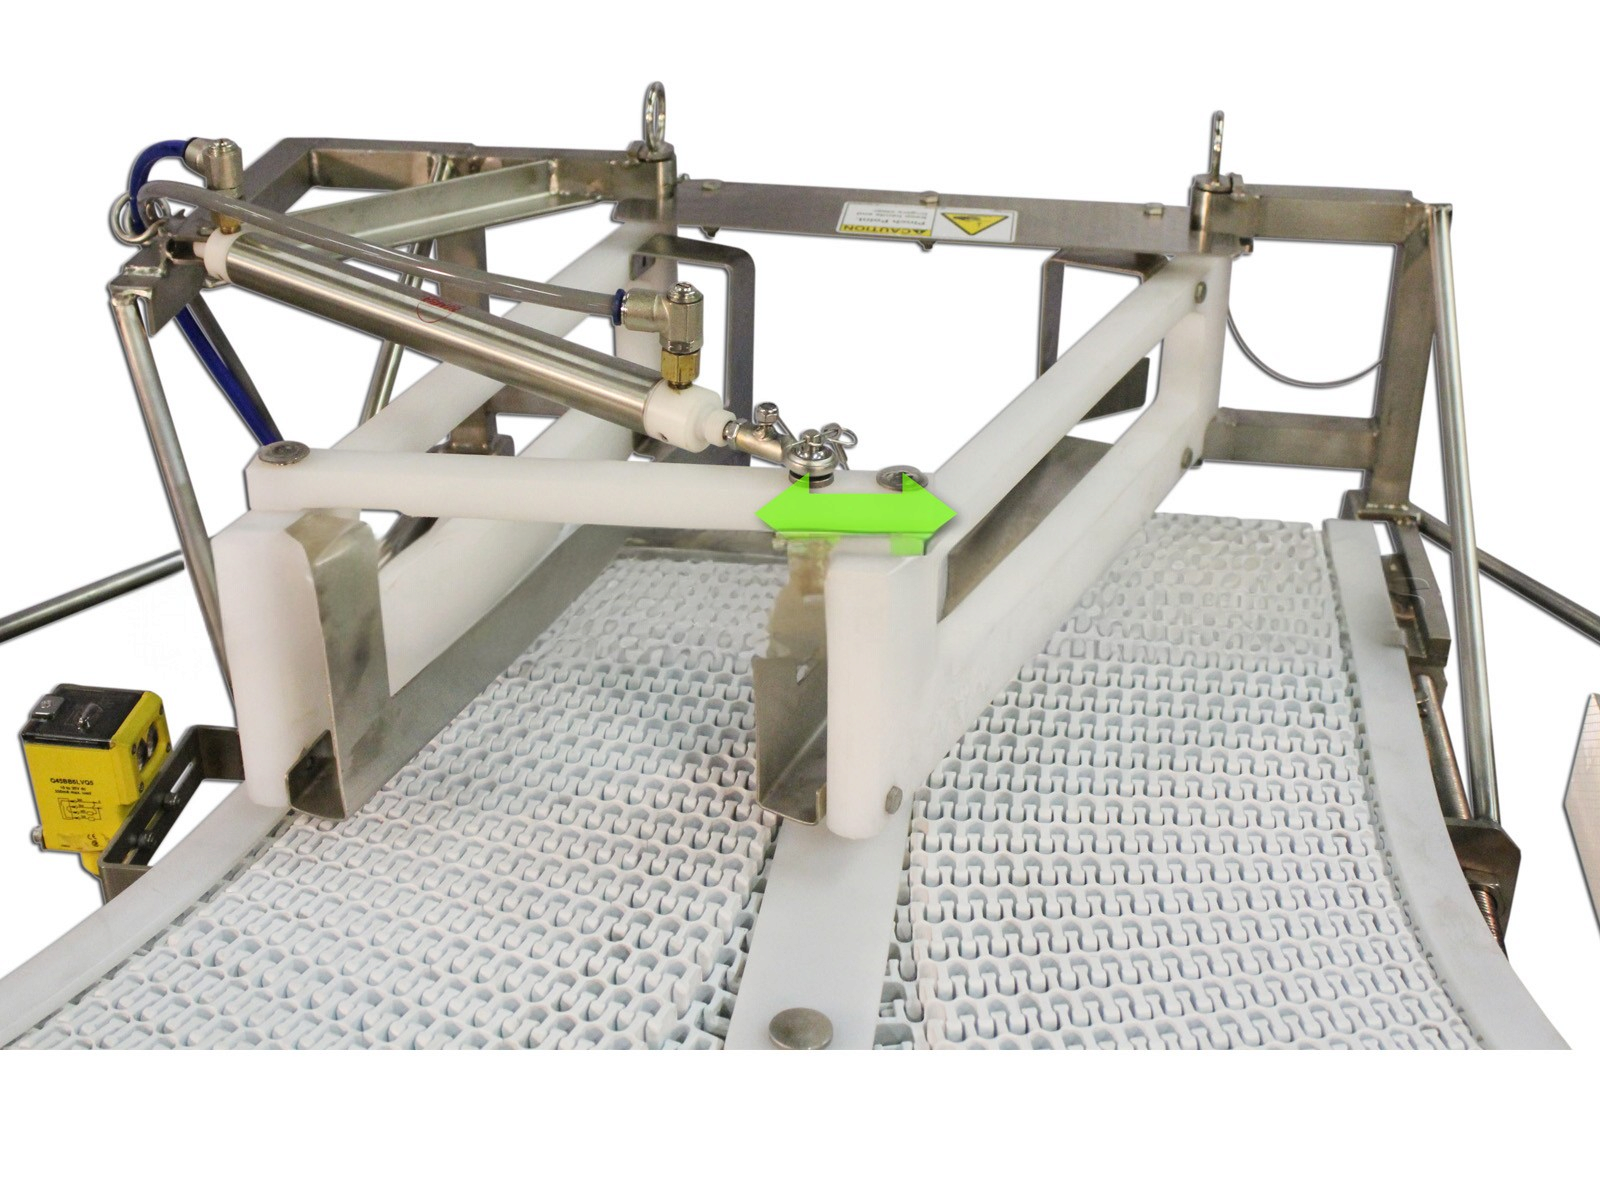
Diverter arms, gates and paddles provide a simple and reliable method of directing products between conveyor lanes. The diverting mechanism can be pneumatically or electrically actuated and synchronized with product detection sensors.
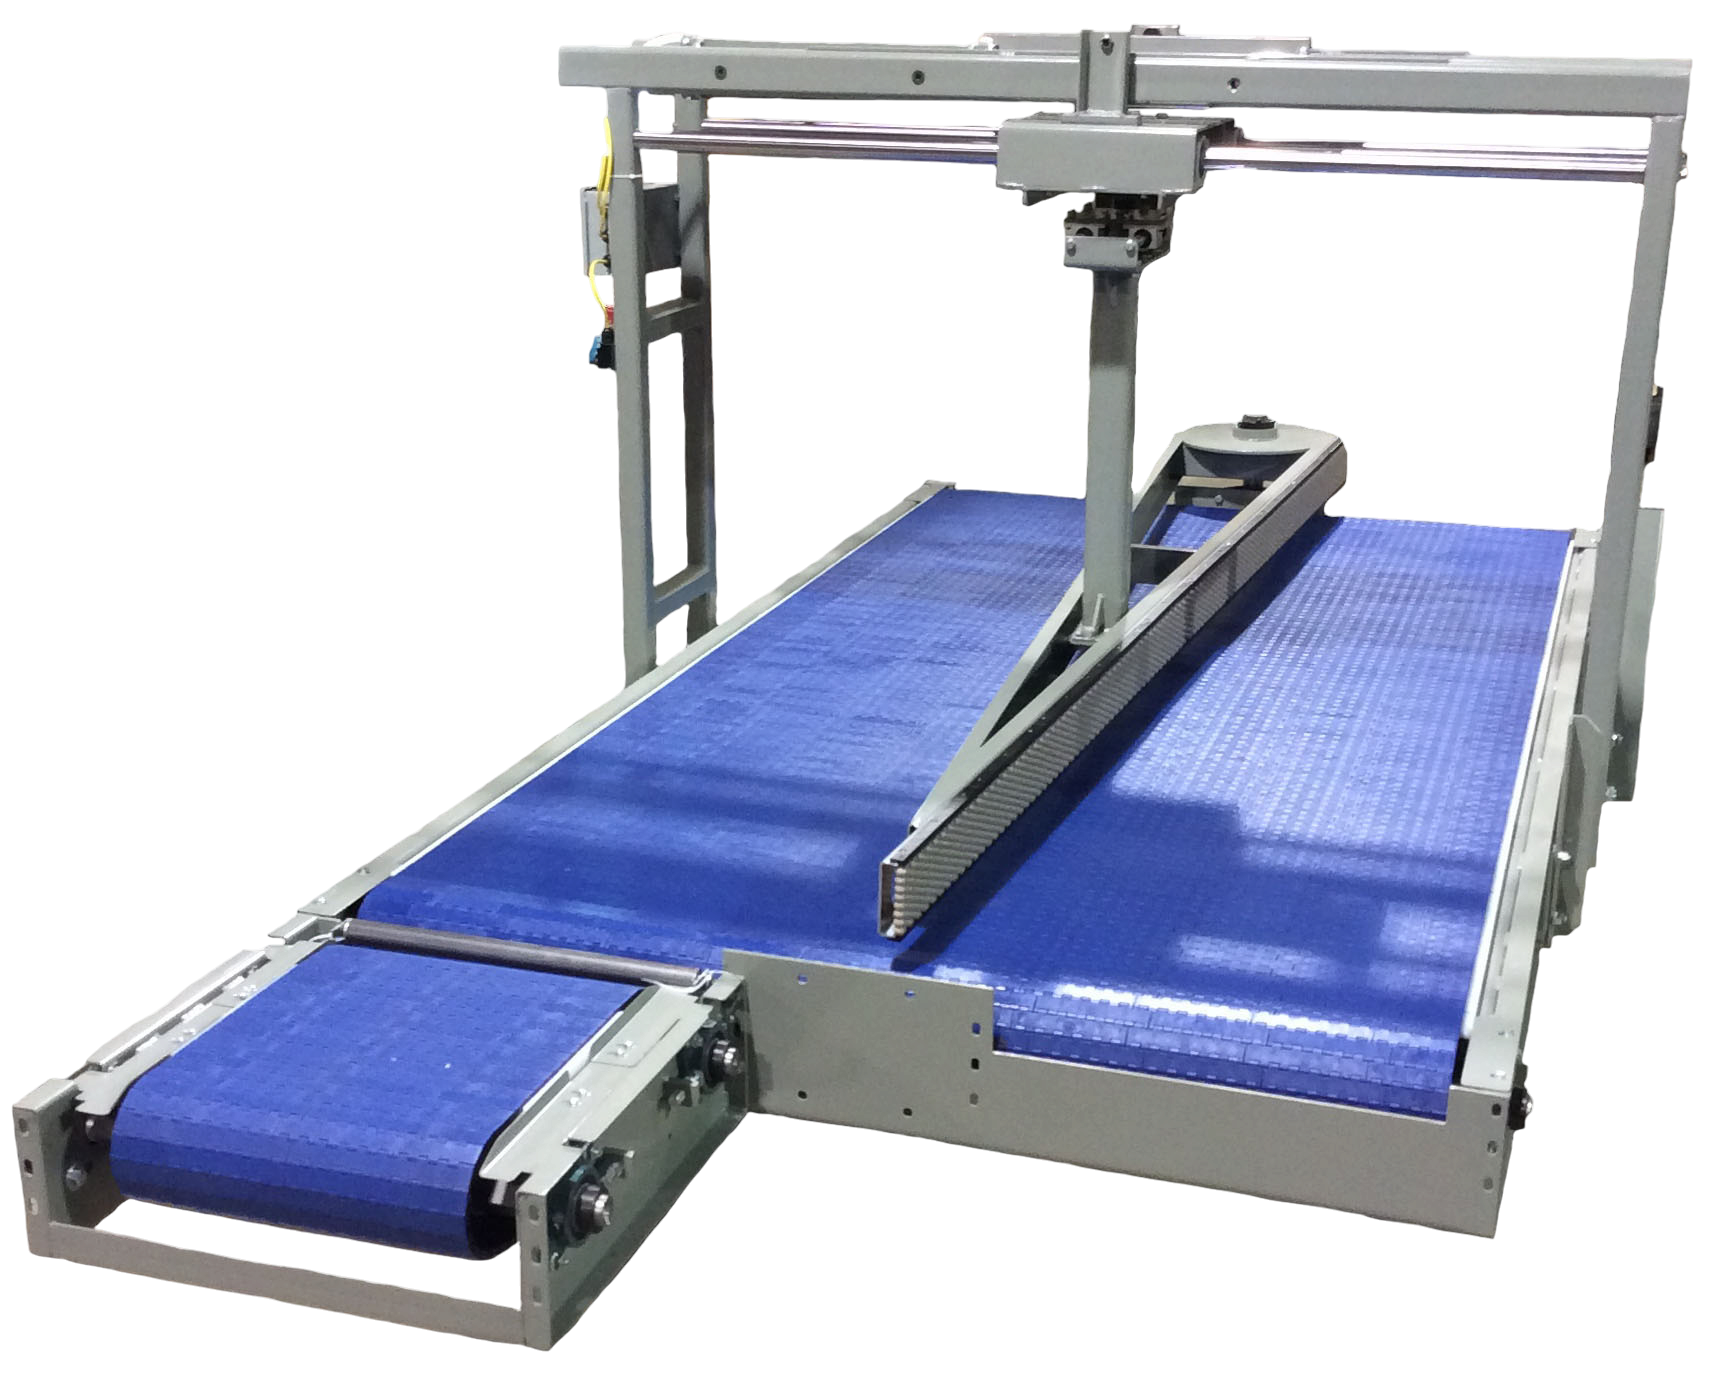
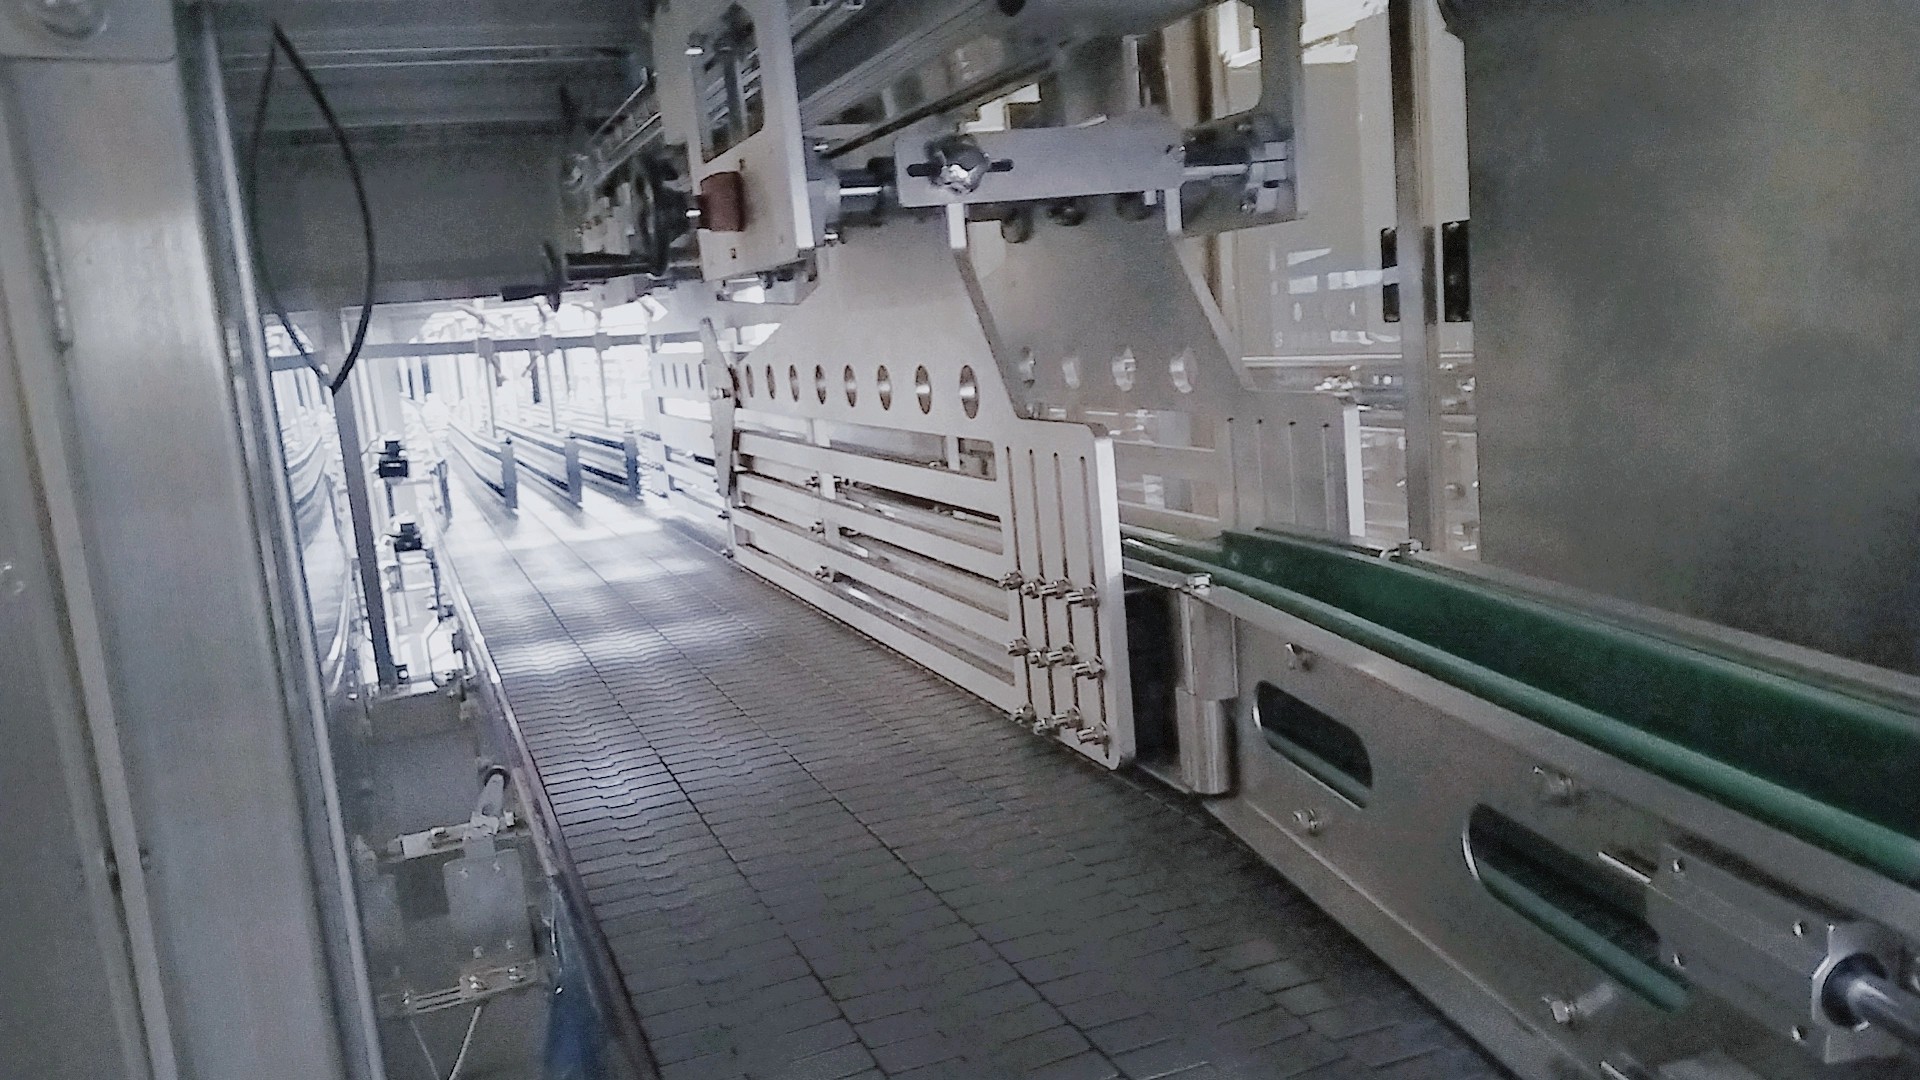
Pusher divert systems move products laterally or perpendicular to the main conveyor flow. Pushers can be mounted from the side or overhead and are particularly useful for transferring cases, cartons, trays, totes and other stable packages onto another conveyor or processing station.
Lane-diverting systems can distribute a single product stream across two or more lanes. Adjustable or automatically controlled guides can be used to direct products while maintaining continuous production flow. These systems can also help distribute production between multiple downstream machines.
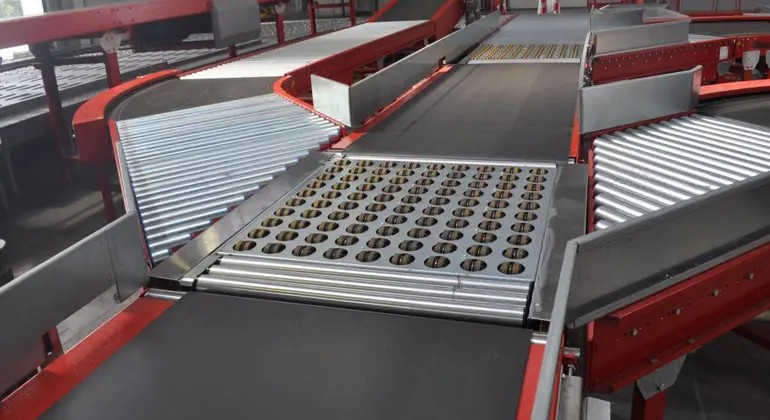
For more complex or high-speed applications, diverting can be accomplished using ARB technology, powered transfers, retracting conveyors or other custom product-handling mechanisms. The appropriate technology is selected according to the product and required movement.
Divert decisions can be controlled by photoelectric sensors, counters, barcode readers, vision systems, checkweighers, inspection systems or PLC logic. This allows individual products to be automatically routed according to SKU, destination, production requirements or inspection results. Sensors and counters are commonly used to trigger conveyor diverters, while inspection equipment can provide the signal for automatic product removal or routing.
Systems can be configured for 1-to-2, 1-to-3 or multiple-lane distribution, depending on the application. Products can be diverted to parallel lanes, perpendicular conveyors, accumulation systems, packaging machines or separate processing operations.
Diverting Systems can handle a wide variety of products including bottles, cans, jars, containers, pouches, trays, cartons, cases, totes and packaged products. Conveyor technology can include tabletop chain, modular belt, flat belt, mat-top or roller conveyors depending on the product.
Saturn Diverting Systems can be supplied as individual conveyor modules or incorporated into complete line integrations with merging systems, accumulation, single filing, product alignment, inspection, packaging and end-of-line equipment.