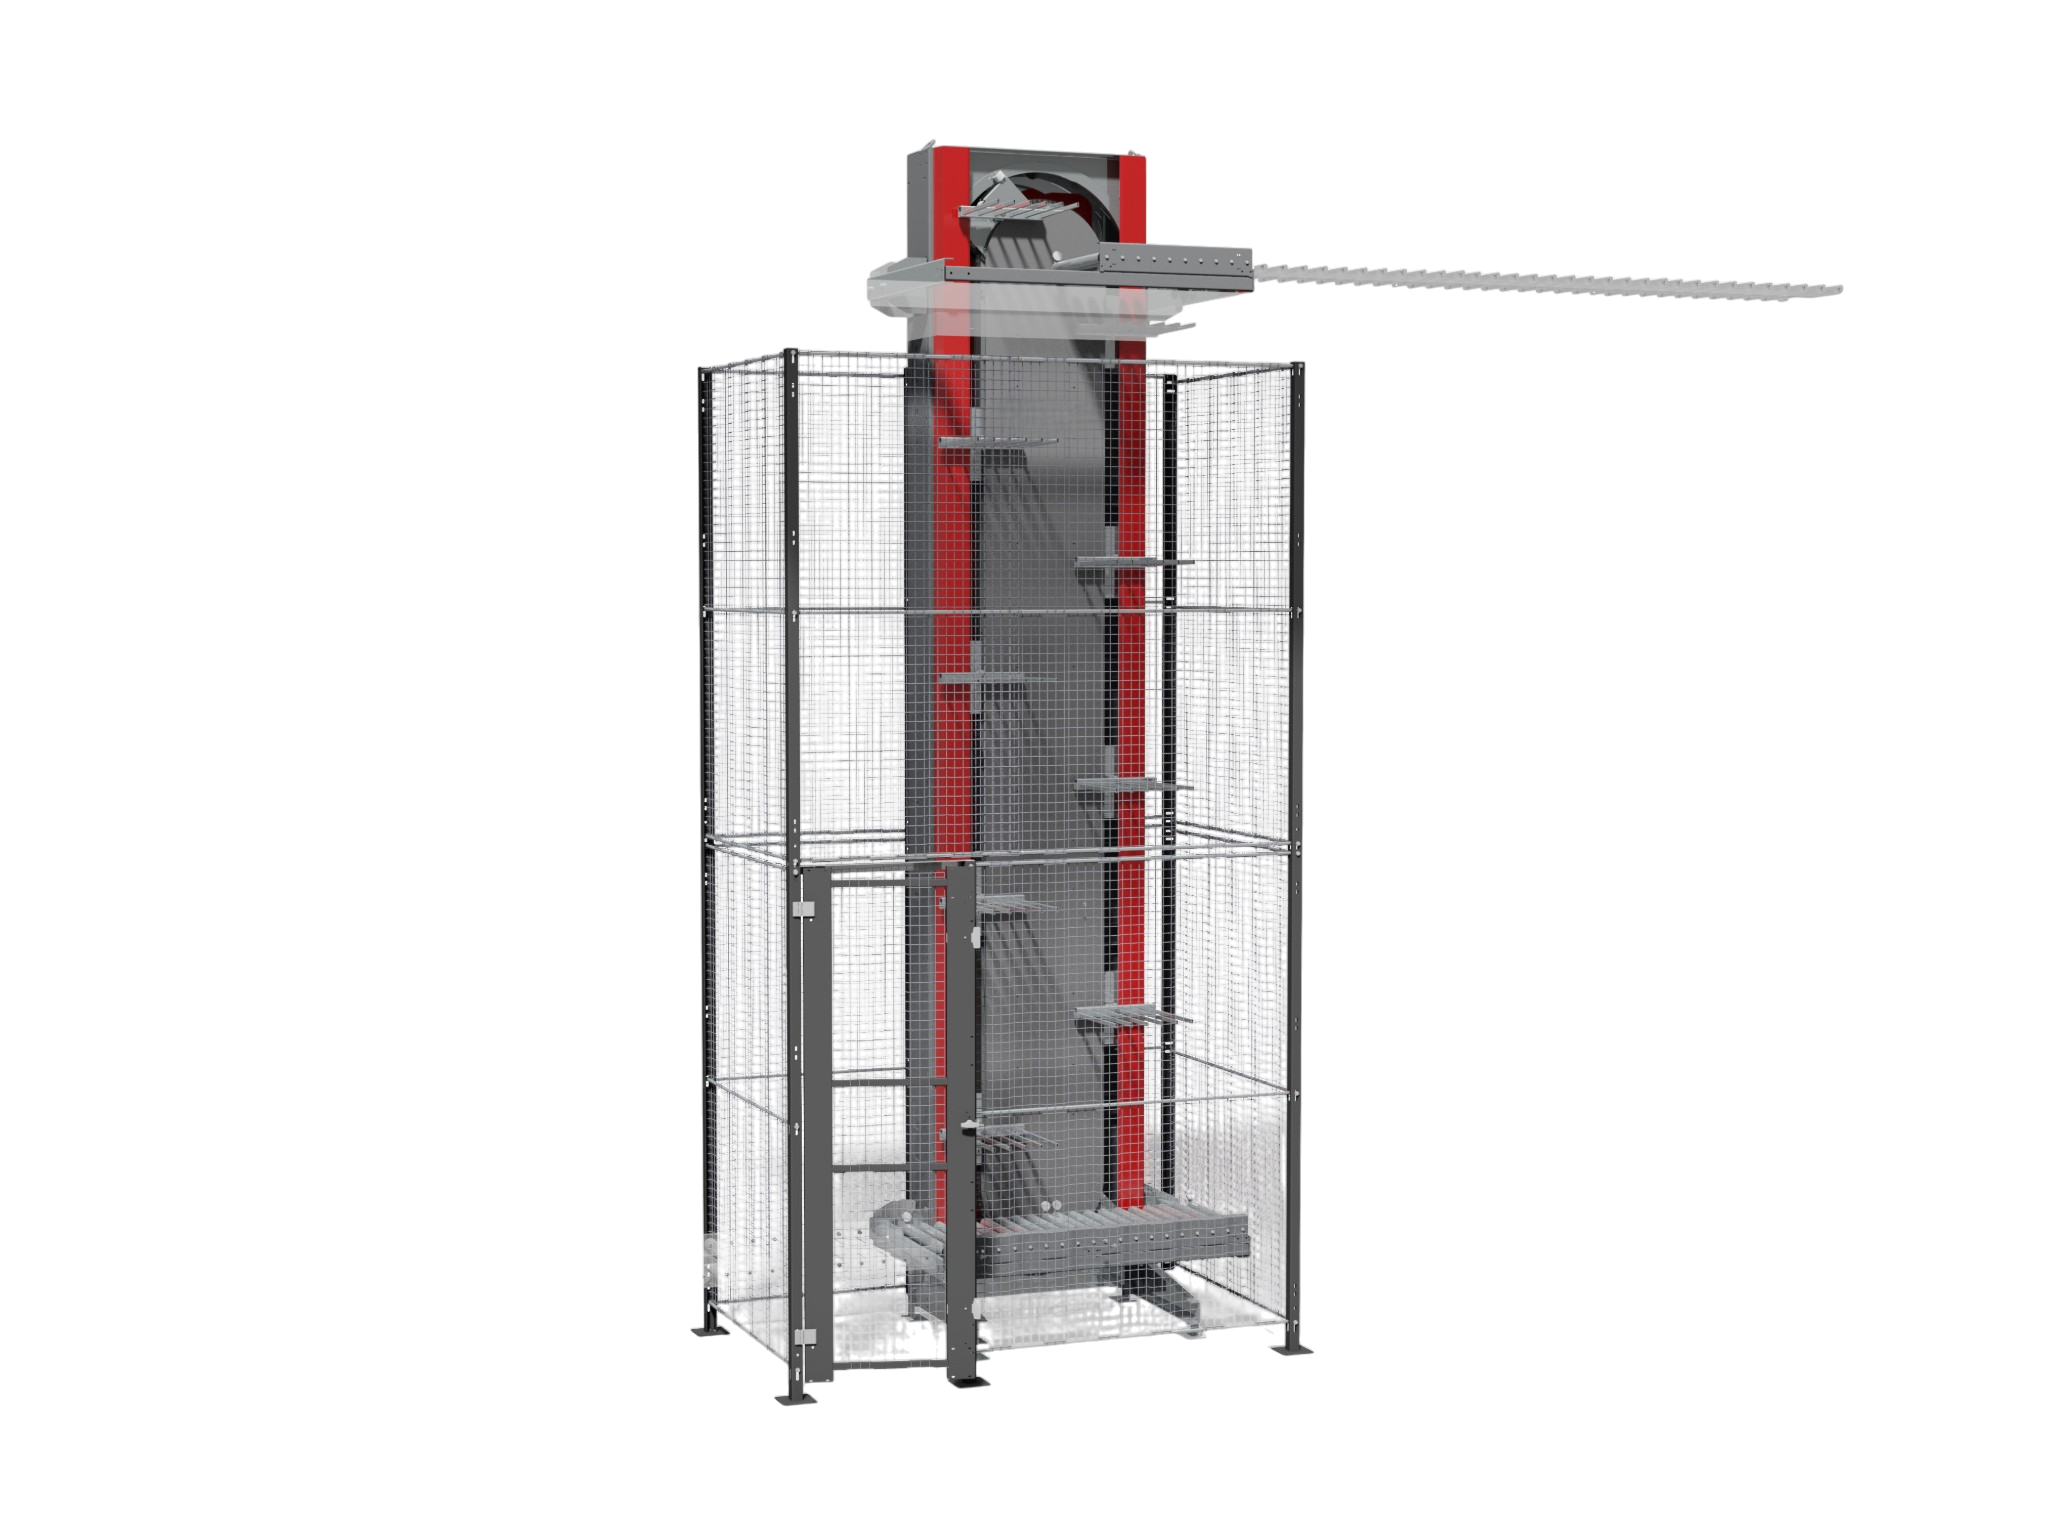
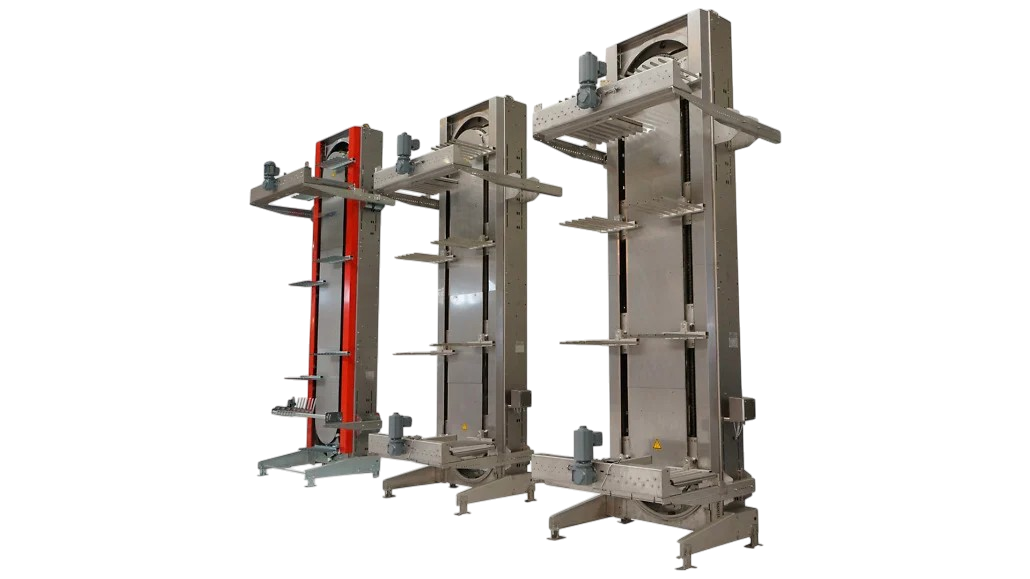
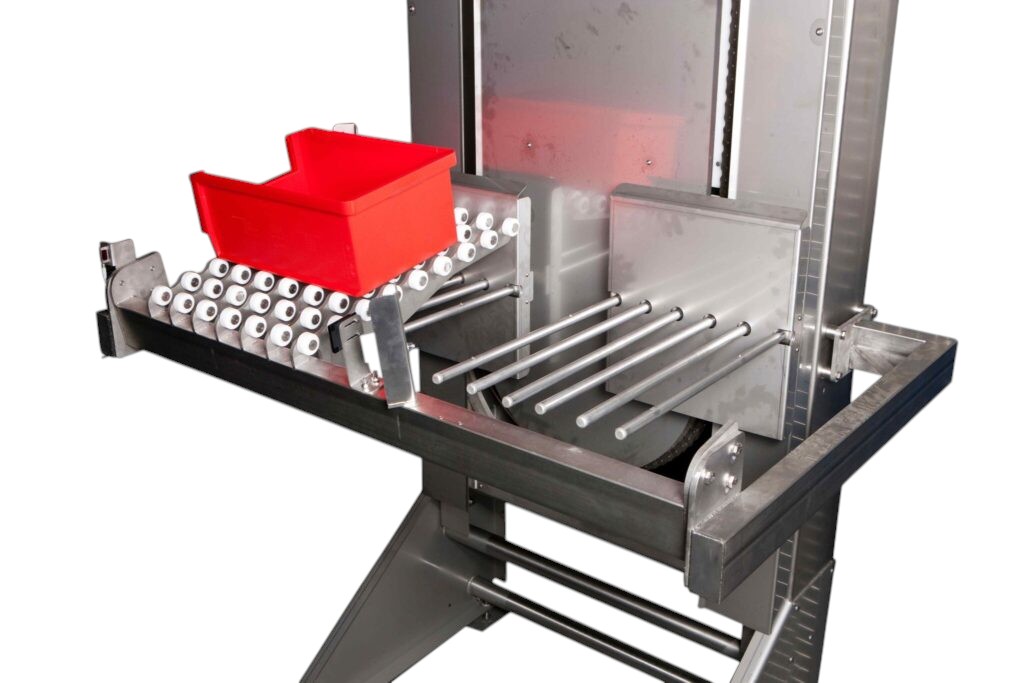
Saturn Elevators & Lowerators provide an efficient solution for transporting products vertically between different conveyor elevations, production levels or floors while minimizing the amount of valuable floor space required.
Systems can be configured as either an elevator to raise products or a lowerator to bring products to a lower elevation. Depending on the application and required throughput, Saturn can provide continuous vertical conveyors or reciprocating vertical conveyors.
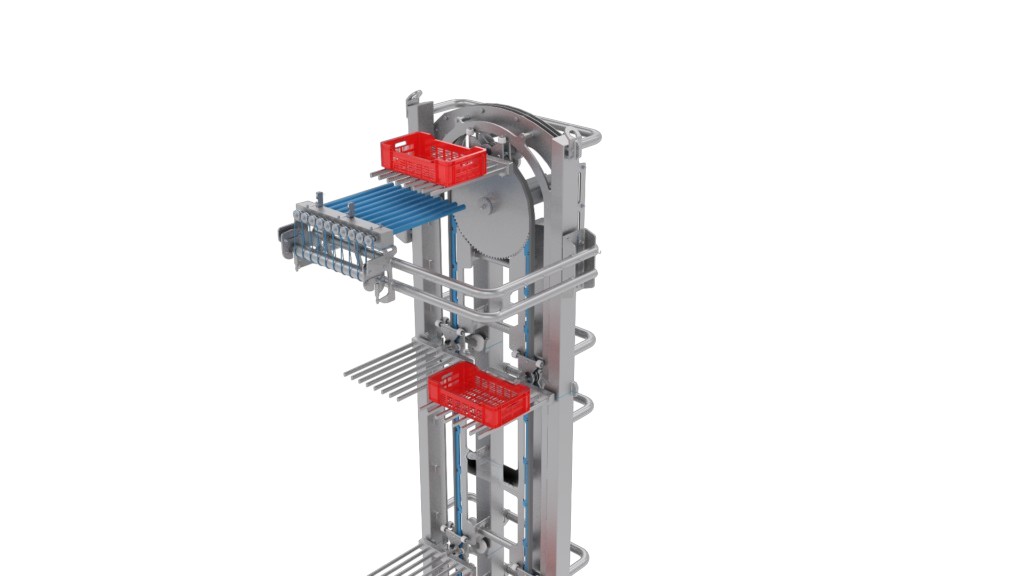
Continuous elevators and lowerators use multiple product carriers circulating continuously through the vertical conveyor. Products are transferred onto individual carriers, transported vertically and discharged onto the downstream conveyor while the system remains in continuous motion. This design is particularly well suited for medium- and high-throughput production lines. Continuous vertical conveyor designs can reach thousands of products per hour depending on product size and system configuration.
During vertical transport, the product carrier remains horizontal, helping maintain stable product orientation throughout the elevation change. This makes the system suitable for products such as cases, cartons, trays, totes, bags, shrink-wrapped packages and other packaged goods.
Reciprocating elevators and lowerators use a single carrier that travels between the required elevations. They provide a compact and economical solution for applications with lower throughput requirements or where products need to be transferred between specific levels. The carrier can incorporate a powered roller conveyor, gravity roller conveyor, belt conveyor or other product-specific transfer system.
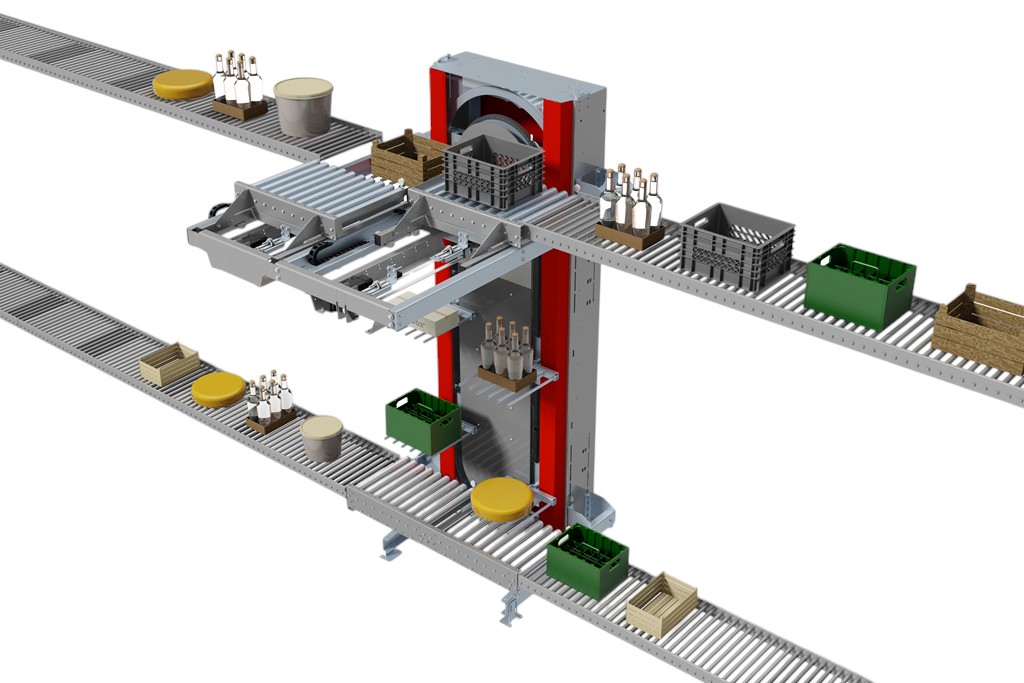
Systems can be configured in C-shape, Z-shape and other infeed/outfeed arrangements, allowing products to enter and discharge from different sides according to the plant layout. This flexibility makes vertical conveyors particularly useful for creating overhead conveyor routes, crossing production aisles and connecting conveyors located on different floors.
Multiple infeed and discharge elevations can also be incorporated for applications requiring products to be distributed between different production levels. More advanced configurations can function as a vertical sorting system, automatically directing products to the required floor or conveyor destination.
Elevators and lowerators are particularly useful when a production line needs to free floor space or maintain access underneath the conveyor system. Products can be elevated to an overhead conveyor, transported above production areas or walkways, and lowered again at the required downstream location.
Different conveyor technologies can be incorporated at the infeed, carrier and discharge, including powered roller, gravity roller and belt conveyors, allowing the vertical system to interface directly with the surrounding conveyor line.
Stainless steel and hygienic configurations can also be provided for food and washdown environments, including applications involving packaged and unpackaged food products.
Saturn Elevators & Lowerators can be supplied as standalone vertical conveyors or integrated with conveyor systems, accumulation, merging and diverting systems, packaging equipment, case handling and complete turnkey production lines.
Simple and easy to use machine with a user friendly interface to cover a vast range of packaged products: cosmetic, pharmaceutical, food, beverage, industrial product. Single or multipack products are manually loaded on the working table. The ergonomic sealing arm covers the heating element which creates the perfect seal. The motorized conveyor eases the product transfer into the heat chamber for the ultimate package.The integrated heat tunnel features a top, bottom and side heated air flow, twin blowers, teflon mesh belt that are all controlled with the SATU digital keypad