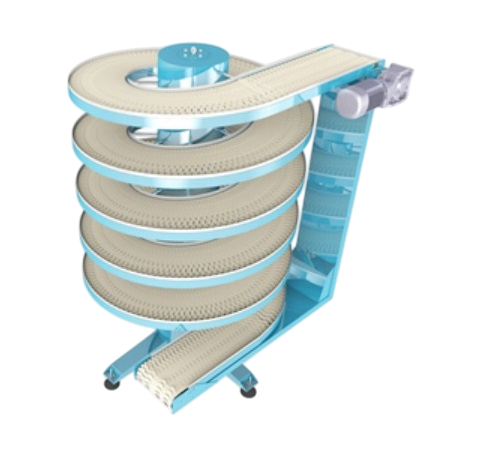
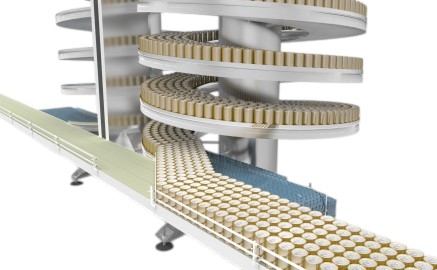
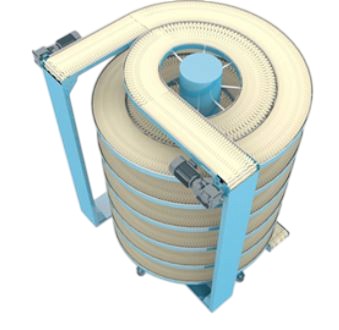
Saturn Spiral Conveyors provide a compact and efficient solution for continuously transporting products between different elevations while minimizing the amount of valuable production floor space required.
Unlike reciprocating elevators that transfer products one cycle at a time, spiral conveyors provide continuous product flow throughout the elevation change, making them particularly suitable for high-throughput production, packaging, bottling and material-handling lines.
Products travel along a continuous conveying surface arranged in a helical path around a central structure, allowing significant elevation changes to be achieved within a much smaller footprint than a conventional incline or decline conveyor.
Saturn Spiral Conveyors can be configured as either an elevator or lowerator, transporting products upward or downward while maintaining controlled product orientation throughout the transfer.
Systems can handle a wide variety of products, including bottles, cans, jars, containers, cases, cartons, trays, totes, shrink-wrapped bundles and other packaged products.
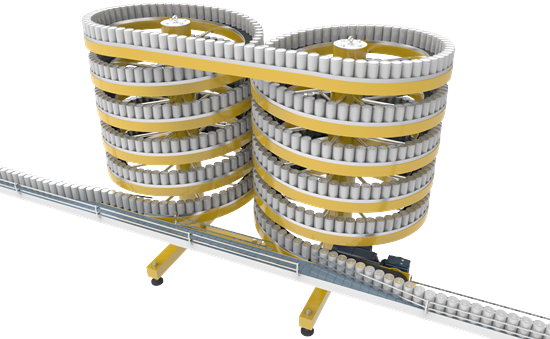
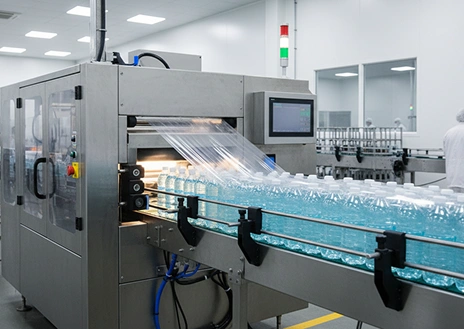
For bottling and container-handling applications, spiral conveyors can transport empty or filled bottles, cans and jars between different elevations. Systems can be configured for single-file or mass-flow conveying, depending on the container, required throughput and surrounding conveyor system.
Mass-flow spiral configurations allow multiple bottles, cans or jars to travel simultaneously across the conveyor width, providing high-capacity vertical transportation while maintaining a compact footprint. This makes spiral conveyors particularly useful for connecting different sections of high-speed bottling and packaging lines.
For cases, cartons, trays and totes, the spiral provides continuous vertical transportation without interrupting product flow. Conveyor width, conveying surface, speed and side guides are selected according to the product dimensions, weight, stability and required throughput.
Spiral conveyors are also an effective solution for creating overhead conveyor routes. Products can be elevated above production equipment, work areas or aisles, transported across the facility and lowered again at the required downstream location.
Systems can also connect different production floors or mezzanine levels, with multi-level configurations available when products need to enter or discharge at several elevations.
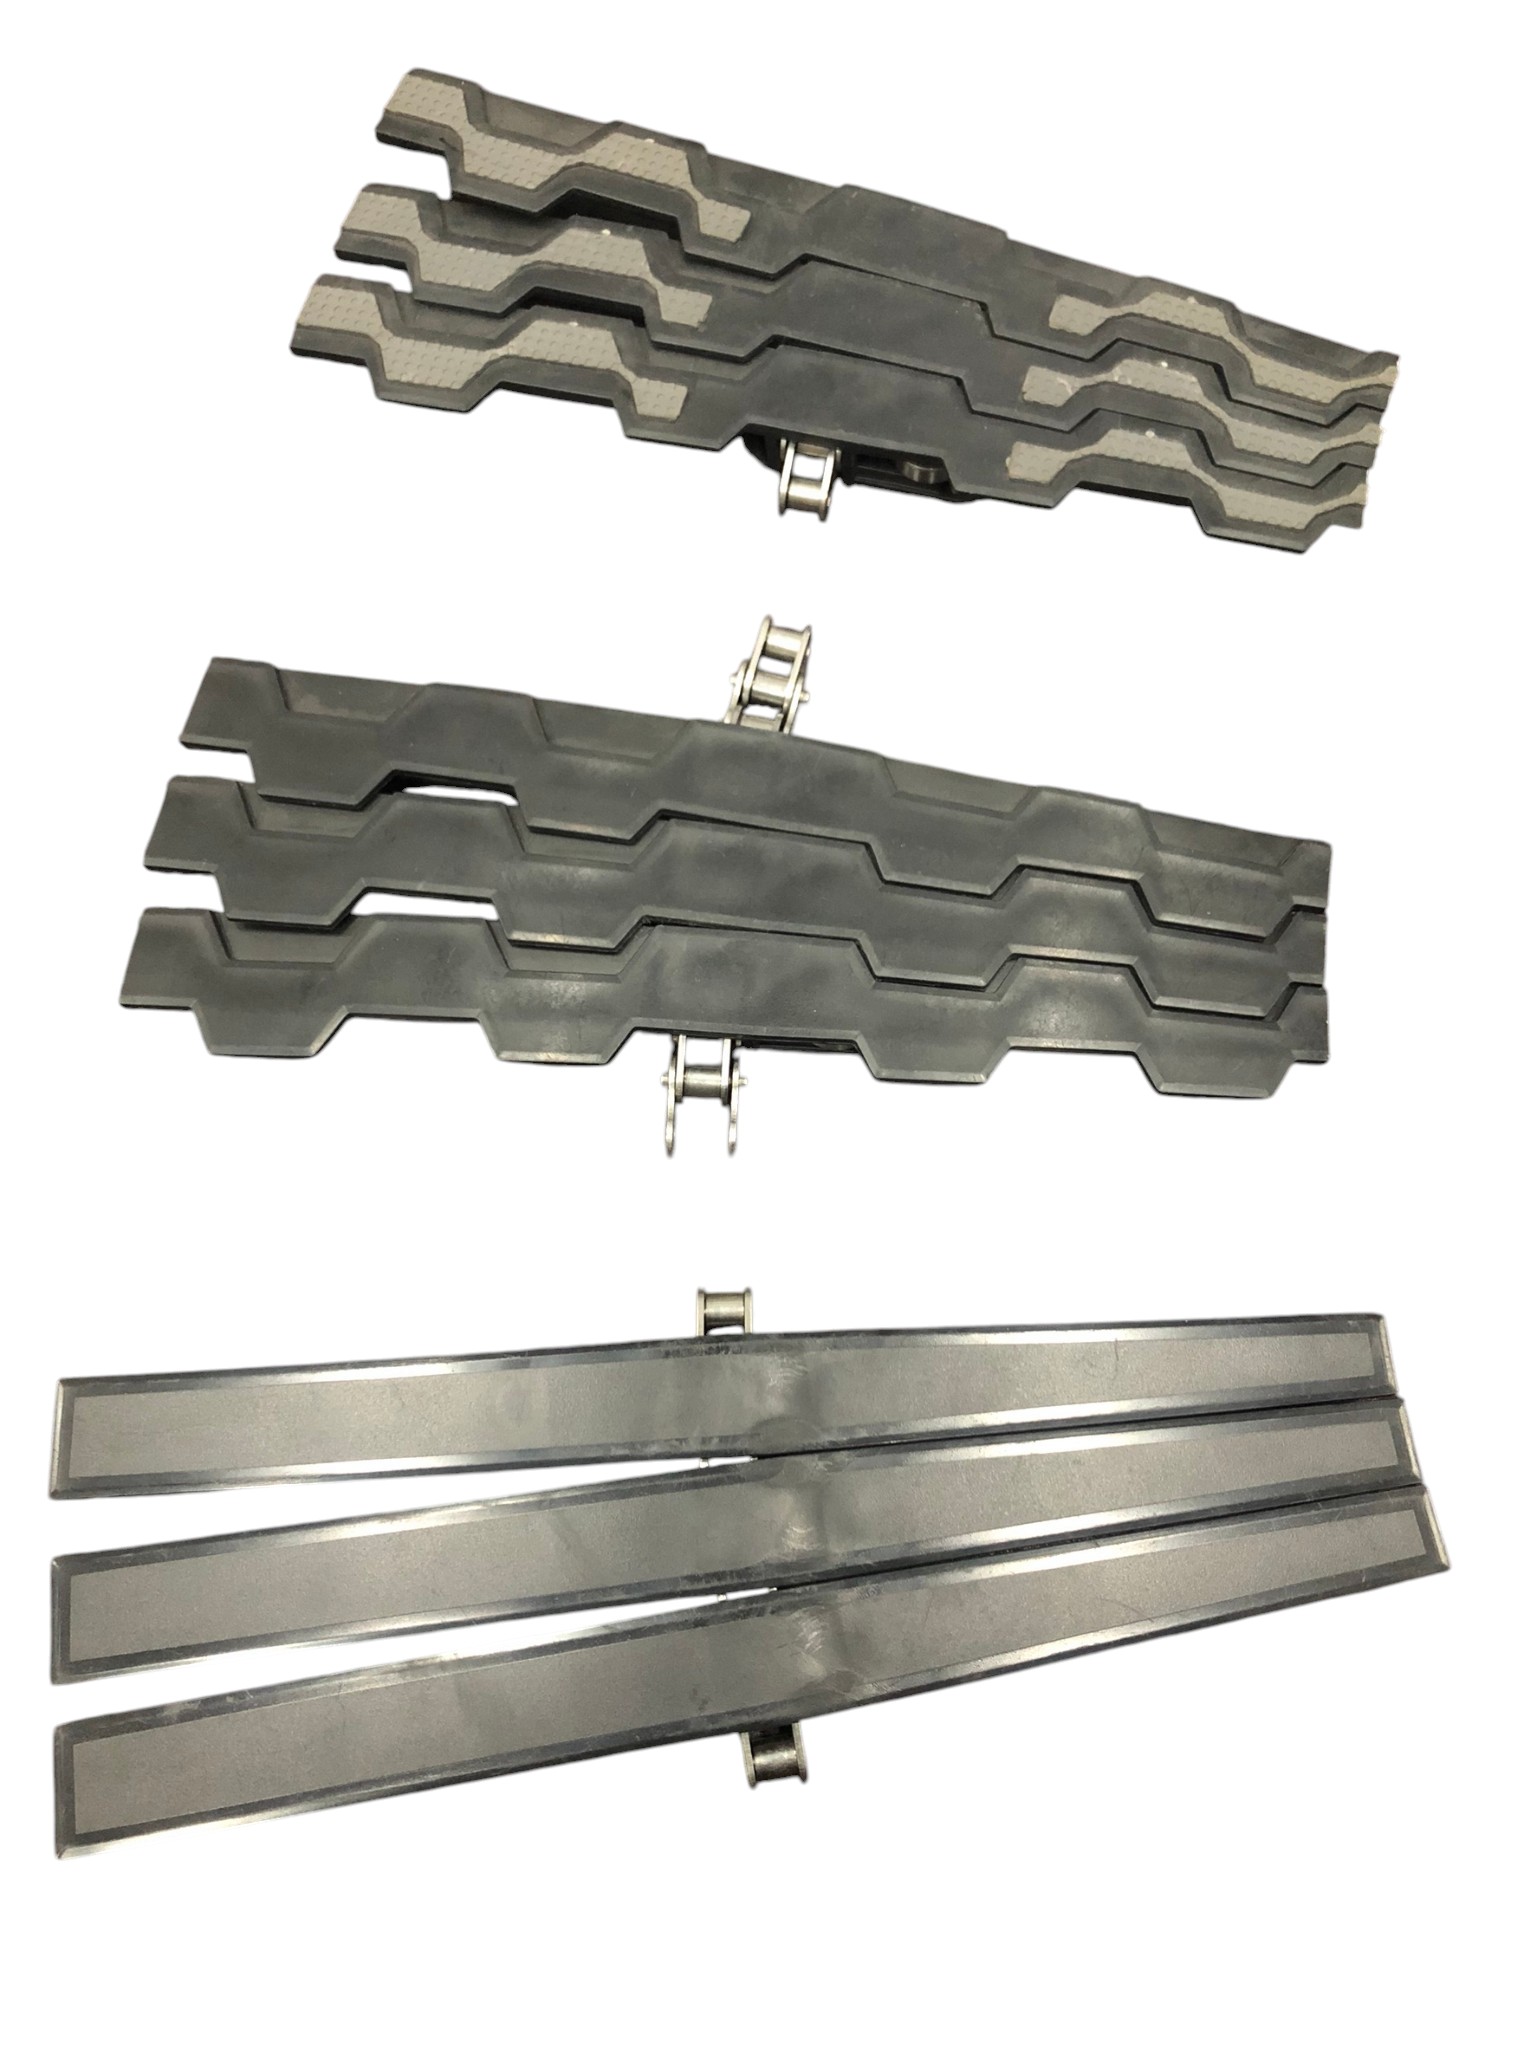
Depending on the application, different belt or slat configurations, widths and product-contact surfaces can be incorporated. High-grip surfaces and customized side guides can be used when additional product stability is required.
Construction can be supplied in painted steel, stainless steel or hybrid configurations, with stainless steel and washdown designs available for food, beverage and wet production environments.
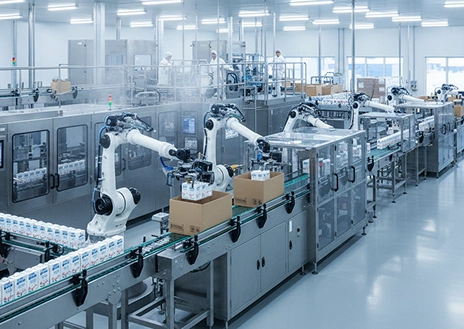
Saturn Spiral Conveyors can be supplied as standalone vertical conveying systems or fully integrated with mass-flow conveyors, single filing systems, accumulation conveyors, fillers, labelers, inspection equipment, case packers, palletizers and complete automated production or packaging lines.